commercial tire recycling
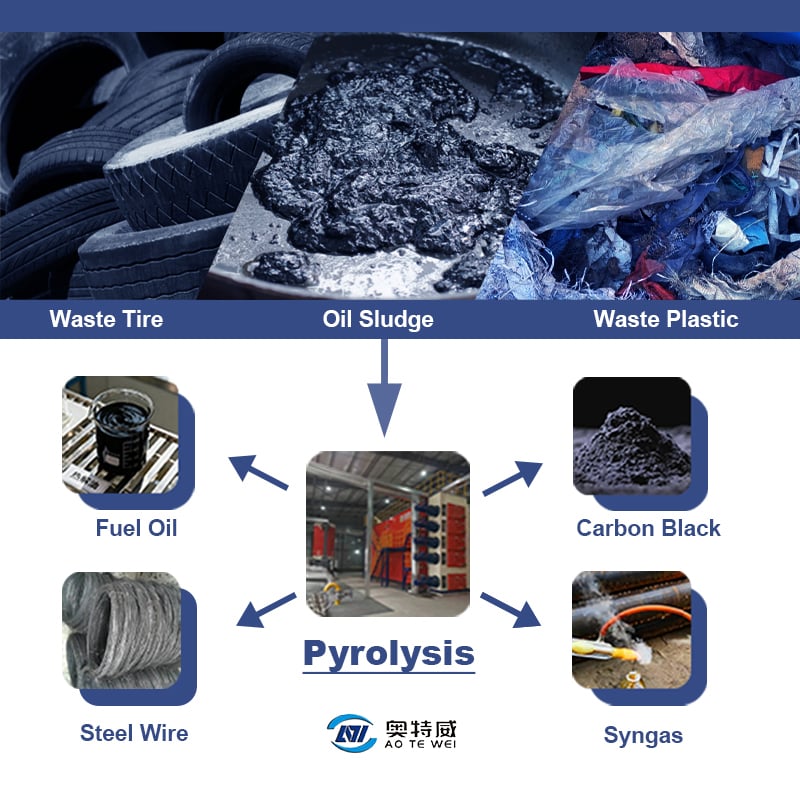
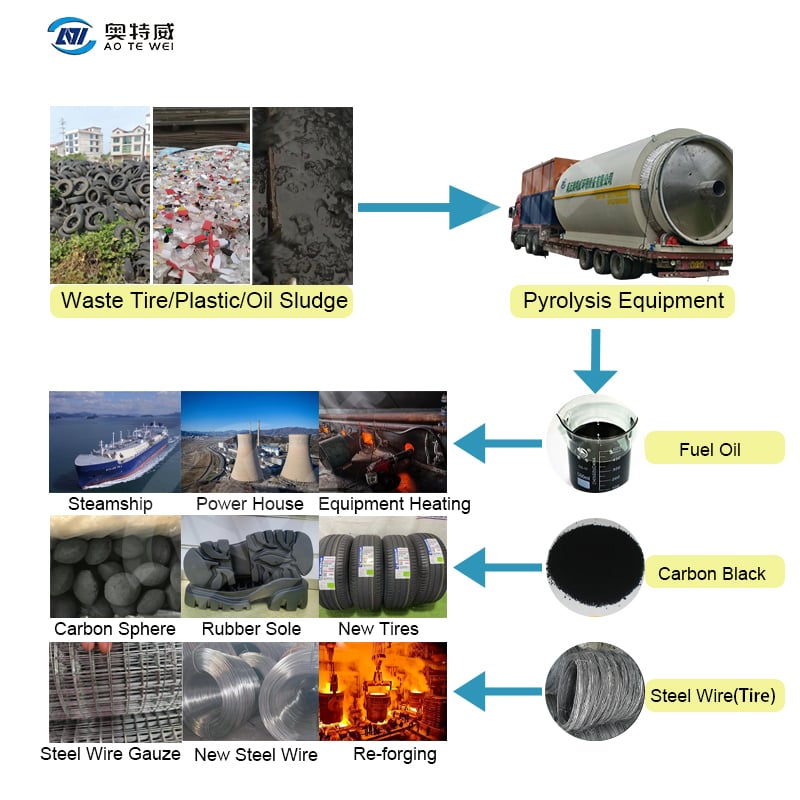
Commercial tire recycling represents a vital environmental and economic solution for managing end-of-life tires across industries. This process transforms discarded tires into valuable resources through advanced mechanical and chemical processes. Commercial tire recycling involves shredding, grinding, and separating tire components to recover rubber, steel, and textile materials for reuse.
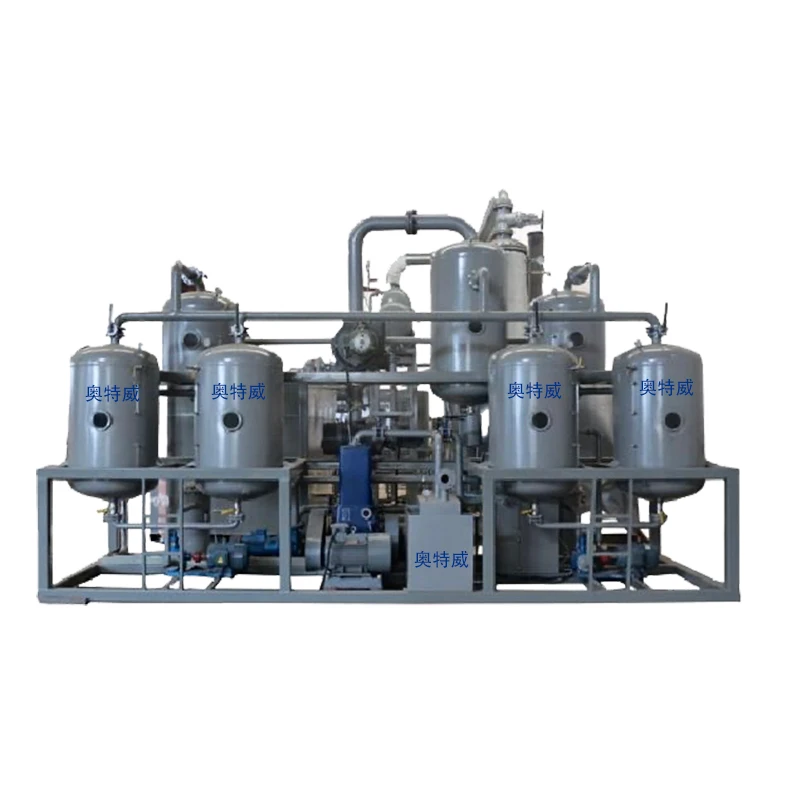
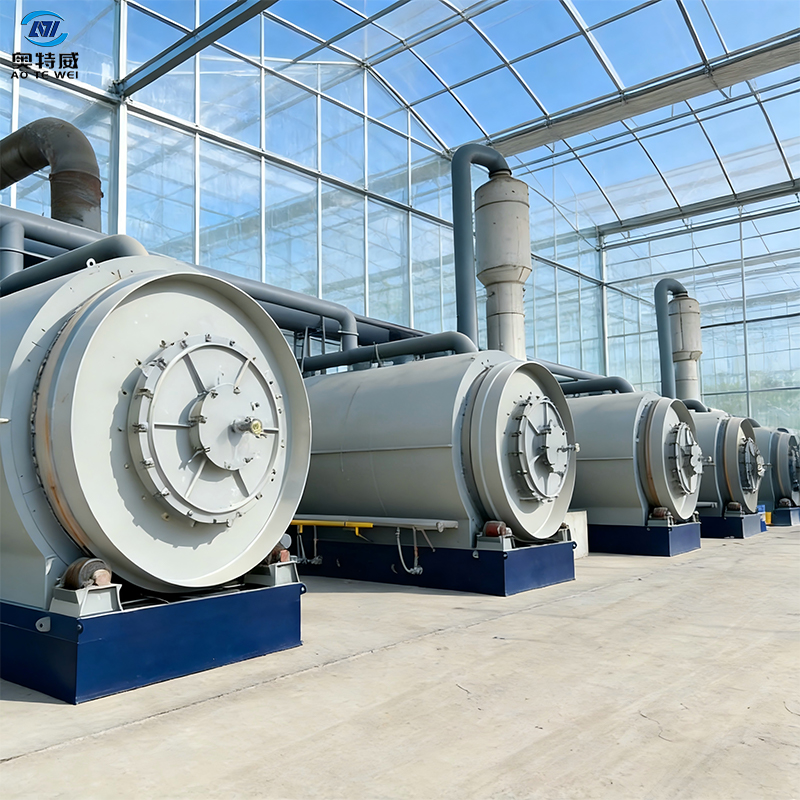
The main functions of commercial tire recycling include reducing landfill waste, conserving natural resources, and creating sustainable materials for new applications. Modern commercial tire recycling facilities utilize state-of-the-art technology including automated sorting systems, cryogenic grinding equipment, and magnetic separation devices that efficiently process thousands of tires daily. These technological features enable precise material separation and high-quality output.
Applications for recycled tire materials are extensive and diverse. Recycled rubber from commercial tire recycling serves construction projects, playground surfaces, athletic tracks, and industrial applications. Steel recovered through commercial tire recycling finds use in manufacturing new vehicles and machinery. Textile fibers become components in automotive parts and household products. The versatility of commercial tire recycling materials makes this process essential for multiple industries seeking sustainable alternatives to virgin materials, supporting both environmental conservation and cost-effective manufacturing solutions.