Scrap Tire Recycling Equipment Solutions

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

scrap tire recycling equipment

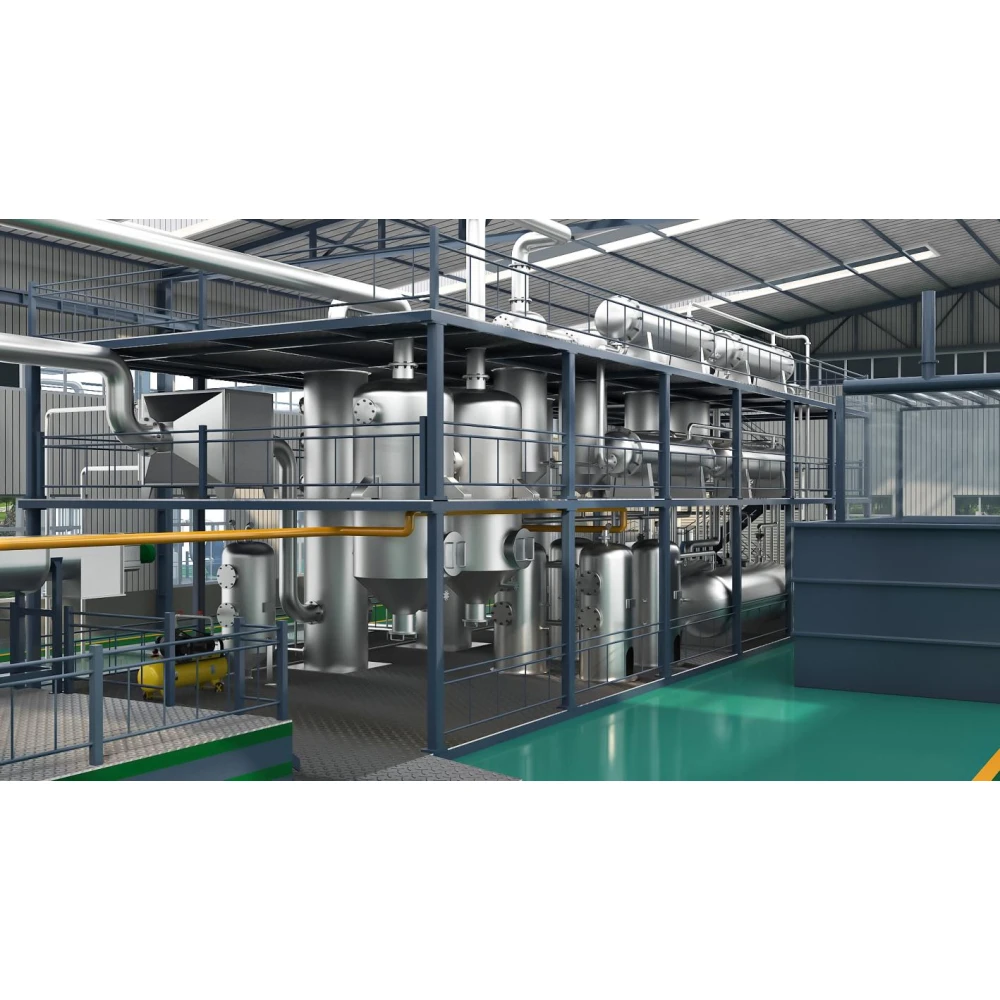
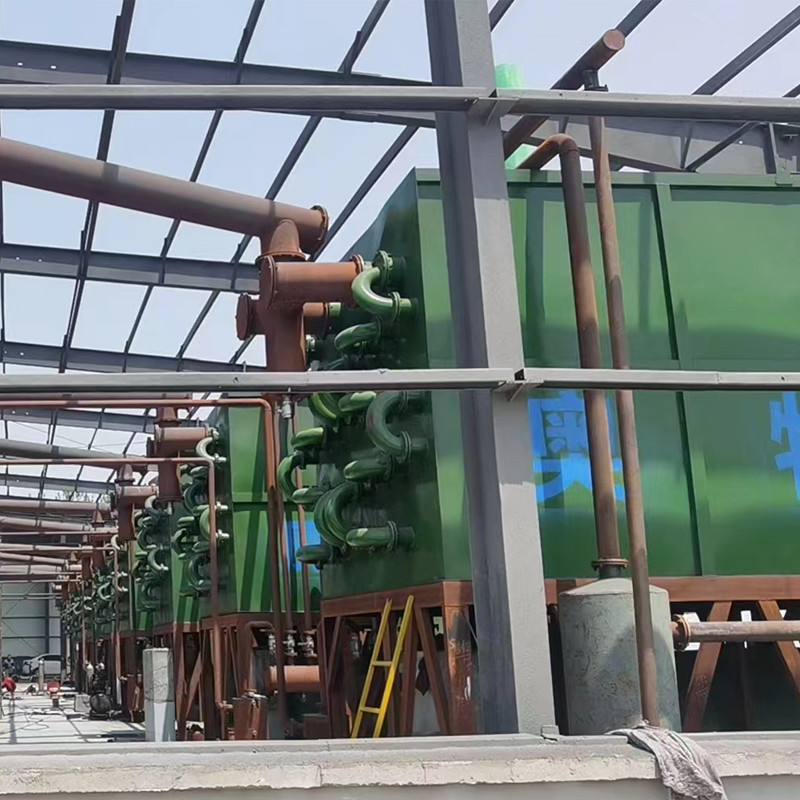
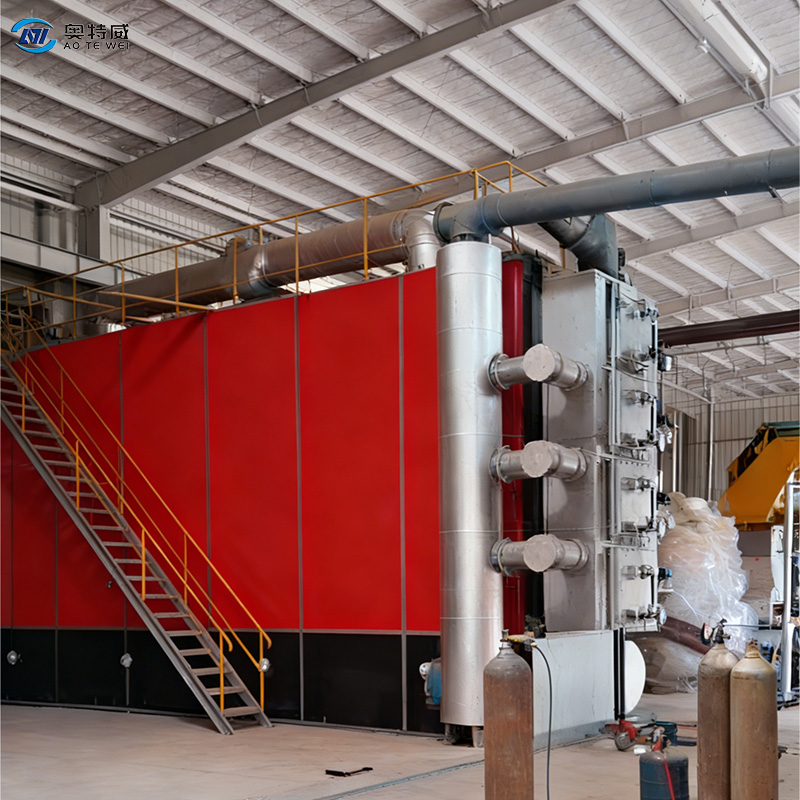
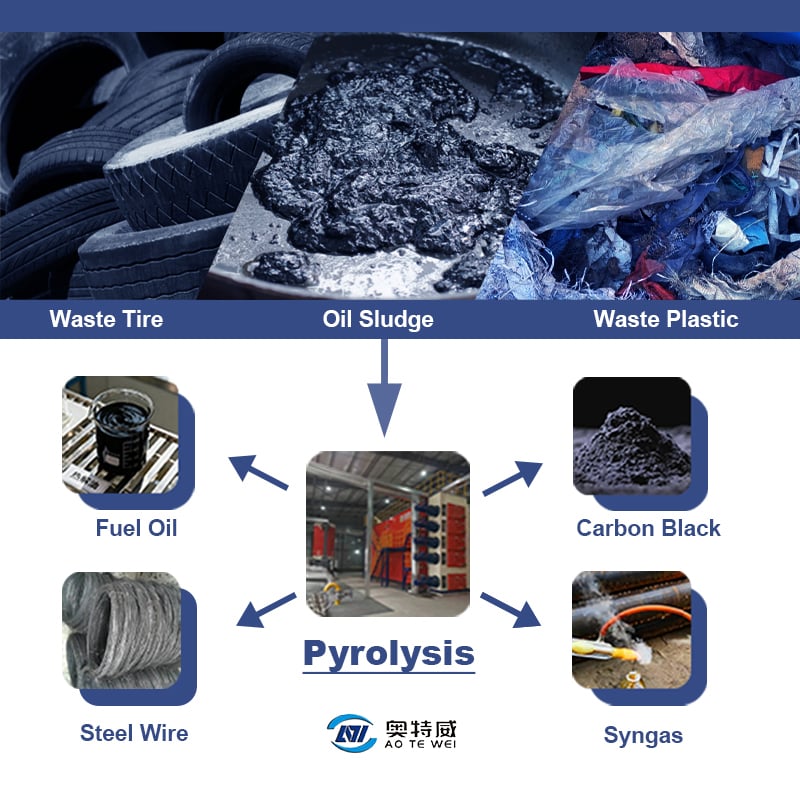
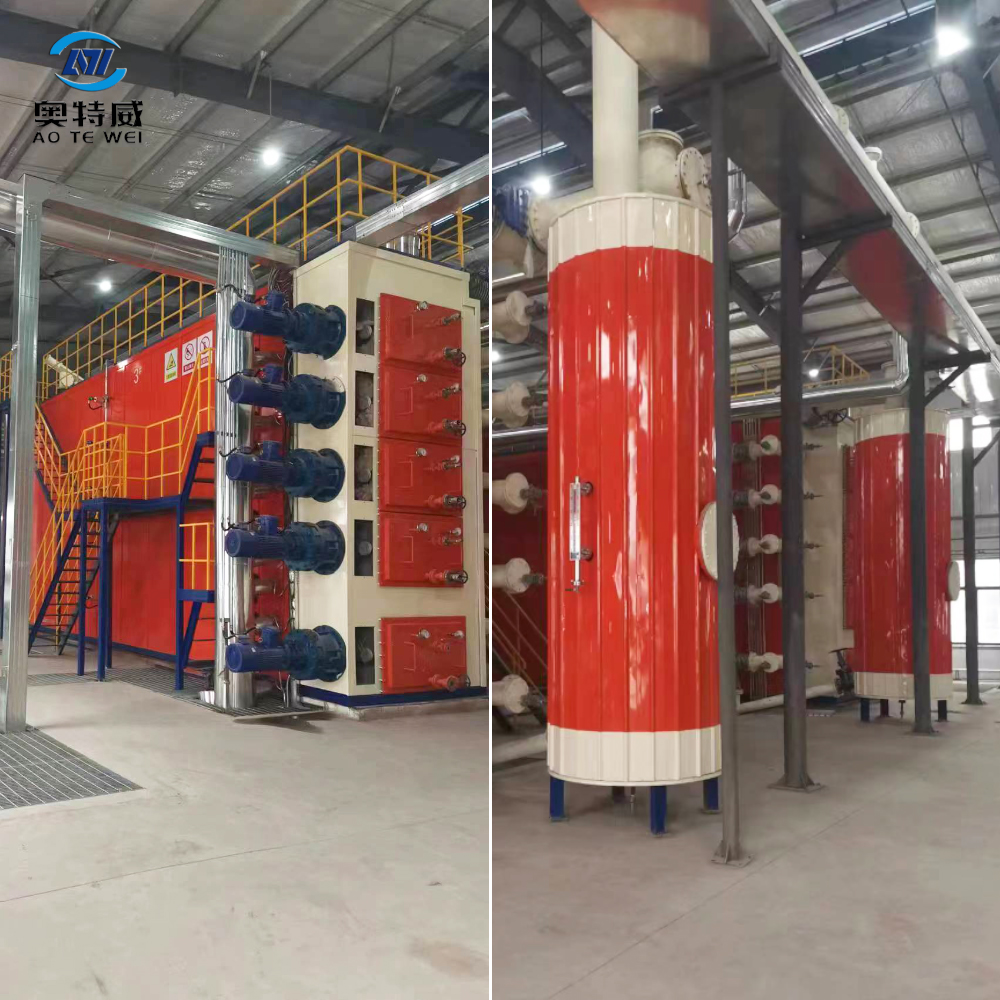
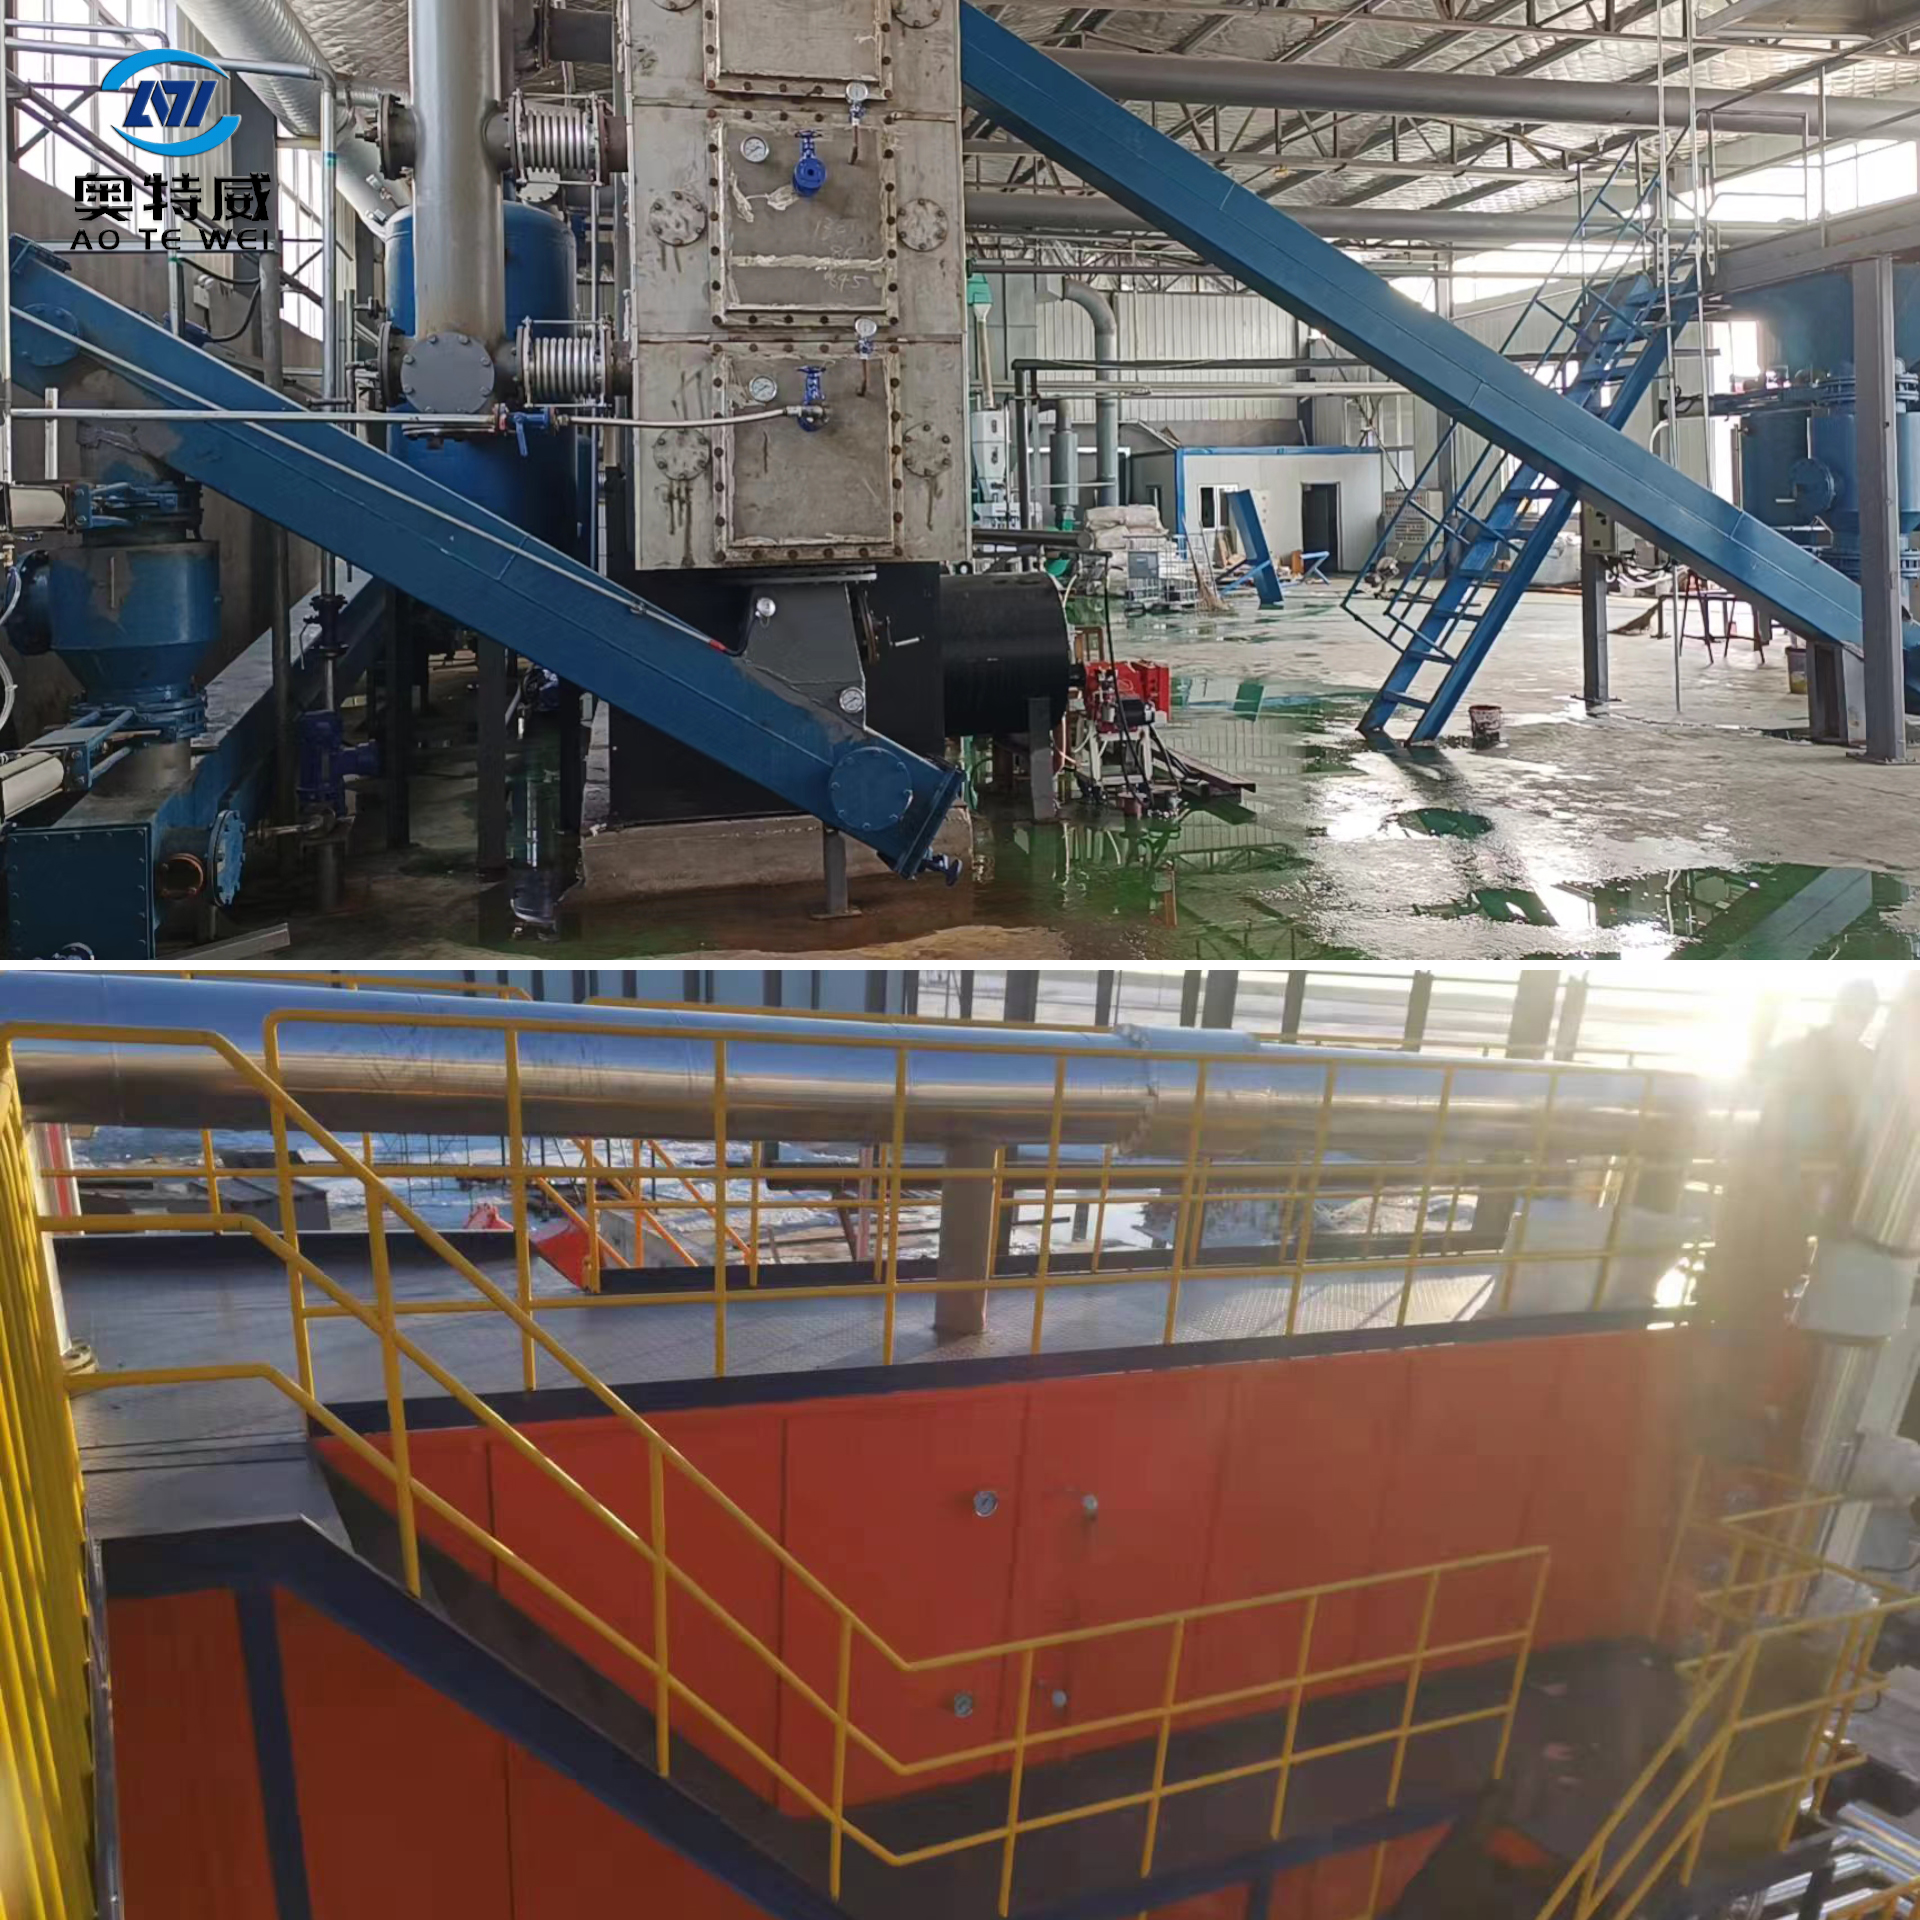
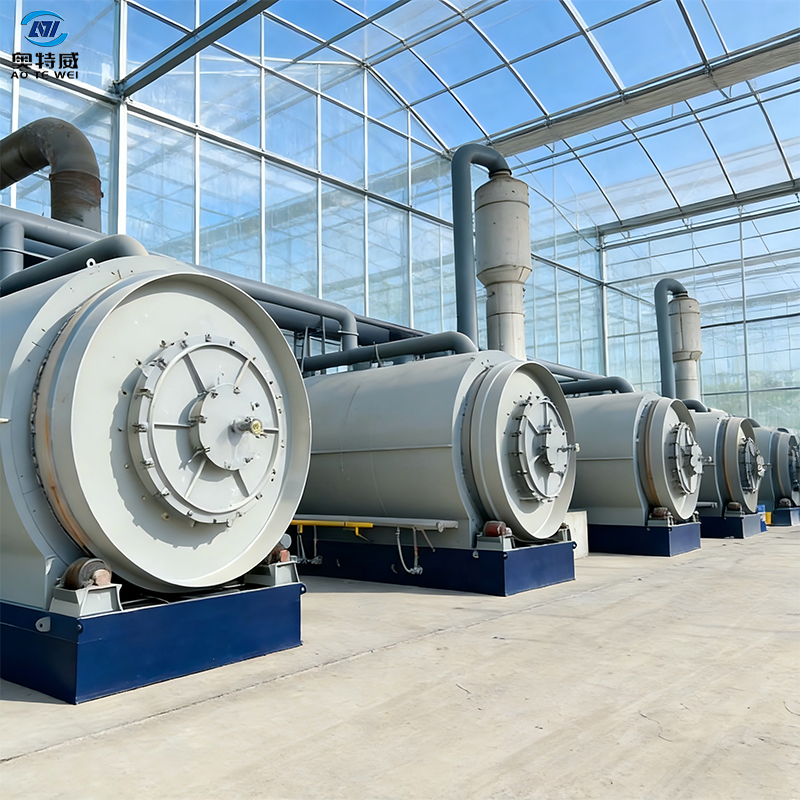
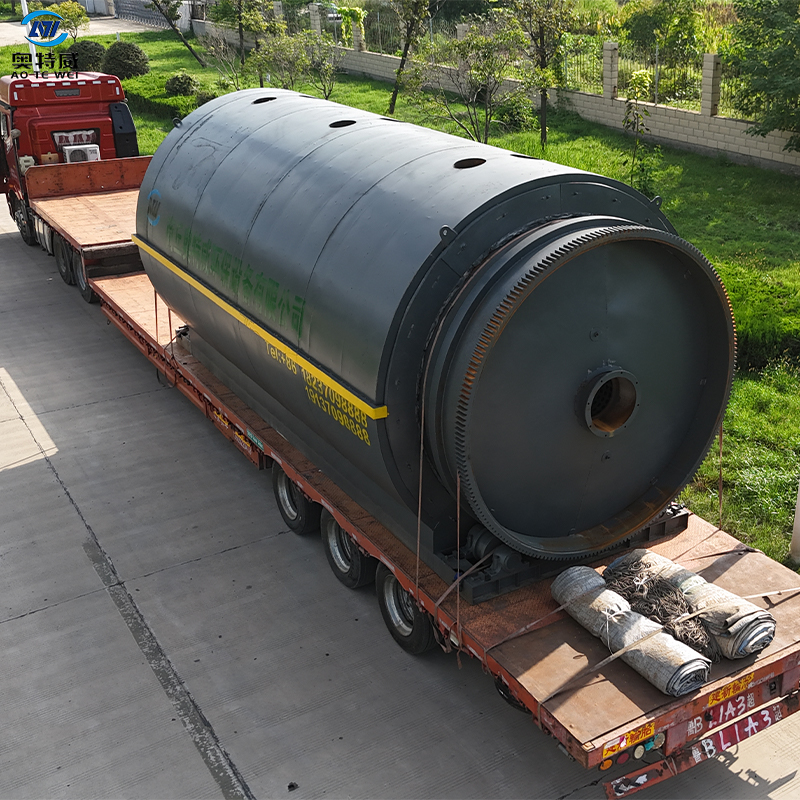
Scrap tire recycling equipment represents a transformative solution for managing end-of-life tires through advanced mechanical and technological processes. This specialized machinery is designed to break down used tires into valuable secondary materials, including rubber granules, steel wire, and textile fibers. The primary function of scrap tire recycling equipment involves shredding, grinding, and separating tire components into reusable raw materials that serve diverse industrial applications. Modern scrap tire recycling equipment incorporates sophisticated technological features including automated feeding systems, high-powered grinding mechanisms, and multi-stage separation technology. These systems utilize precision-engineered cutting tools and intelligent sorting mechanisms to maximize material recovery efficiency. The equipment operates through carefully controlled processes that preserve material quality while minimizing energy consumption and environmental impact. Applications for scrap tire recycling equipment extend across numerous industries. Recycled rubber from this equipment feeds into playground surfaces, athletic tracks, and construction materials. Steel components recovered through scrap tire recycling equipment processing supply metalworking industries, while recovered textile fibers support fabric and geotextile manufacturing. Environmental benefits include substantial waste reduction, landfill diversion, and conservation of natural resources. Industries ranging from construction and manufacturing to sports facility development increasingly depend on scrap tire recycling equipment to source sustainable, cost-effective materials that meet growing ecological standards and regulatory requirements.
New Product Recommendations

Scrap tire recycling equipment delivers compelling operational and financial benefits for waste management facilities, material recovery operations, and manufacturing enterprises. The most significant advantage lies in resource recovery efficiency. This equipment transforms waste tires into three distinct material streams—rubber, steel, and textiles—each commanding substantial market value. Operators experience immediate revenue generation from selling recovered materials, effectively converting disposal costs into profit centers through scrap tire recycling equipment investment. Operational benefits prove equally impressive. Modern scrap tire recycling equipment operates with minimal manual intervention through automated systems that enhance worker safety and reduce labor expenses. The equipment's reliable performance ensures consistent material output, enabling predictable supply chains for downstream industries. Processing capacity scales efficiently, allowing businesses to expand operations without proportional cost increases. Application suitability makes scrap tire recycling equipment indispensable for environmentally conscious organizations. Companies seeking sustainability credentials find that implementing this equipment demonstrates genuine environmental commitment, improving brand reputation and stakeholder relationships. Material recovery reduces landfill dependencies, supporting circular economy principles increasingly required by regulations and consumer expectations. Decision-useful context includes regulatory compliance advantages. Jurisdictions worldwide implement stricter tire disposal regulations, making scrap tire recycling equipment essential for legal operations. Early adoption positions companies ahead of compliance deadlines while competitors scramble for solutions. The equipment's environmental performance also qualifies facilities for tax incentives and grants, further improving financial returns. Integration of scrap tire recycling equipment represents strategic investment combining profitability, sustainability, operational excellence, and regulatory certainty into one comprehensive solution.

Latest News

How does oil distillation improve purity and usability of recycled oil products?

01

Sep

How does oil distillation improve purity and usability of recycled oil products?

Oil distillation represents one of the most effective methods for restoring the quality and usability of recycled oil products in modern industrial operations. As environmental regulations tighten and resource costs rise, the ability to recycle used ...
View More
Why are manufacturers investing in plastic pyrolysis technology for sustainability?

30

Jul

Why are manufacturers investing in plastic pyrolysis technology for sustainability?

Across the global manufacturing sector, plastic pyrolysis has rapidly moved from a niche concept to a strategic priority. As regulatory pressure on plastic waste intensifies and corporate sustainability commitments become binding targets, manufacture...
View More
How does rubber recycling improve material reuse in manufacturing industries?

01

Sep

How does rubber recycling improve material reuse in manufacturing industries?

Rubber recycling represents one of the most effective strategies for transforming industrial waste into valuable manufacturing resources. As manufacturing industries face increasing pressure to reduce environmental footprints and optimize material co...
View More
Why do factories implement oil recycling systems for cost-saving benefits?

03

Sep

Why do factories implement oil recycling systems for cost-saving benefits?

Factories across industries are increasingly turning to oil recycling as a strategic approach to managing operational costs while addressing environmental responsibility. The decision to implement oil recycling systems goes far beyond simple waste ma...
View More

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

scrap tire recycling equipment

Advanced Material Separation Technology

Advanced Material Separation Technology

Scrap tire recycling equipment incorporates cutting-edge separation systems that efficiently isolate rubber, steel, and textile components with unprecedented precision. This technological advancement ensures maximum material purity and market value for each recovered fraction. The multi-stage separation process utilizes magnetic extraction, density sorting, and fiber separation mechanisms working in seamless coordination. Superior separation efficiency directly translates to higher-quality materials commanding premium prices in secondary markets. Manufacturers utilizing scrap tire recycling equipment benefit from consistently pure material streams that meet strict industrial standards. This advanced capability reduces contamination costs, minimizes reprocessing requirements, and enhances customer satisfaction across material buyers. The investment in precision separation technology represents intelligent business strategy, transforming traditional waste management into profitable material production operations.
Energy-Efficient Processing Systems

Energy-Efficient Processing Systems

Modern scrap tire recycling equipment features intelligent energy management systems that dramatically reduce operational costs while maintaining processing efficiency. Advanced motor controls, optimized grinding mechanisms, and thermal management systems work collectively to minimize power consumption. These energy-efficient innovations reduce electricity expenses significantly, improving bottom-line profitability without compromising equipment performance. Operators benefit from reduced environmental footprint and lower carbon emissions associated with scrap tire recycling equipment operation. The energy-efficient design also extends equipment lifespan by reducing mechanical stress and heat generation during processing cycles. Facilities implementing this equipment experience measurable reductions in utility bills, creating sustainable competitive advantages. Investment in energy-conscious scrap tire recycling equipment demonstrates environmental responsibility while delivering concrete financial savings that accumulate substantially over operational years.
High-Volume Processing Capacity

High-Volume Processing Capacity

Scrap tire recycling equipment delivers exceptional throughput capabilities, processing substantial tire volumes efficiently within compact operational footprints. Industrial-scale models handle hundreds of tires daily, making mass recycling economically viable for large-scale operations. This impressive processing capacity enables businesses to service entire regional waste streams, establishing dominant market positions within their geographic areas. Operators achieve rapid material inventory accumulation, enabling consistent material supply to manufacturing customers and supporting stable revenue streams. The equipment's scalable design accommodates facility expansion without requiring complete system replacement or extensive infrastructure modifications. High-volume processing capacity inherent to scrap tire recycling equipment makes large-scale tire management profitable and operationally feasible for enterprises committed to comprehensive waste solutions.

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000
Newsletter
Please Leave A Message With Us