Distillation Factory | Industrial Separation Solutions

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

distillation factory

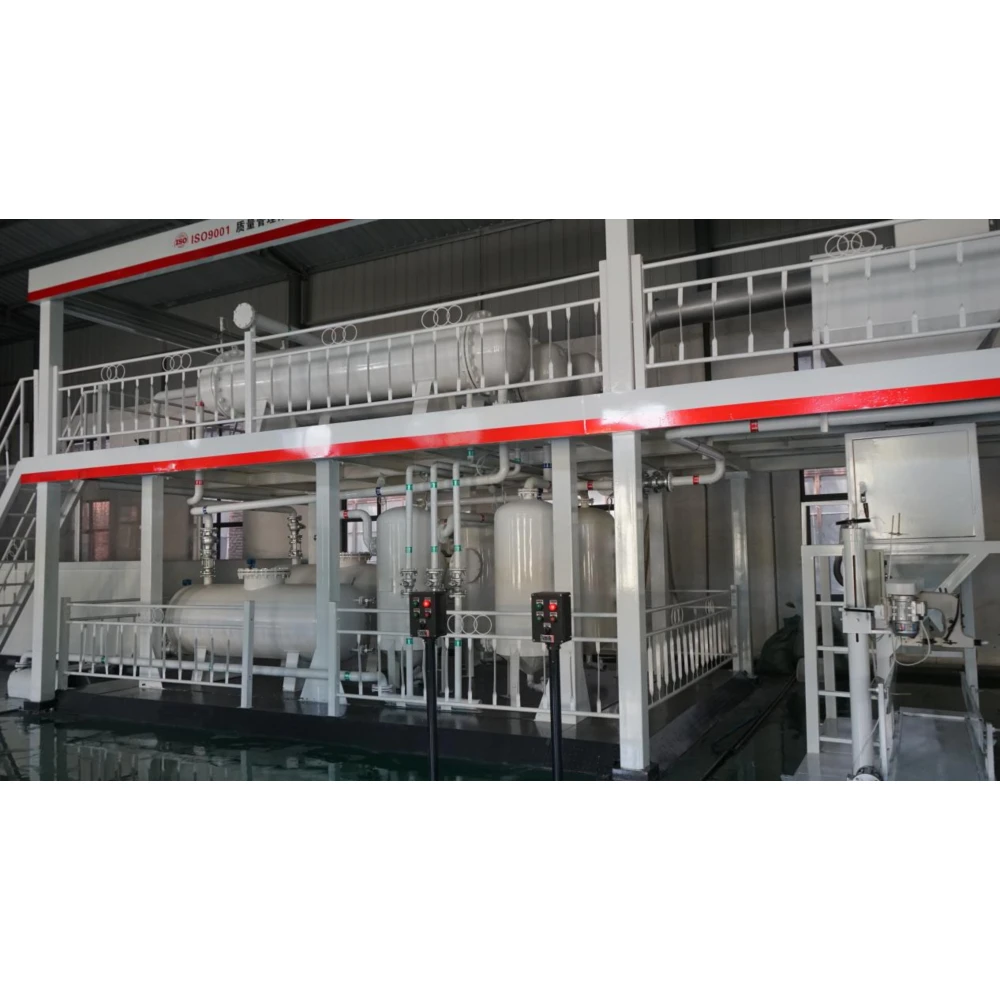
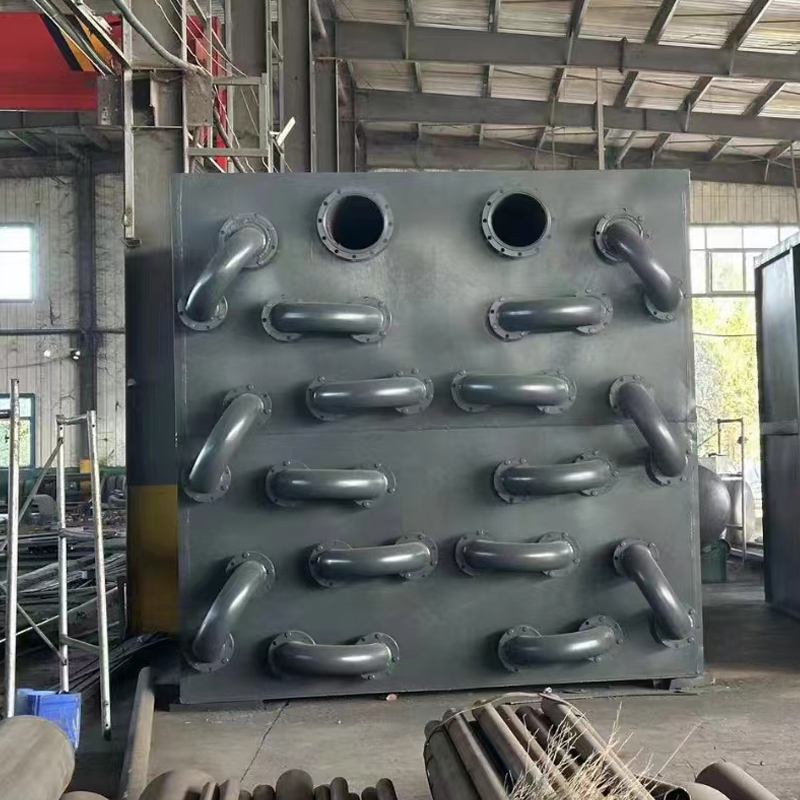
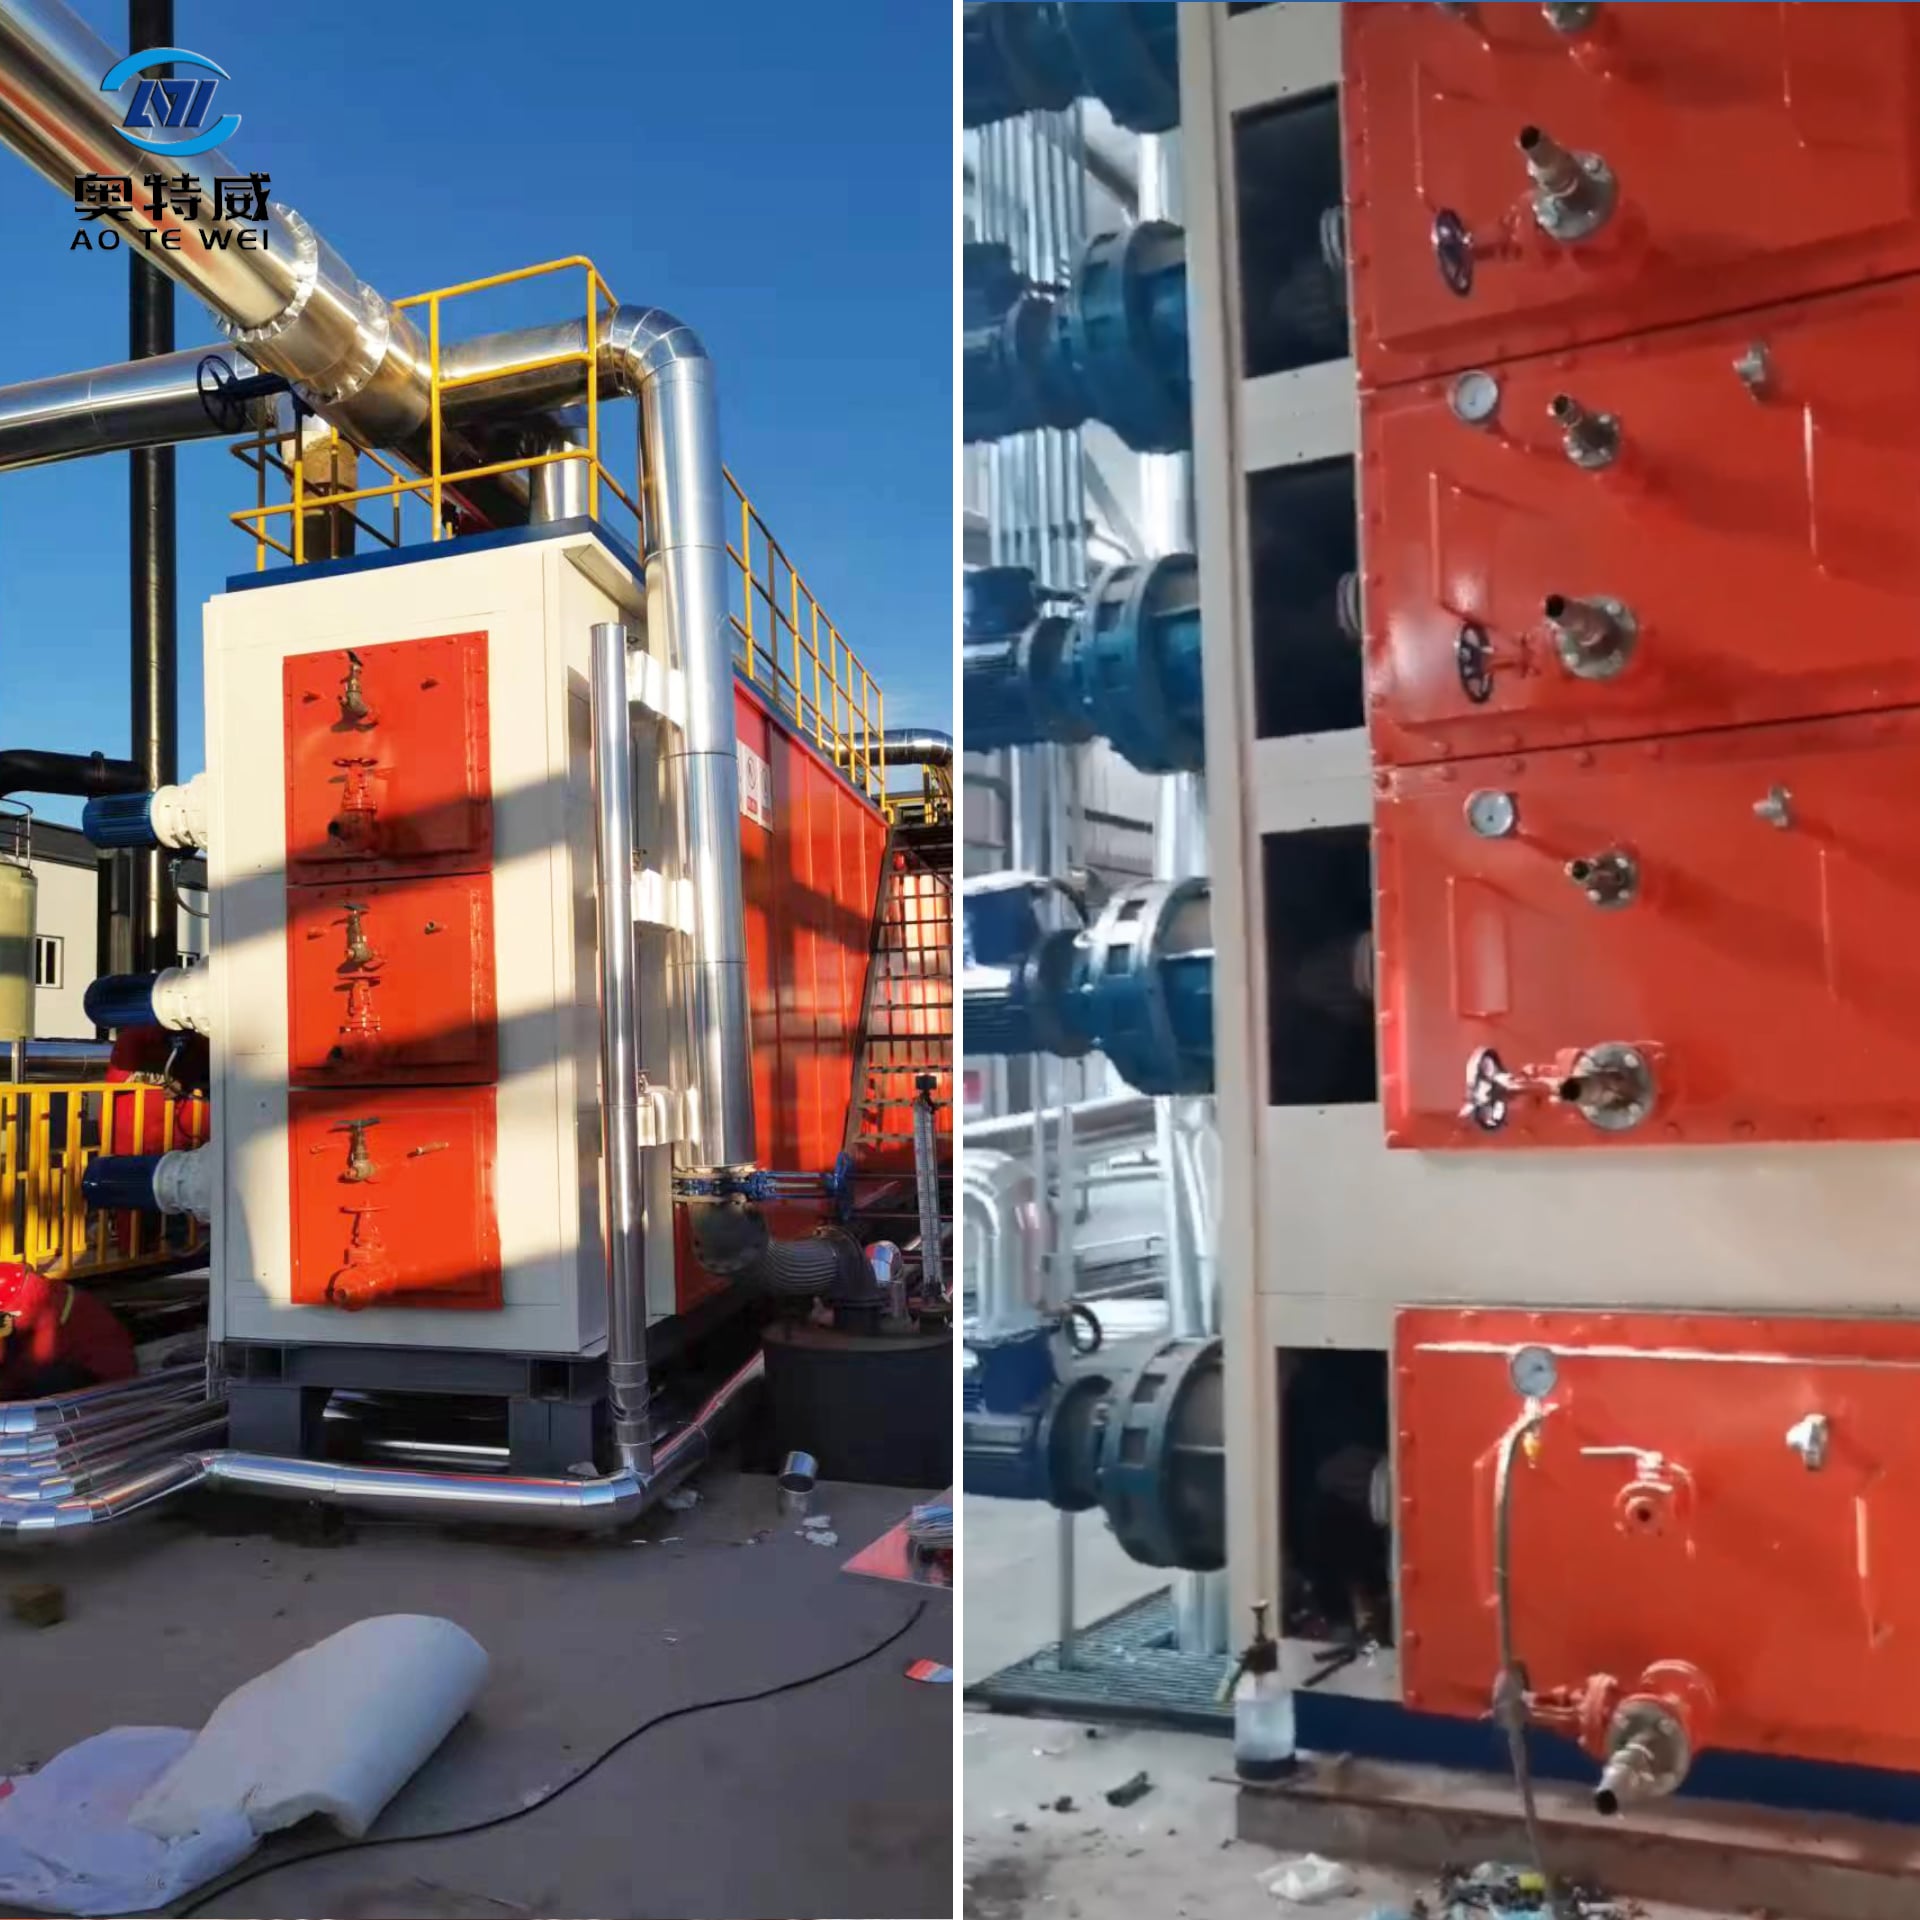
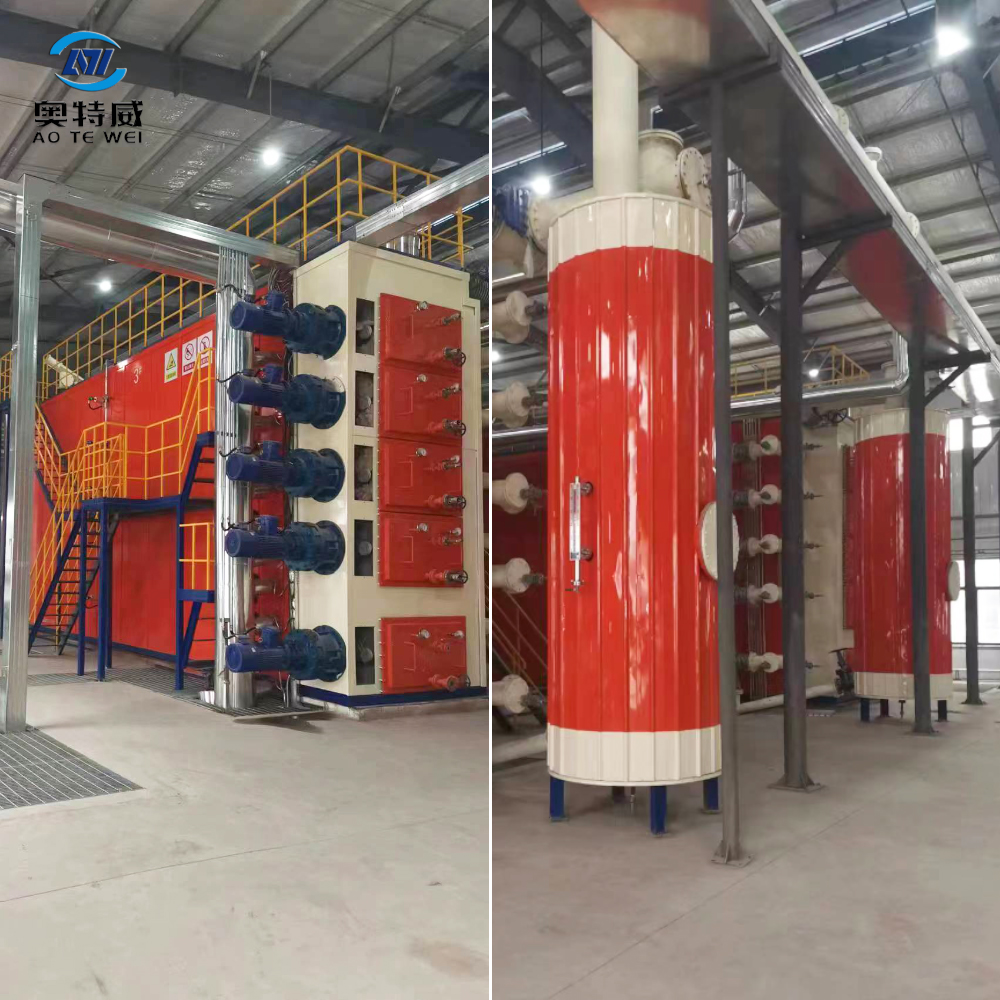
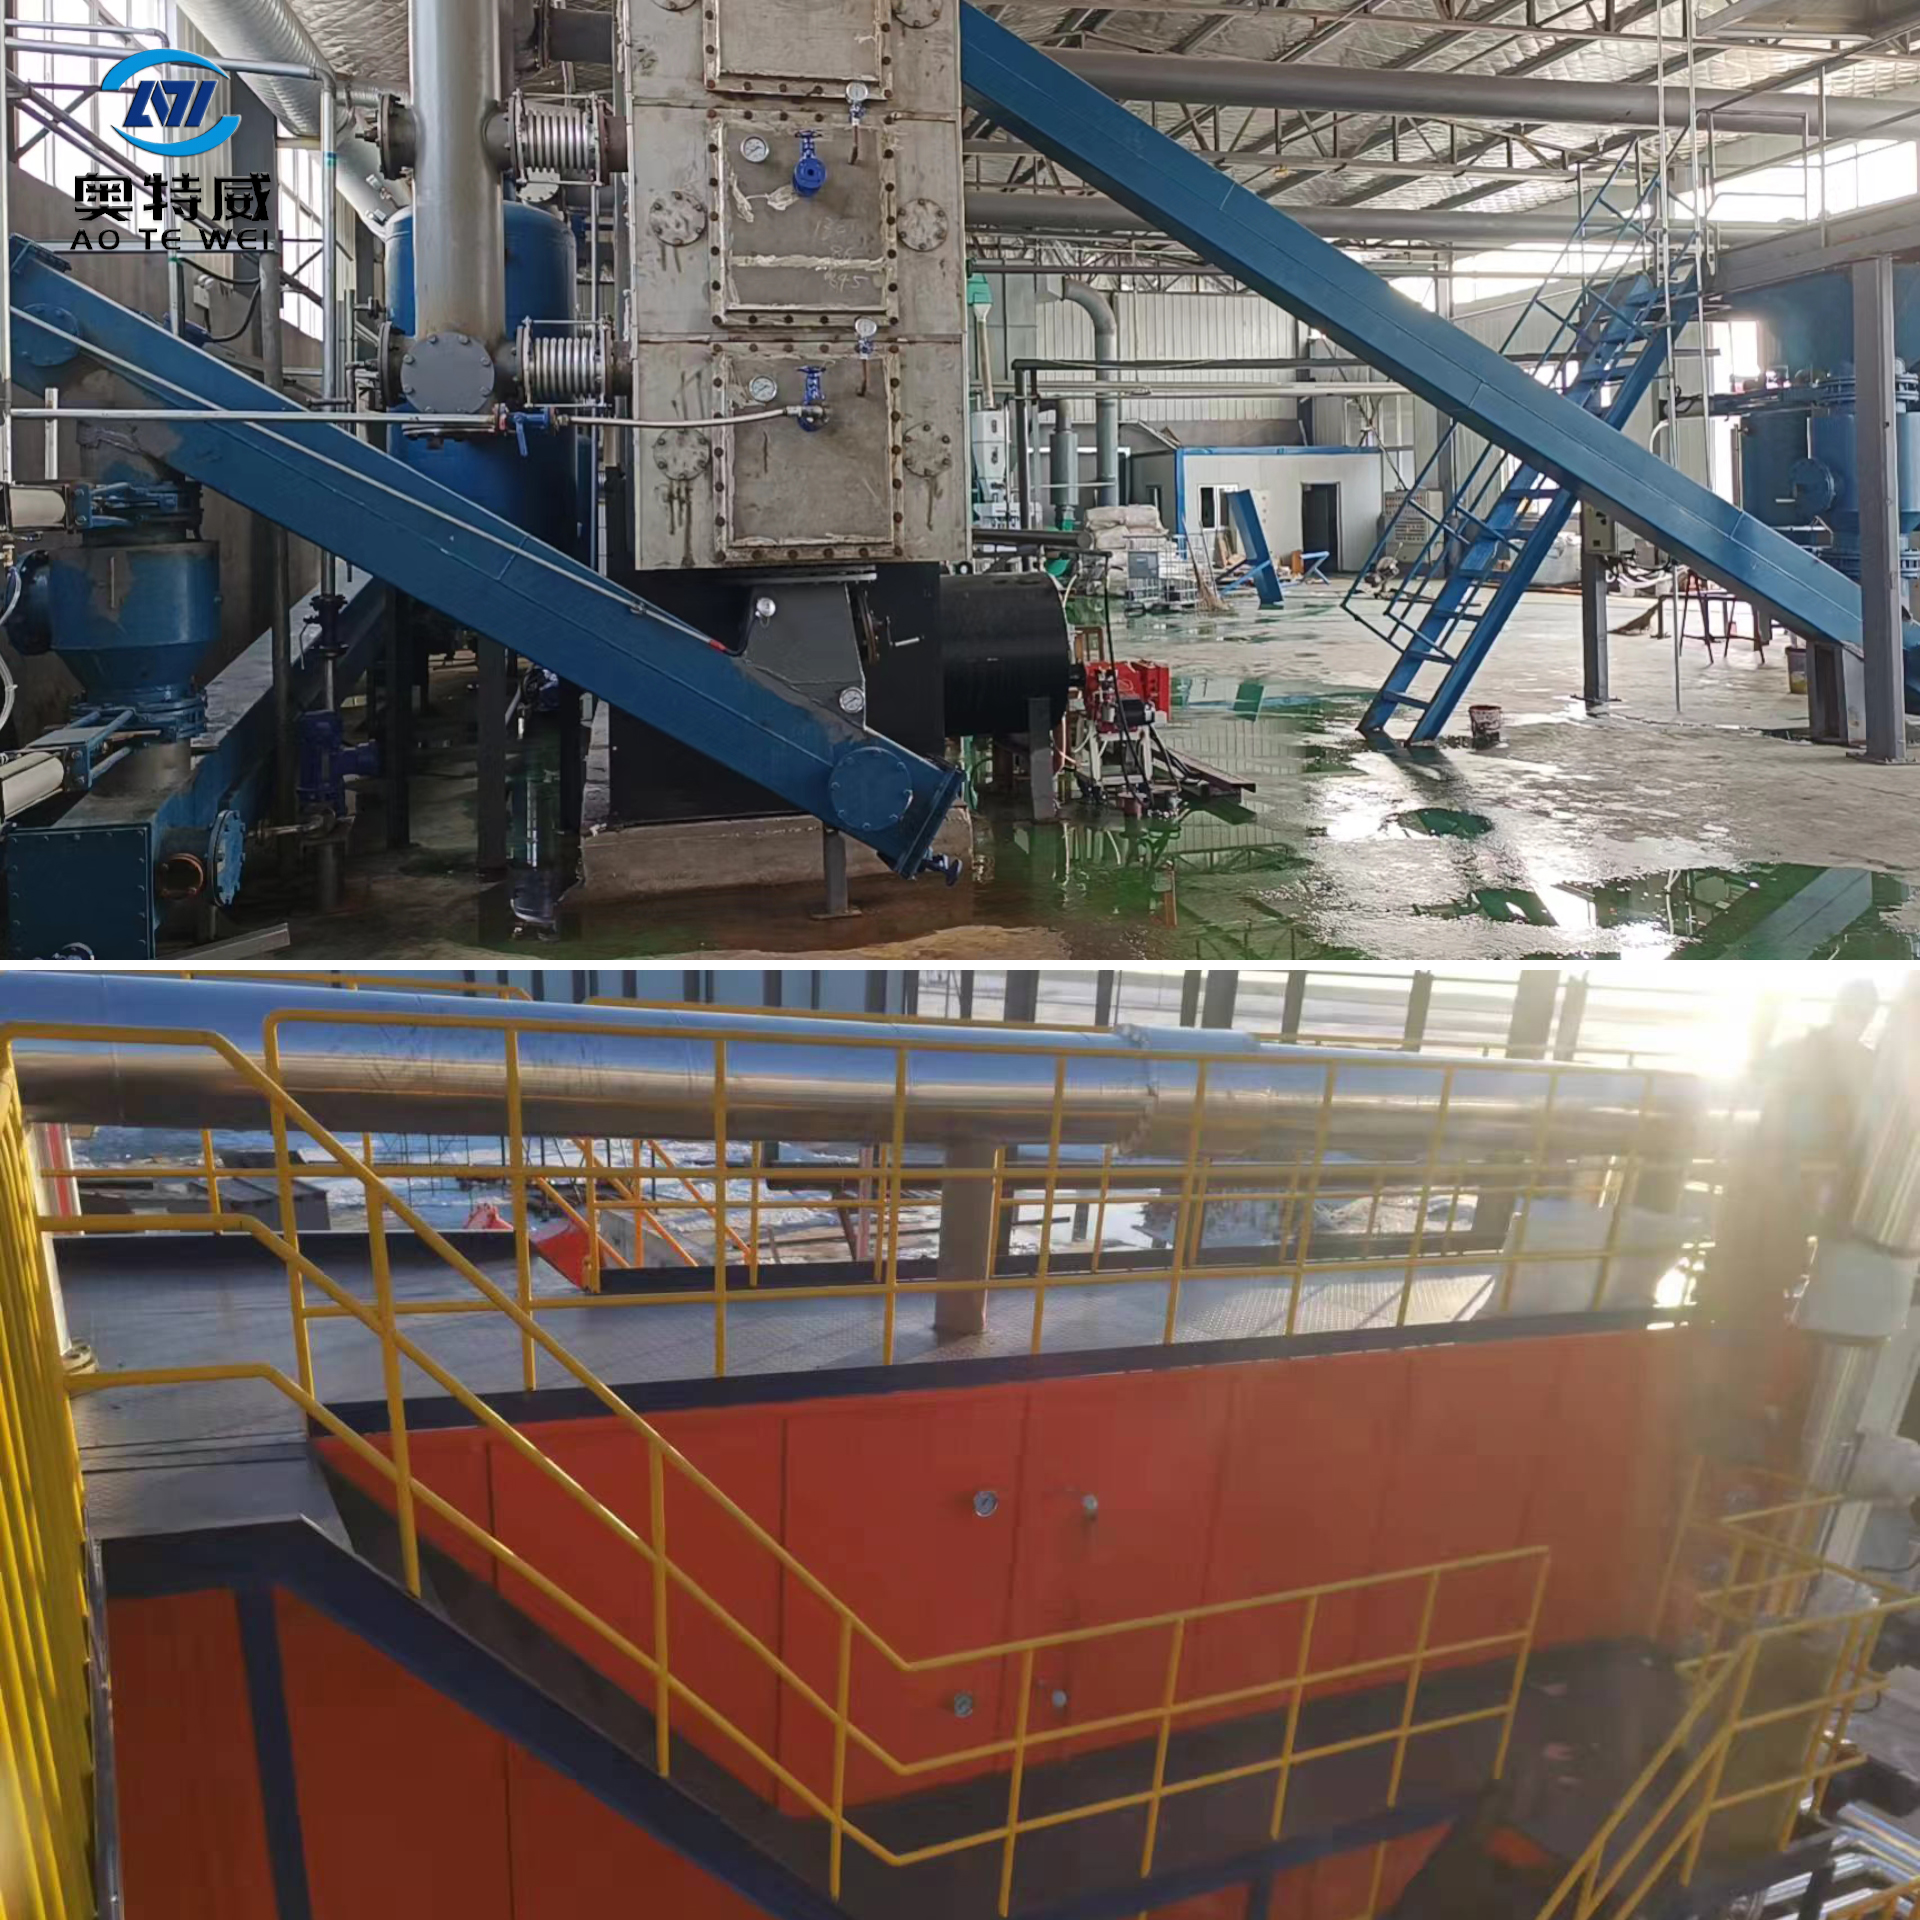
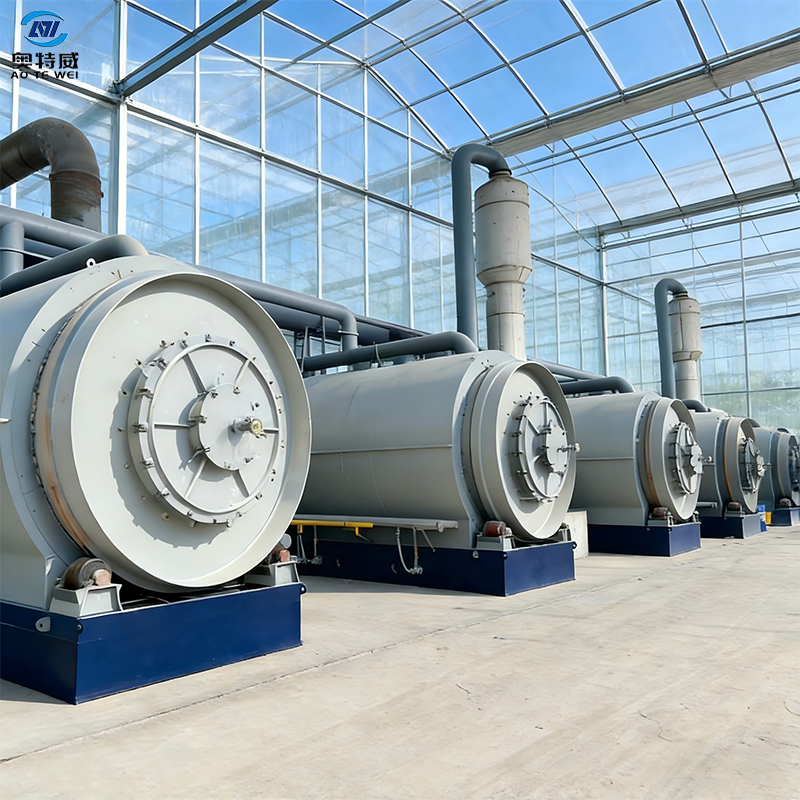
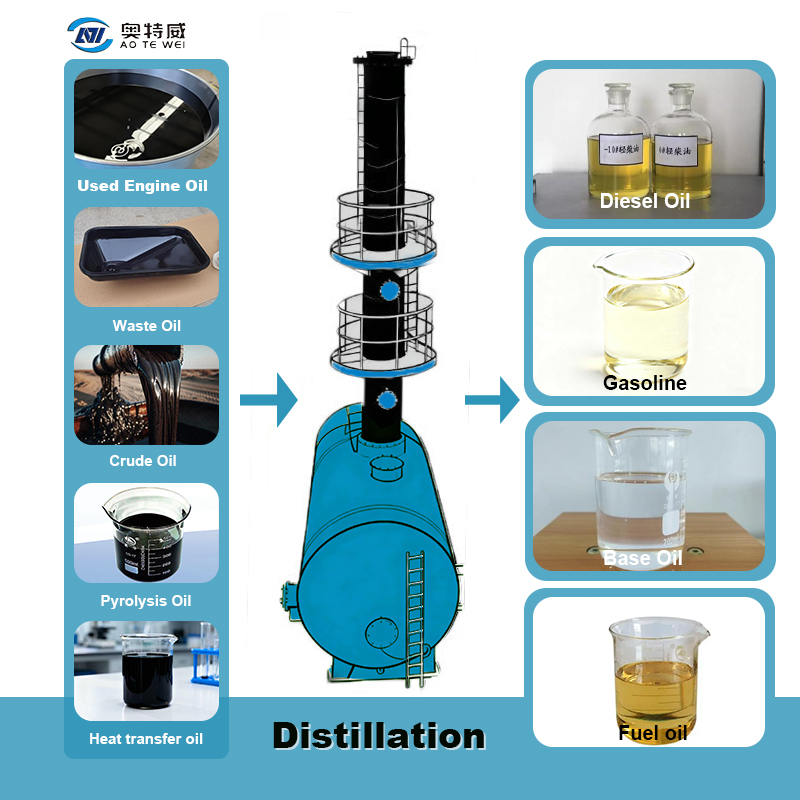
A distillation factory is a specialized industrial facility designed to separate liquid mixtures into pure components through the distillation process. This sophisticated operation relies on the principle of heating liquids to create vapor, then cooling and condensing that vapor back into liquid form. The distillation factory serves as a critical hub in numerous industries, including petroleum refining, chemical production, pharmaceutical manufacturing, and beverage production. The distillation factory operates using advanced technological features that ensure precision and efficiency. Modern distillation factories employ fractional distillation columns, vacuum distillation systems, and steam distillation technologies to achieve optimal separation results. These systems allow operators to control temperature, pressure, and residence time with remarkable accuracy, ensuring consistent product quality. Key functions of a distillation factory include purifying crude oil into gasoline, diesel, and kerosene, extracting essential oils from botanical materials, producing high-purity chemicals and solvents, and concentrating alcoholic beverages. The distillation factory processes large volumes of raw materials daily, transforming them into valuable products through continuous or batch processing methods. Applications of a distillation factory extend across diverse sectors. In the petroleum industry, it refines crude oil into marketable fuels. In pharmaceuticals, it produces purified active ingredients. In the beverage industry, it creates spirits and other concentrated products. The distillation factory's versatility makes it indispensable for companies seeking to extract maximum value from their raw materials while maintaining strict quality standards and regulatory compliance.
New Product Recommendations

Choosing a distillation factory for your separation and purification needs delivers substantial operational and financial benefits that transform your production capabilities. A modern distillation factory significantly improves product purity levels, ensuring that your final outputs meet the highest industry standards and customer expectations. This enhanced quality directly translates to increased market competitiveness and customer satisfaction. The distillation factory provides exceptional operational efficiency through continuous processing capabilities and automated control systems. Your production team can monitor and adjust parameters in real time, reducing downtime and maximizing throughput. This operational advantage means your distillation factory processes materials faster while consuming less energy than traditional methods, directly impacting your bottom line. Investing in a distillation factory delivers remarkable cost savings across multiple areas. Reduced energy consumption, minimized product losses, and lower maintenance requirements combine to decrease your overall operational expenses substantially. The distillation factory's advanced design prevents contamination and waste, ensuring that more of your raw materials convert into sellable products. A distillation factory offers unmatched application suitability for various industries and product types. Whether you process petroleum, chemicals, pharmaceuticals, or botanical extracts, the distillation factory adapts to your specific requirements. This flexibility means one facility can handle multiple product lines, maximizing your investment returns. The distillation factory provides decision-useful context for businesses planning expansion or modernization. Its proven track record across industries demonstrates reliability and profitability. By selecting a distillation factory, you gain access to cutting-edge technology that positions your company as an industry leader, attracts quality-conscious customers, and supports sustainable business growth for years to come.

Tips And Tricks

Why do recycling plants rely on pyrolysis reactor technology for energy recovery?

01

Sep

Why do recycling plants rely on pyrolysis reactor technology for energy recovery?

Modern recycling plants face mounting pressure to recover maximum value from waste streams while maintaining environmental compliance. The pyrolysis reactor has emerged as a critical technology for achieving this balance, transforming discarded mater...
View More
How does rubber recycling improve material reuse in manufacturing industries?

01

Sep

How does rubber recycling improve material reuse in manufacturing industries?

Rubber recycling represents one of the most effective strategies for transforming industrial waste into valuable manufacturing resources. As manufacturing industries face increasing pressure to reduce environmental footprints and optimize material co...
View More
Why do factories implement oil recycling systems for cost-saving benefits?

03

Sep

Why do factories implement oil recycling systems for cost-saving benefits?

Factories across industries are increasingly turning to oil recycling as a strategic approach to managing operational costs while addressing environmental responsibility. The decision to implement oil recycling systems goes far beyond simple waste ma...
View More
How does plastic pyrolysis improve value recovery from mixed plastic waste streams?

03

Sep

How does plastic pyrolysis improve value recovery from mixed plastic waste streams?

Mixed plastic waste streams present a significant challenge for waste management industries worldwide. Traditional recycling methods struggle to handle contaminated, multi-polymer, or degraded plastics that cannot be mechanically reprocessed into vir...
View More

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

distillation factory

Advanced Separation Technology

Advanced Separation Technology

The distillation factory incorporates state-of-the-art separation technology that delivers unparalleled purity and consistency in your products. Fractional distillation columns within the distillation factory contain multiple theoretical plates, enabling precise component separation at molecular levels. This advanced architecture allows the distillation factory to achieve separation efficiencies exceeding ninety-five percent, significantly outperforming conventional methods. The distillation factory uses sophisticated instrumentation and automated control systems that monitor hundreds of parameters simultaneously. Real-time data analytics enable operators to optimize the distillation factory's performance continuously, adjusting temperatures and pressures to maintain peak efficiency. This technological advantage ensures your distillation factory produces consistent, high-quality outputs batch after batch, reducing variability and improving customer trust in your products.
Energy Efficiency and Cost Reduction

Energy Efficiency and Cost Reduction

Operating a distillation factory delivers substantial energy savings through innovative heat recovery and thermal optimization systems. The distillation factory captures waste heat from condenser operations and redirects it productively, significantly reducing overall energy consumption. Many modern distillation factory designs incorporate vacuum distillation capabilities, which operate at lower temperatures and pressures, consuming less energy while protecting heat-sensitive compounds. The distillation factory's efficient operation translates directly into reduced operating costs that improve profitability. Lower energy bills combine with decreased maintenance requirements and minimal product loss to create compelling financial benefits. Your distillation factory investment begins generating measurable returns within months. The reduced operational expenses allow you to offer competitive pricing while maintaining healthy profit margins, positioning your business advantageously within your market segment and supporting long-term sustainable growth.
Versatile Application Capability

Versatile Application Capability

A distillation factory provides remarkable versatility, processing diverse materials across multiple industries with exceptional results. The distillation factory handles petroleum crude oil, refined chemicals, pharmaceutical precursors, essential oils, alcoholic beverages, and numerous other liquid mixtures. This application diversity means your distillation factory adapts to changing market demands without requiring expensive retrofitting or replacement. The distillation factory's flexible design accommodates batch processing for small-volume specialty products and continuous processing for high-volume commodity production. This capability enables businesses to serve multiple market segments simultaneously, maximizing revenue opportunities. Your distillation factory becomes a strategic asset that supports business expansion into new markets and product categories, protecting your investment while creating growth opportunities that strengthen your competitive position.

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000
Newsletter
Please Leave A Message With Us