Multi Column Distillation Plant Solutions

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

multi column distillation plant

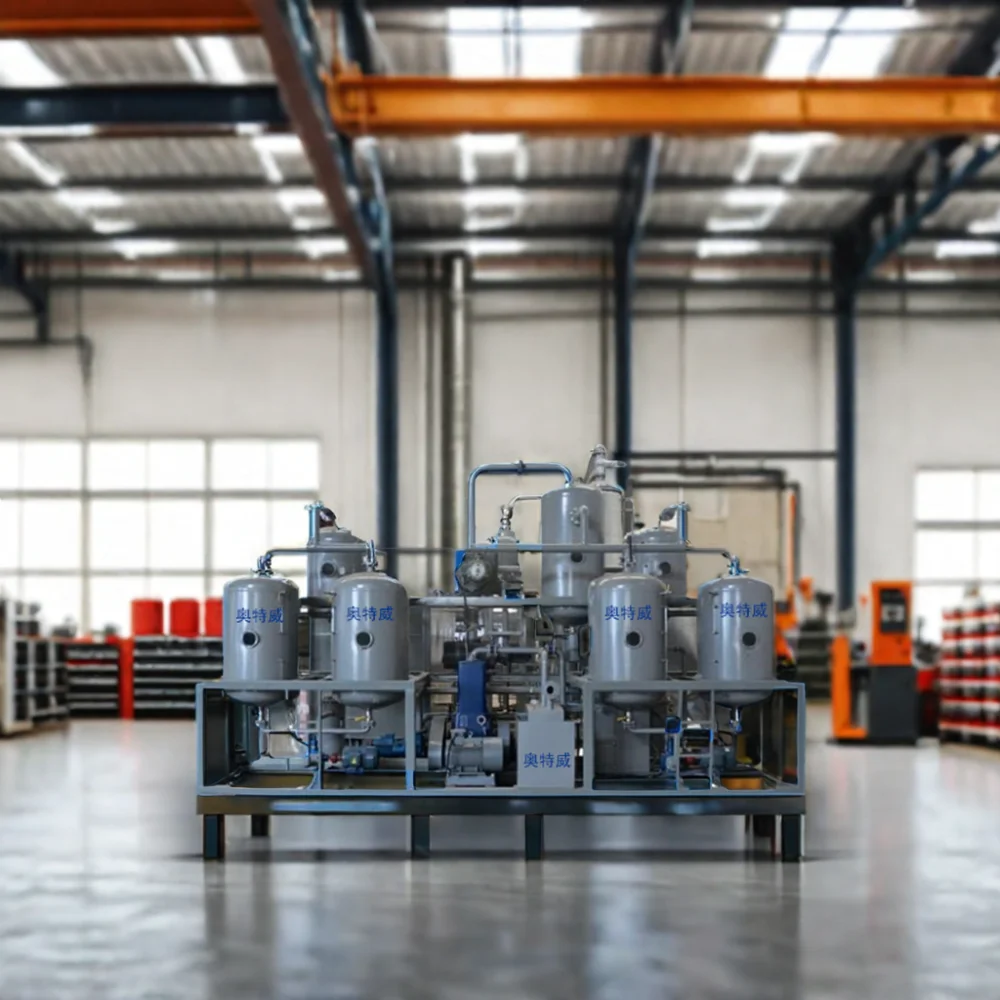
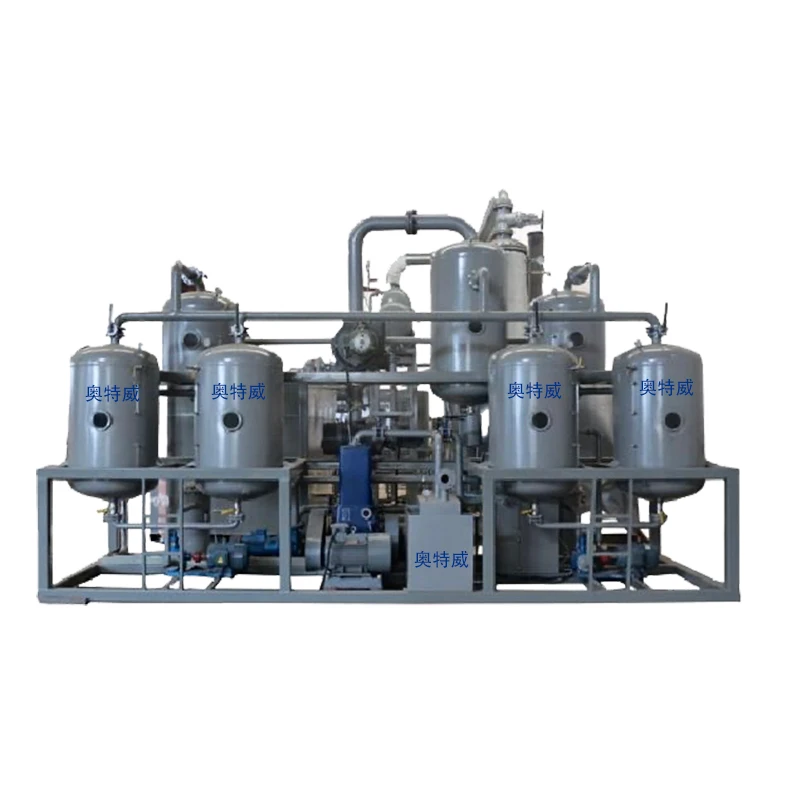
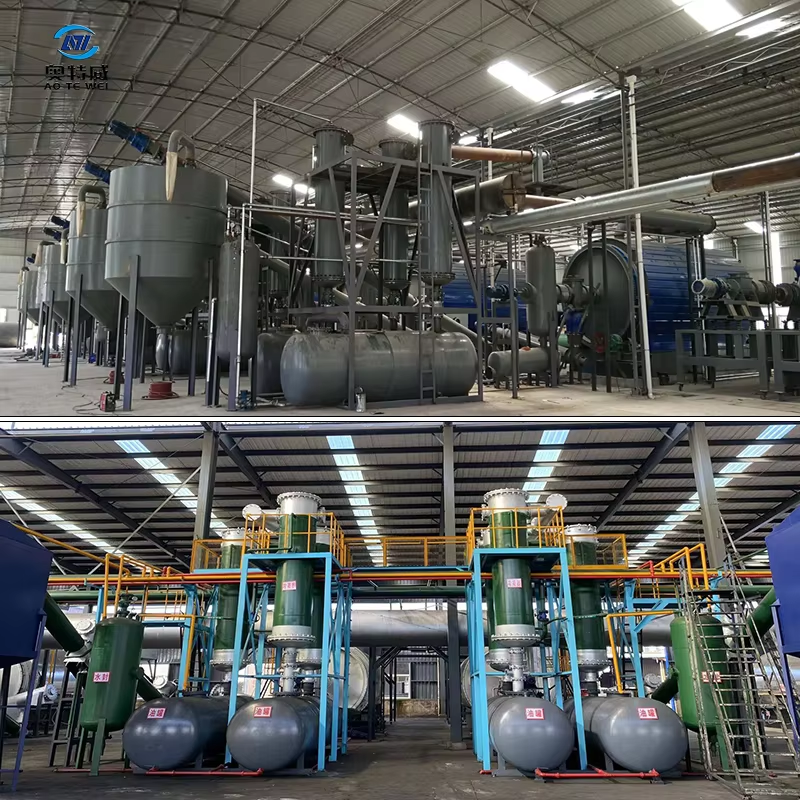
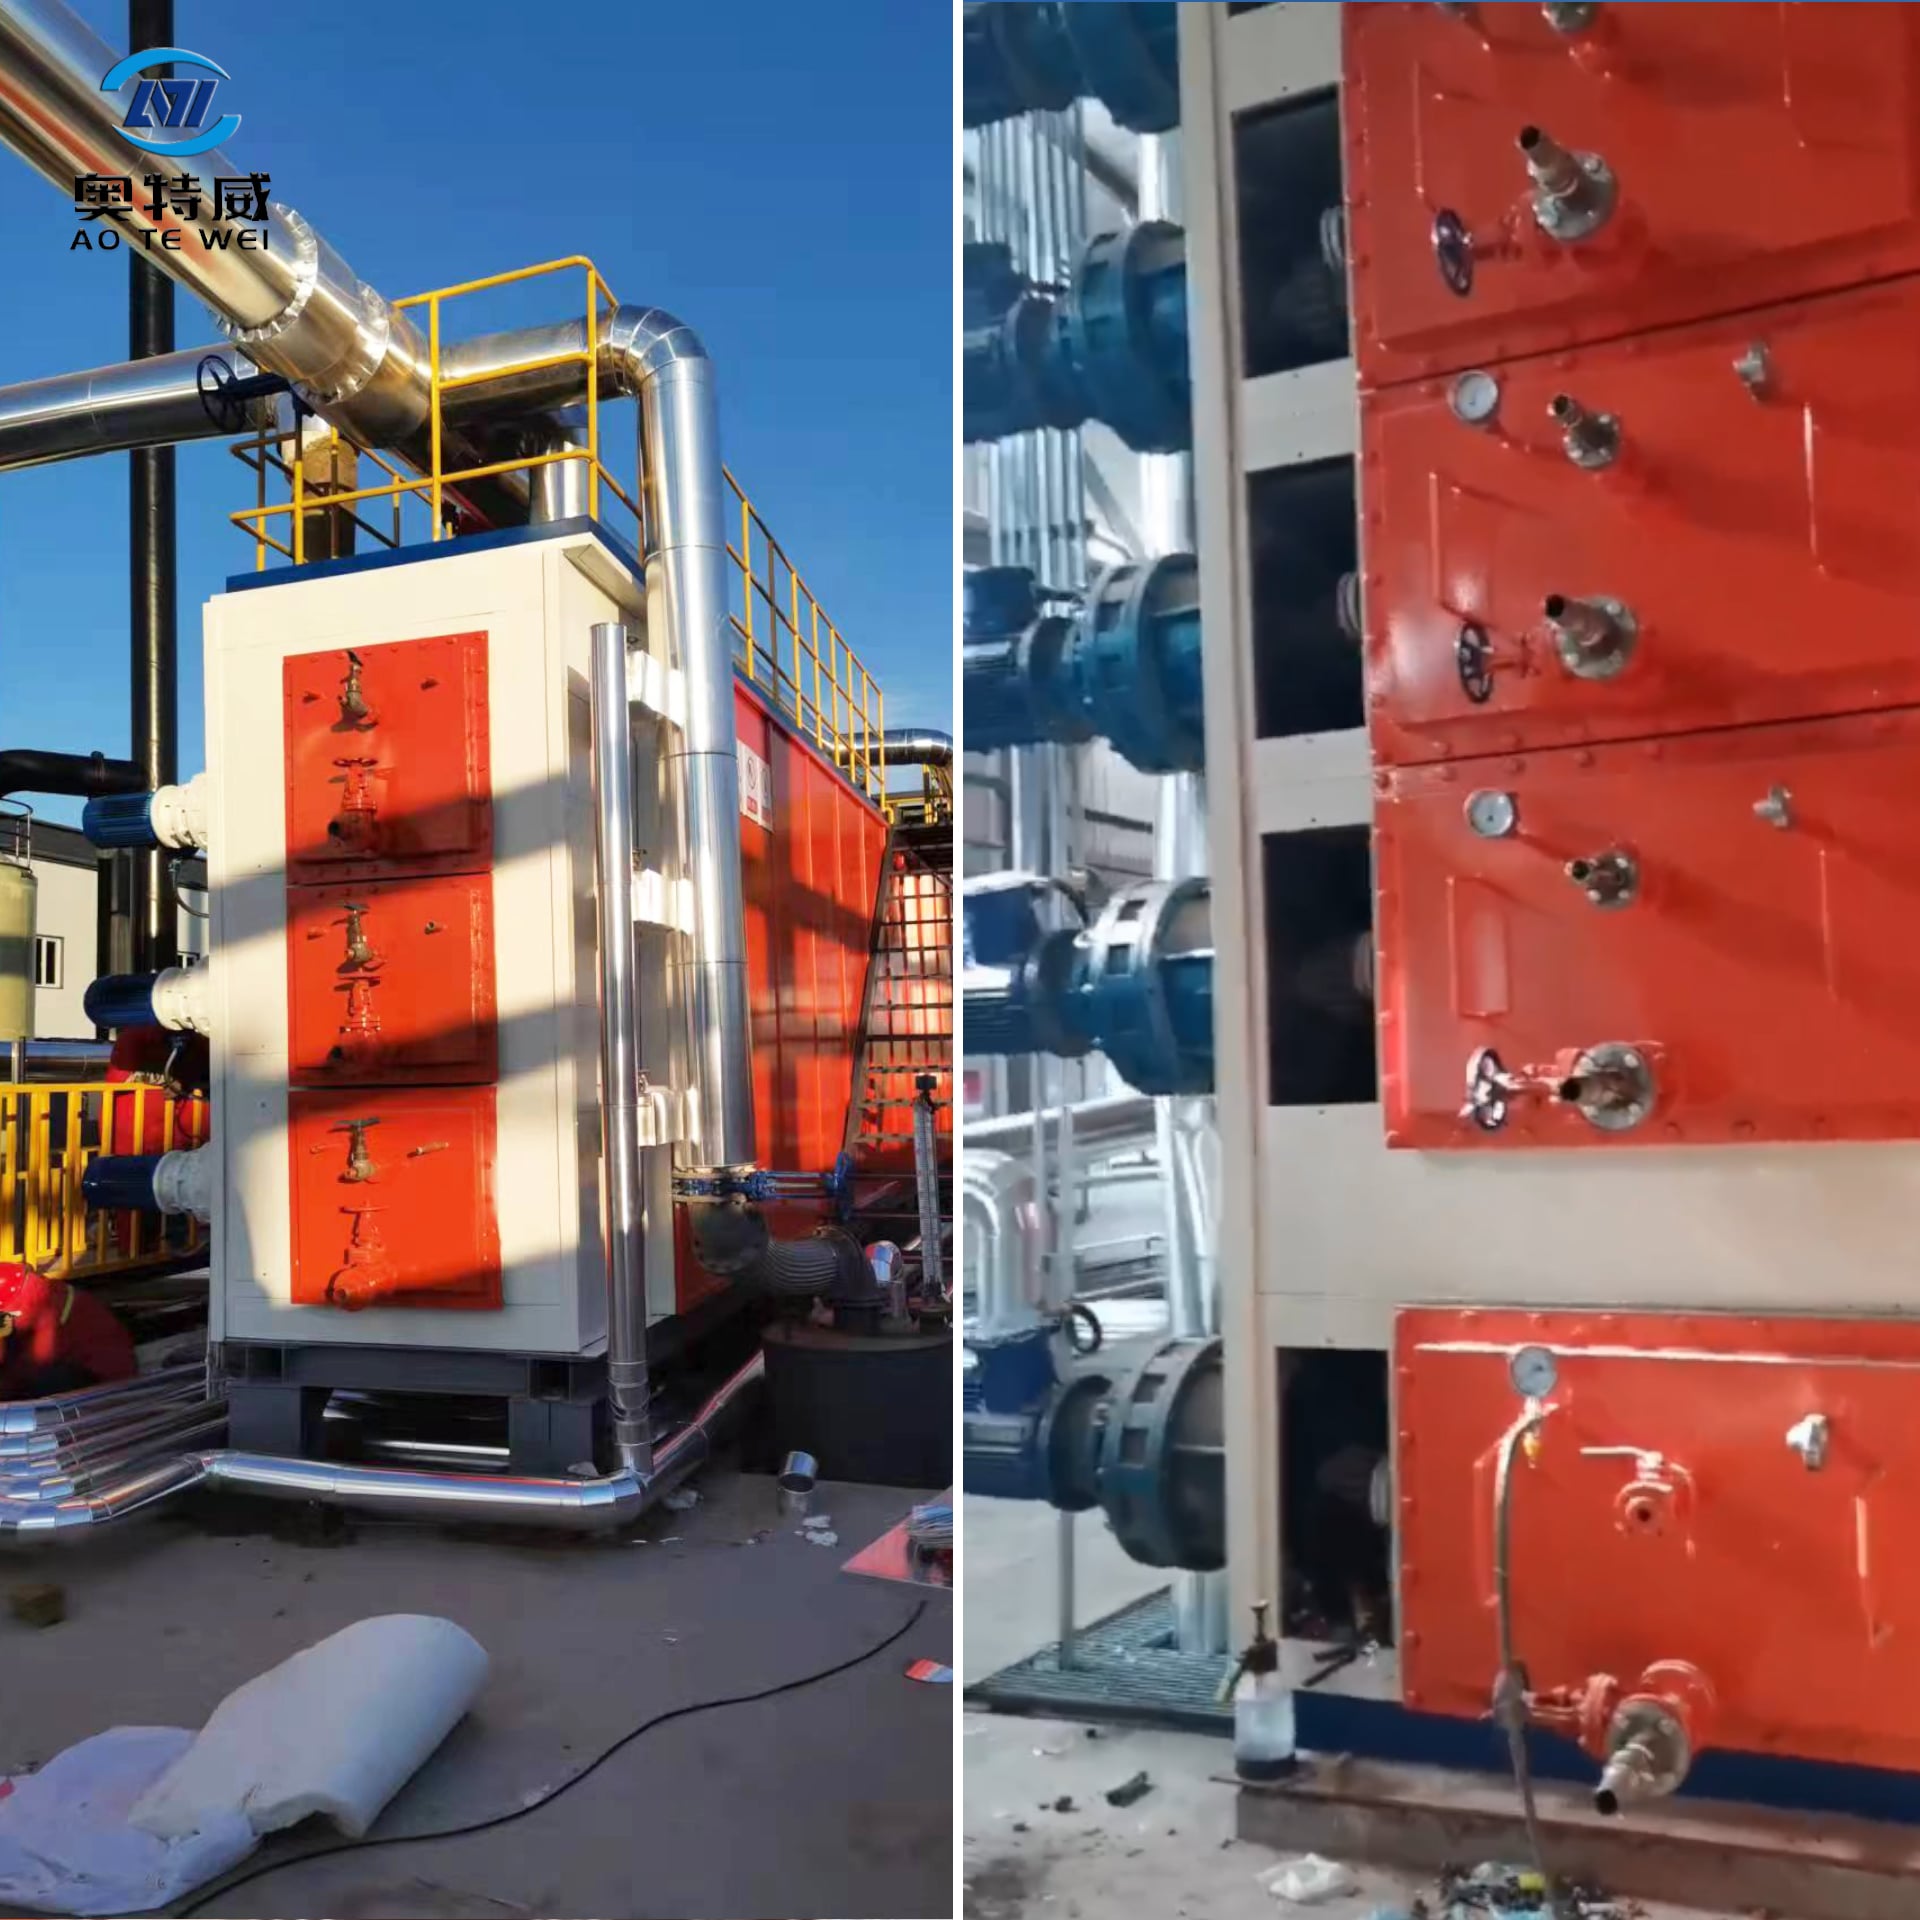
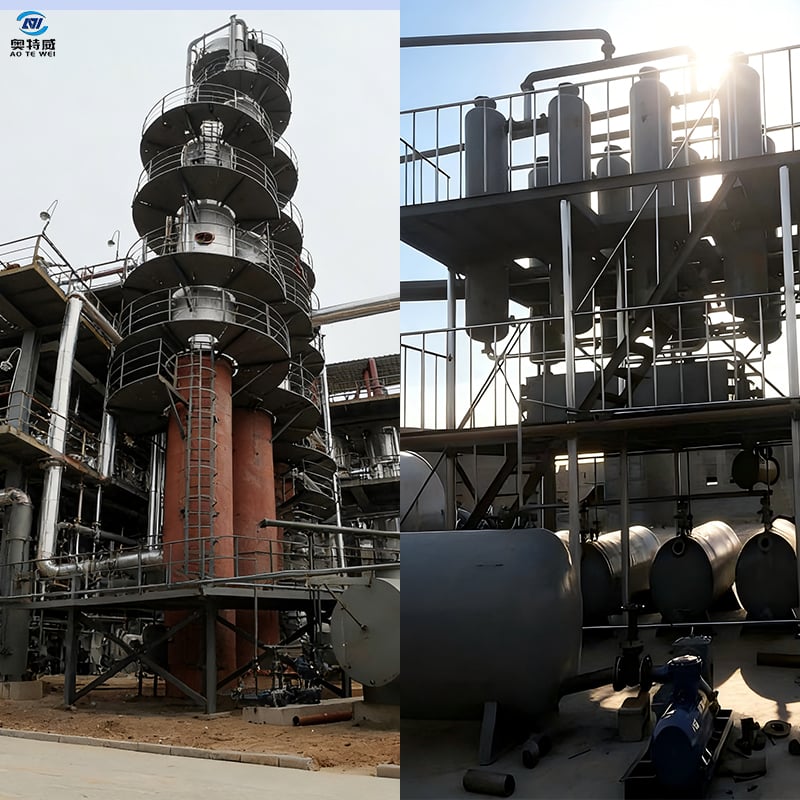
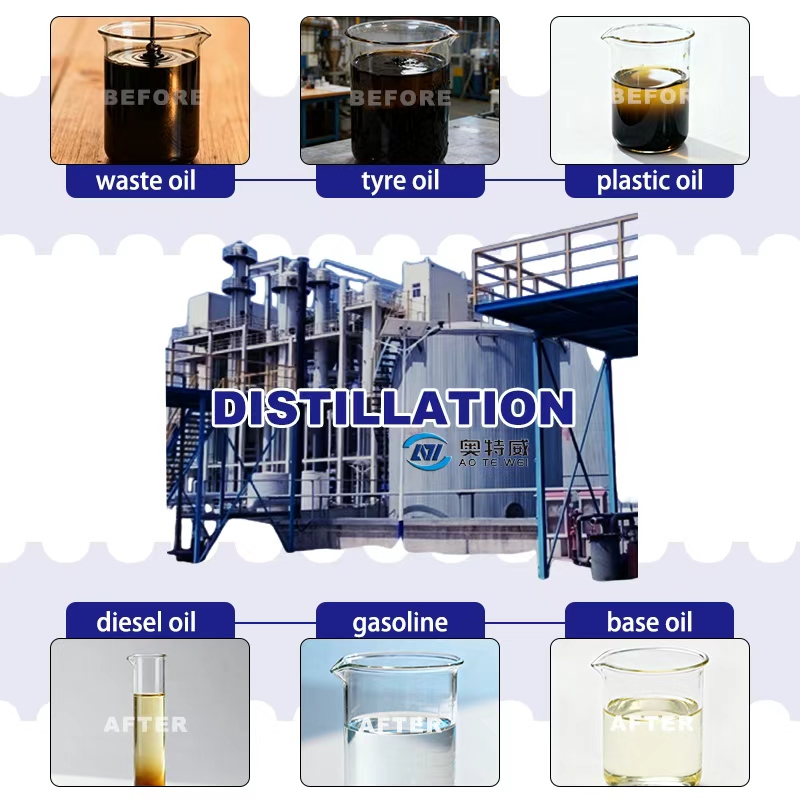
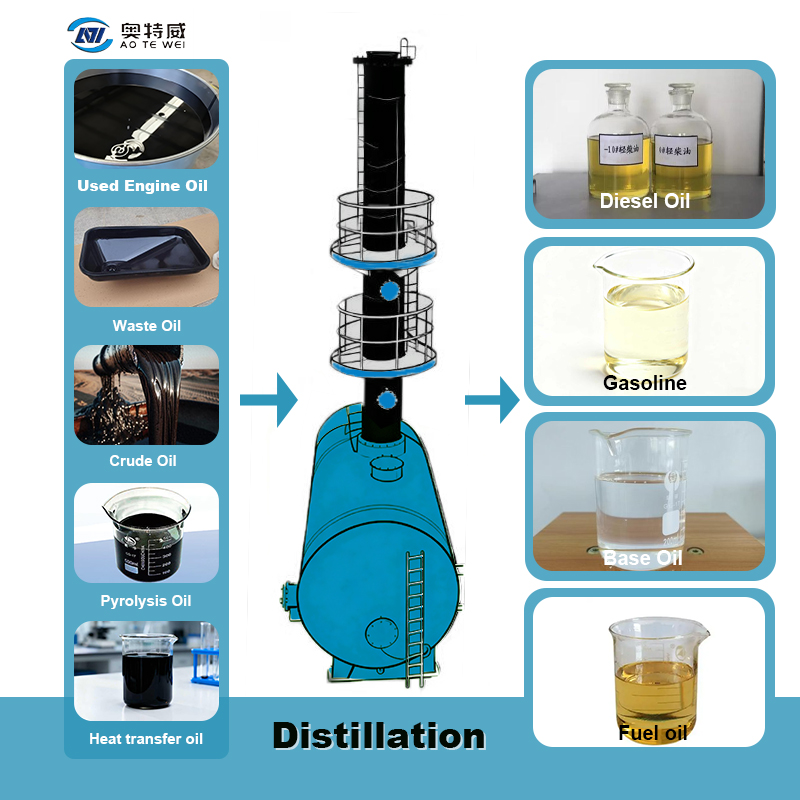
A multi column distillation plant represents an advanced industrial solution designed to separate liquid mixtures into pure components through precision distillation processes. This specialized equipment utilizes multiple distillation columns working in coordinated sequences to achieve superior separation efficiency and product purity levels that single-column systems cannot match. The multi column distillation plant operates through a sophisticated approach where different compounds are separated based on their varying boiling points across multiple stages. Each column within the system handles specific separation challenges, allowing operators to process complex mixtures that contain numerous components requiring different treatment conditions. This multi-stage configuration enables the plant to deliver higher yields and more consistent product quality. Key technological features of a multi column distillation plant include advanced temperature control systems, precision pressure regulation, and automated process monitoring. The plant incorporates state-of-the-art instrumentation that tracks chemical composition in real-time, ensuring optimal separation at each stage. Heat recovery mechanisms integrated throughout the multi column distillation plant minimize energy consumption while maximizing throughput. Applications span across petroleum refining, chemical manufacturing, pharmaceutical production, and food processing industries. The multi column distillation plant excels in separating crude oil fractions, purifying essential oils, concentrating alcoholic beverages, and processing specialty chemicals. Its versatility makes it invaluable for operations requiring multiple purification stages or handling mixtures with closely-spaced boiling points that demand exceptional separation precision and consistent quality output.
New Product Recommendations

A multi column distillation plant delivers exceptional operational efficiency that directly impacts your production costs and profitability. By processing complex mixtures in coordinated stages, this equipment reduces processing time significantly compared to traditional single-column alternatives. Your facility gains the ability to handle larger volumes while maintaining superior product purity and consistency that customers demand. The multi column distillation plant provides remarkable flexibility across diverse applications and product types. Whether you're processing crude oil fractions, chemical compounds, or specialty products, the modular design allows you to customize separation parameters for each specific need. This adaptability ensures you can expand your product range without requiring entirely new equipment investments. Energy efficiency represents another critical advantage of choosing a multi column distillation plant for your operations. Integrated heat recovery systems capture and redistribute thermal energy between columns, substantially reducing overall energy consumption. Your facility achieves lower operational costs while simultaneously improving environmental performance and meeting sustainability objectives. The multi column distillation plant incorporates advanced automation and control systems that minimize manual intervention requirements. Real-time monitoring and adjustment capabilities ensure consistent product quality with minimal operator oversight. This automation reduces human error, enhances worker safety, and allows your team to focus on strategic operations rather than routine monitoring tasks. Capital and operating efficiency combines with impressive scalability when you invest in a multi column distillation plant. The system grows with your business needs, handling increased production demands without complete equipment replacement. Superior product yields translate to better return on investment, making this technology the smart choice for forward-thinking manufacturers seeking competitive advantages and long-term profitability in increasingly demanding markets.

Latest News

How does rubber recycling improve material reuse in manufacturing industries?

01

Sep

How does rubber recycling improve material reuse in manufacturing industries?

Rubber recycling represents one of the most effective strategies for transforming industrial waste into valuable manufacturing resources. As manufacturing industries face increasing pressure to reduce environmental footprints and optimize material co...
View More
Can a pyrolysis plant support environmentally friendly recycling business models?

30

Jul

Can a pyrolysis plant support environmentally friendly recycling business models?

The global push toward circular economy principles has created significant demand for innovative recycling solutions, and the pyrolysis plant stands at the forefront of this transformation. A pyrolysis plant processes waste materials through high-tem...
View More
How does oil distillation improve purity and usability of recycled oil products?

01

Sep

How does oil distillation improve purity and usability of recycled oil products?

Oil distillation represents one of the most effective methods for restoring the quality and usability of recycled oil products in modern industrial operations. As environmental regulations tighten and resource costs rise, the ability to recycle used ...
View More
How does rubber recycling contribute to eco-friendly industrial development goals?

01

Sep

How does rubber recycling contribute to eco-friendly industrial development goals?

Rubber recycling has emerged as a critical pillar in achieving eco-friendly industrial development goals across manufacturing, construction, and transportation sectors. As global industries face mounting pressure to reduce environmental impact and ad...
View More

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

multi column distillation plant

Advanced Multi-Stage Separation Technology

Advanced Multi-Stage Separation Technology

The multi column distillation plant features cutting-edge separation technology that orchestrates multiple columns to handle complex mixture challenges with precision previously unattainable in single-stage systems. Each column specializes in specific separation tasks, working sequentially to progressively purify compounds based on their distinct boiling points. This sophisticated approach allows the multi column distillation plant to achieve exceptional purity levels even when processing mixtures containing components with similar thermal properties. The coordinated operation ensures that difficult separations become manageable, expanding the range of products your facility can profitably produce. Advanced instrumentation monitors each stage continuously, automatically adjusting parameters to maintain optimal separation conditions. This technological innovation means your facility can access premium product quality that commands higher market prices while reducing waste and improving yields significantly.
Superior Energy Efficiency and Cost Savings

Superior Energy Efficiency and Cost Savings

Operating a multi column distillation plant delivers substantial energy advantages through integrated heat recovery and thermal optimization systems. Rather than losing valuable thermal energy as waste, the equipment recycles and redistributes heat between columns, minimizing your overall energy consumption dramatically. This efficiency translates directly into reduced utility bills and lower production costs per unit. The multi column distillation plant's design eliminates redundant heating stages, ensuring thermal energy serves maximum purpose throughout the separation process. Companies implementing this technology report energy savings of thirty to fifty percent compared to conventional distillation methods. Long-term operational cost reductions make the multi column distillation plant an investment that pays dividends continuously. Lower energy consumption also enhances your environmental profile, positioning your company as a responsible manufacturer while improving bottom-line profitability.
Reliable Automation and Quality Consistency

Reliable Automation and Quality Consistency

Modern multi column distillation plants incorporate sophisticated automation systems that ensure consistent, predictable results with minimal human intervention required. Real-time analytical monitoring tracks composition and quality throughout the separation process, automatically fine-tuning parameters to maintain specifications. The multi column distillation plant delivers batch-to-batch consistency that builds customer confidence and reduces quality control challenges. Automated systems reduce operator fatigue and minimize errors associated with manual process management. Your workforce can concentrate on strategic improvements rather than routine monitoring tasks. The multi column distillation plant's intelligent control architecture learns from operational patterns, continuously optimizing performance and predicting maintenance needs before problems develop. This proactive approach reduces unexpected downtime and extends equipment lifespan significantly. Reliable automation transforms distillation from an art requiring extensive expertise into a manageable, reproducible process accessible to broader teams.

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000
Newsletter
Please Leave A Message With Us