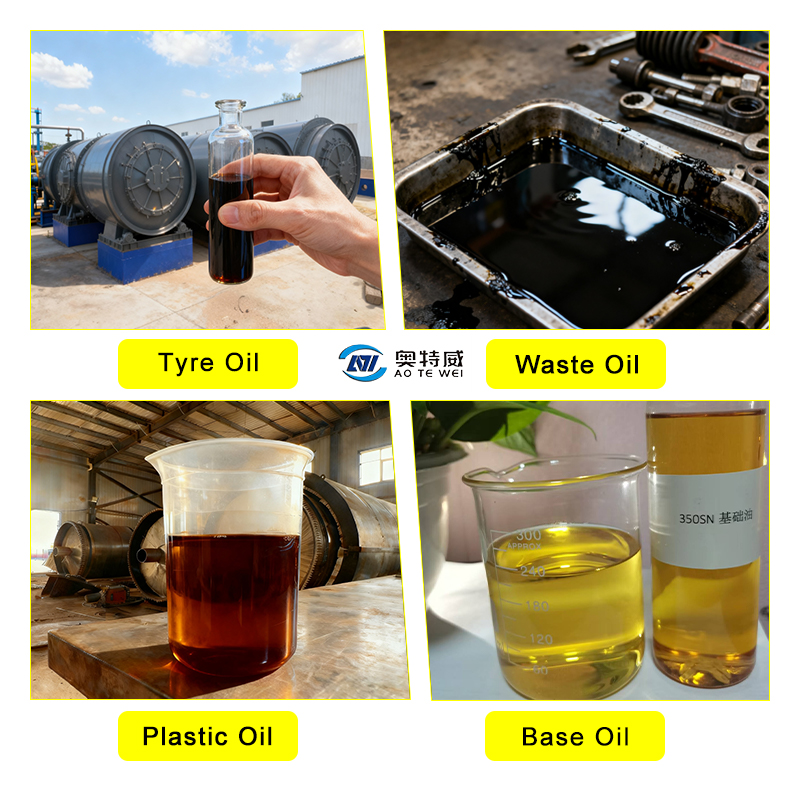
Batch Pyrolysis Reactor Systems

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

batch pyrolysis reactor

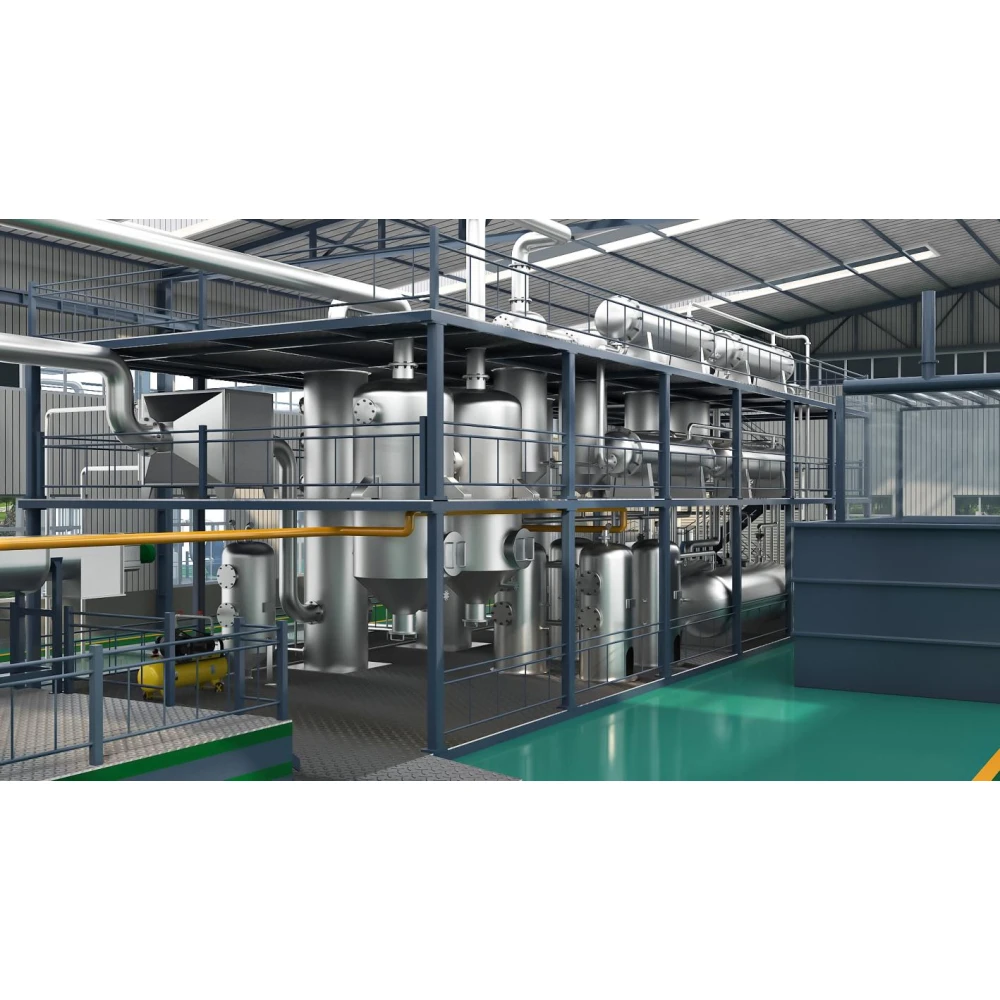
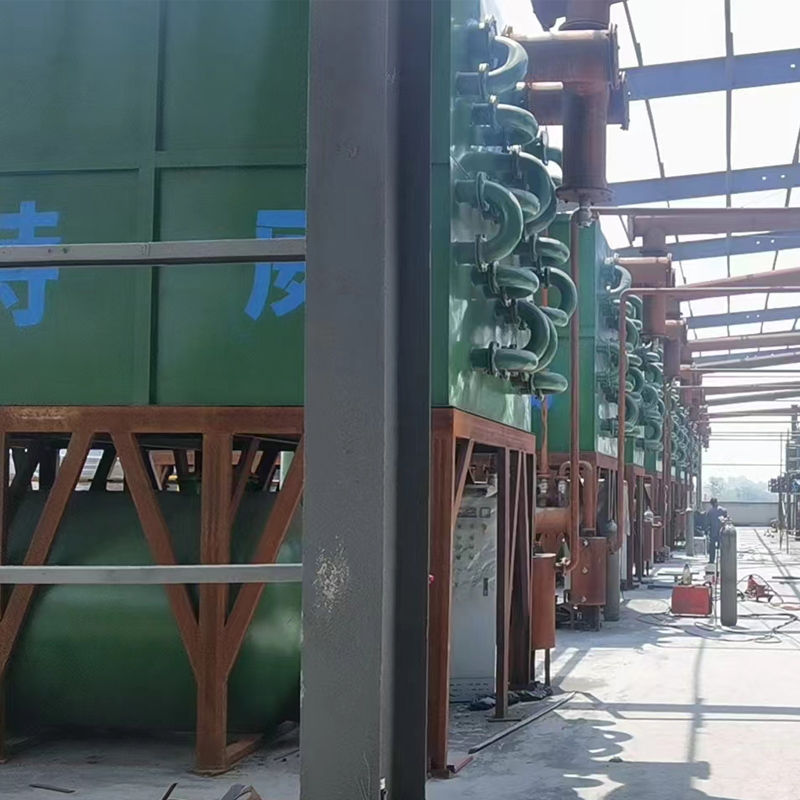
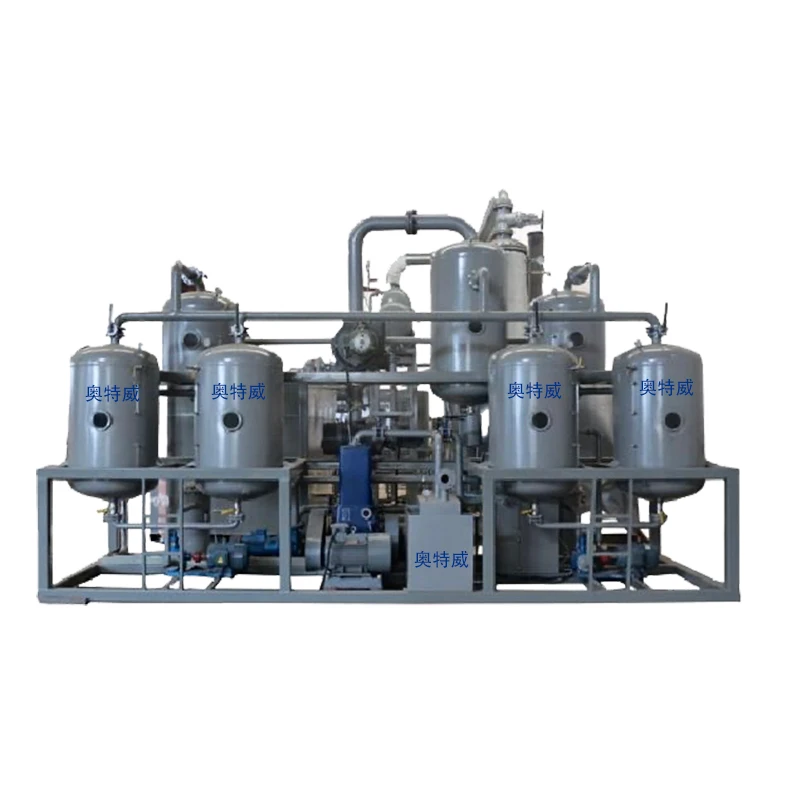
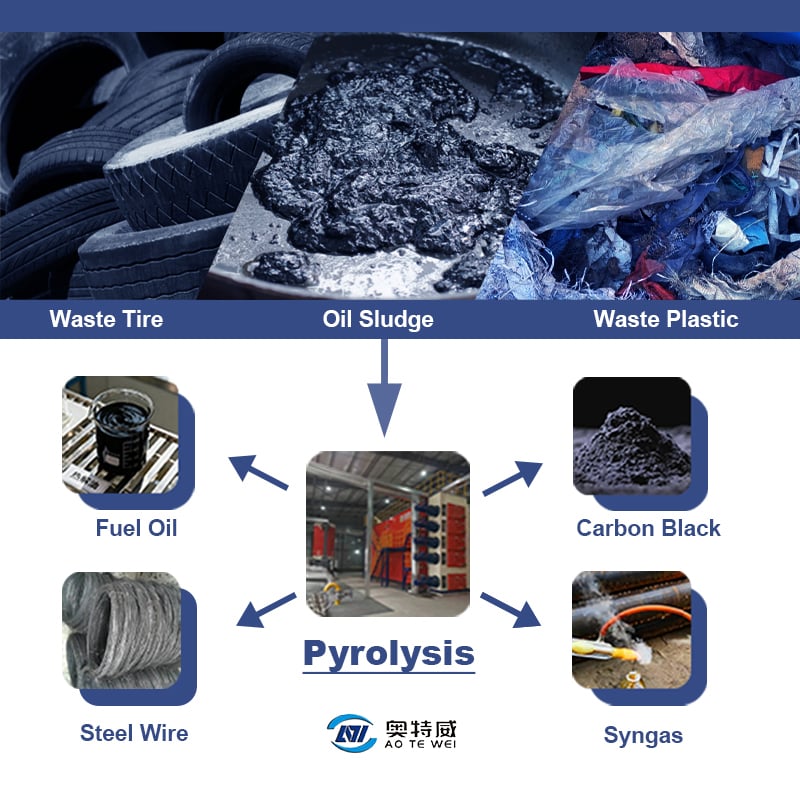
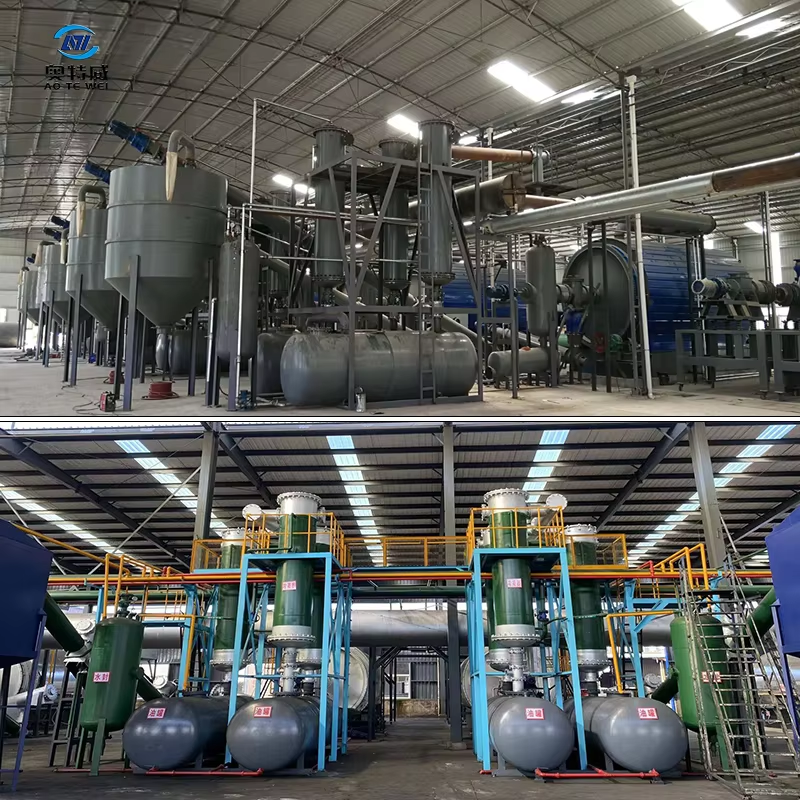
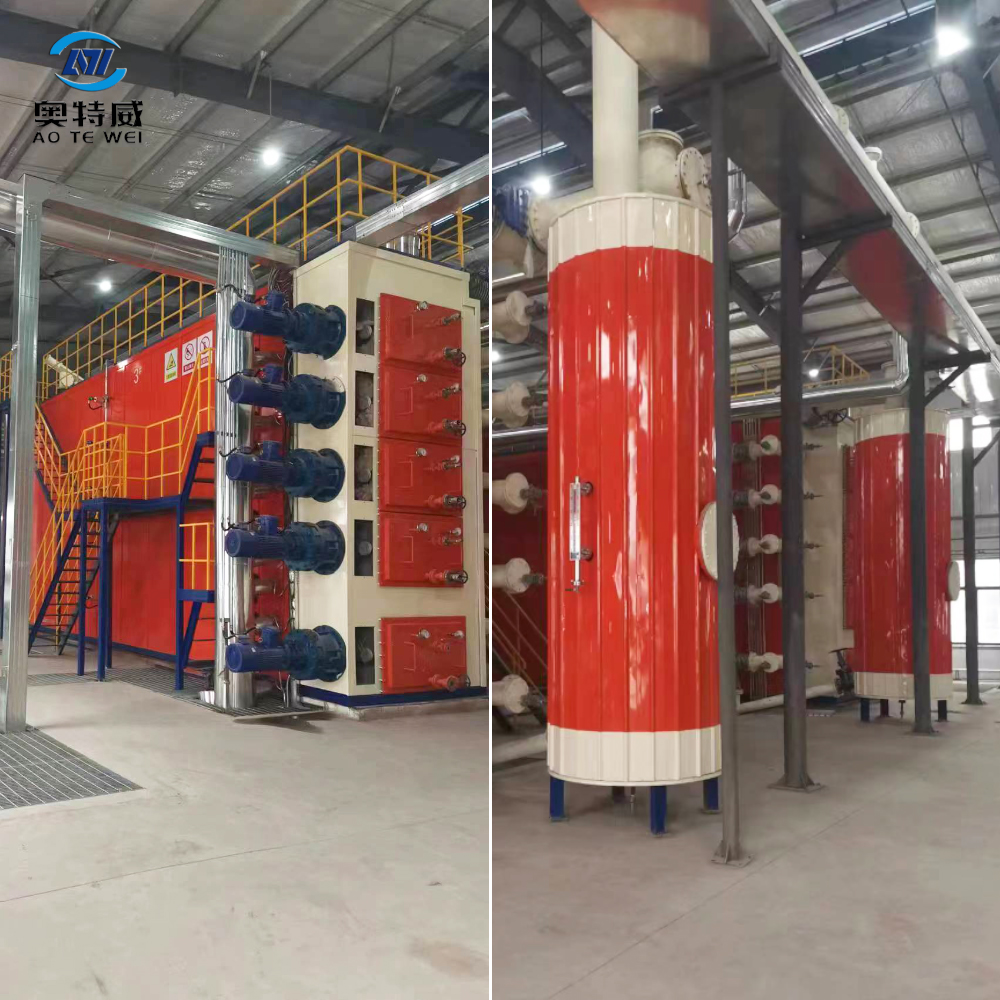
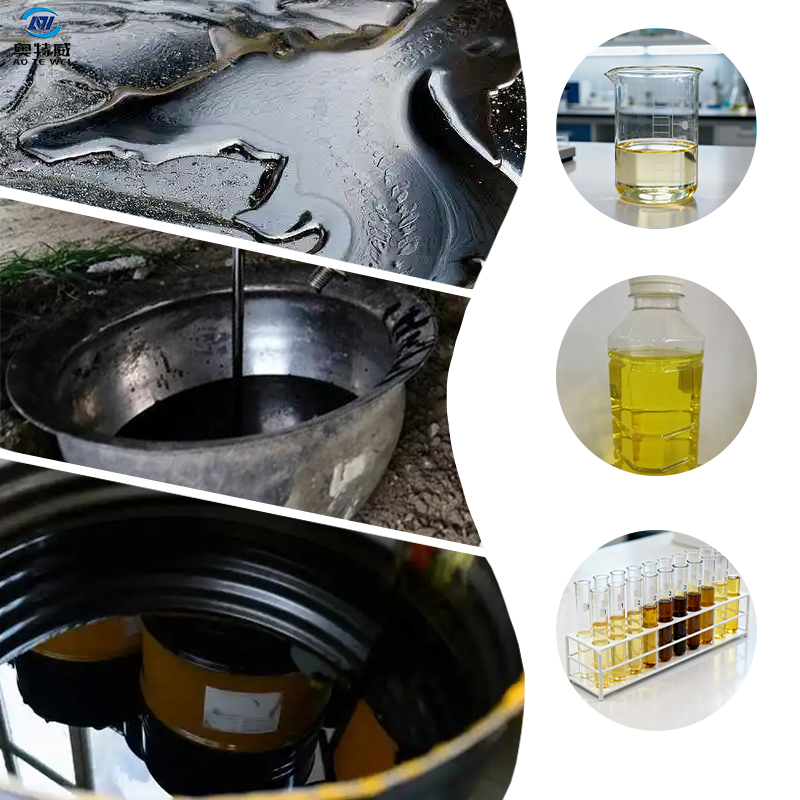
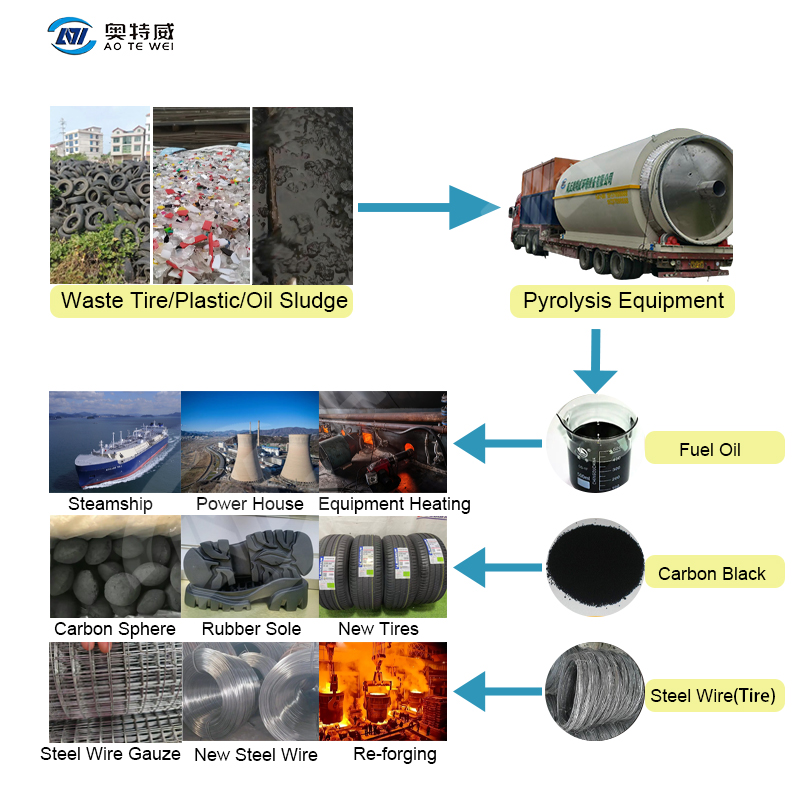
A batch pyrolysis reactor represents a specialized thermal processing system designed to decompose organic materials through controlled heating in an oxygen-free environment. This batch pyrolysis reactor operates by subjecting feedstock such as biomass, waste plastics, rubber, or other organic compounds to high temperatures, typically ranging from 400 to 800 degrees Celsius, initiating the breaking of chemical bonds without combustion. The primary function of a batch pyrolysis reactor involves converting solid waste materials into valuable products including bio-oil, biochar, and synthesis gas. The batch pyrolysis reactor achieves this transformation through a carefully controlled heating process that maximizes product yield while minimizing harmful emissions. Key technological features of a batch pyrolysis reactor include advanced temperature control systems, efficient heat transfer mechanisms, and integrated condensation units for vapor recovery. The reactor vessel, typically constructed from heat-resistant steel alloys, maintains structural integrity under extreme thermal stress. A well-designed batch pyrolysis reactor incorporates sophisticated monitoring equipment to track pressure, temperature, and gas composition throughout the pyrolysis cycle. Applications for a batch pyrolysis reactor span multiple industries. Environmental companies utilize this batch pyrolysis reactor for waste management and resource recovery. Agricultural operations employ it for biomass conversion, while manufacturing facilities use it for producing alternative fuels and chemical feedstocks. The batch pyrolysis reactor also supports circular economy initiatives by converting end-of-life materials into commercially viable products, making it an environmentally responsible solution for sustainable resource management and industrial waste reduction.
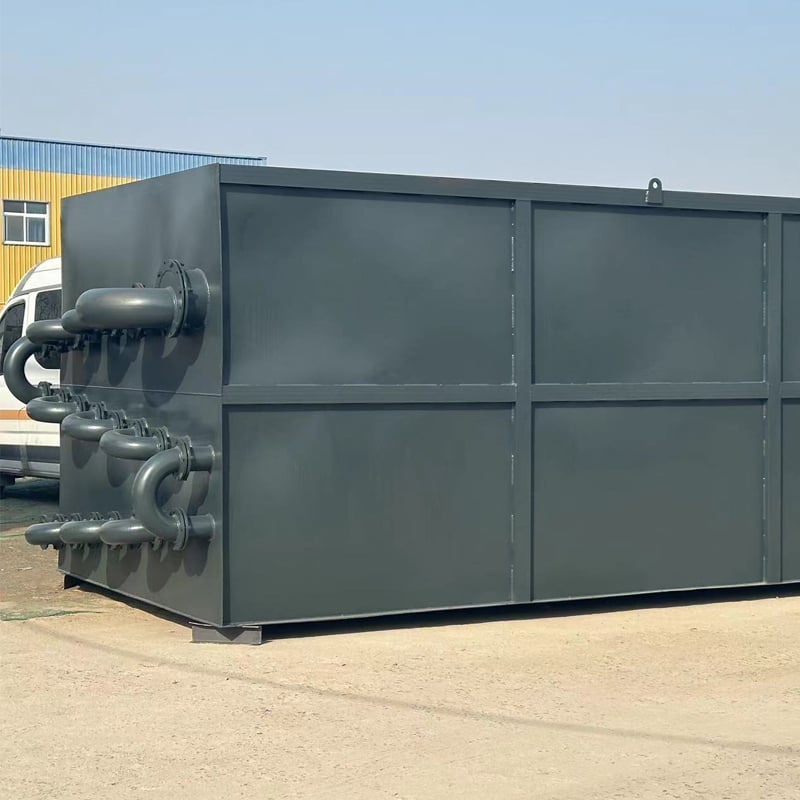
New Product Releases

A batch pyrolysis reactor delivers exceptional value to operators seeking efficient waste processing and resource recovery solutions. Operating a batch pyrolysis reactor provides immediate environmental benefits by safely treating hazardous and challenging waste streams that would otherwise occupy landfills or require expensive disposal methods. Practical operational benefits of a batch pyrolysis reactor include its versatility in processing diverse feedstock types without requiring extensive material pre-treatment. Users can operate a batch pyrolysis reactor with minimal operational complexity, making it accessible to businesses of varying sizes and technical expertise levels. The batch pyrolysis reactor enables operators to achieve consistent product quality through precise temperature and duration controls, ensuring reliable results across successive production cycles. From an economic perspective, investing in a batch pyrolysis reactor generates revenue streams through valuable product creation. The recovered bio-oil serves industrial applications, biochar finds markets in agriculture and environmental remediation, while synthesis gas can fuel on-site operations or be sold externally. A batch pyrolysis reactor effectively transforms waste management from a cost center into a profit-generating operation. Application suitability makes a batch pyrolysis reactor ideal for facilities processing municipal waste, agricultural residues, manufacturing scrap, or contaminated materials. The batch pyrolysis reactor accommodates fluctuating input volumes without performance degradation, providing operational flexibility for dynamic business environments. Decision-useful product context shows that a batch pyrolysis reactor represents a strategic investment in sustainable operations. Companies operating a batch pyrolysis reactor enhance their environmental credentials while improving profitability. The reduced carbon footprint and lower emissions profile align with increasingly stringent environmental regulations, positioning organizations as responsible industrial citizens while maintaining competitive advantages through resource efficiency.

Latest News

Why are manufacturers investing in plastic pyrolysis technology for sustainability?

30

Jul

Why are manufacturers investing in plastic pyrolysis technology for sustainability?

Across the global manufacturing sector, plastic pyrolysis has rapidly moved from a niche concept to a strategic priority. As regulatory pressure on plastic waste intensifies and corporate sustainability commitments become binding targets, manufacture...
View More
Can a pyrolysis plant support environmentally friendly recycling business models?

30

Jul

Can a pyrolysis plant support environmentally friendly recycling business models?

The global push toward circular economy principles has created significant demand for innovative recycling solutions, and the pyrolysis plant stands at the forefront of this transformation. A pyrolysis plant processes waste materials through high-tem...
View More
How does rubber recycling improve material reuse in manufacturing industries?

01

Sep

How does rubber recycling improve material reuse in manufacturing industries?

Rubber recycling represents one of the most effective strategies for transforming industrial waste into valuable manufacturing resources. As manufacturing industries face increasing pressure to reduce environmental footprints and optimize material co...
View More
Why do governments encourage tire recycling projects in waste management programs?

03

Sep

Why do governments encourage tire recycling projects in waste management programs?

Tire recycling has become a cornerstone of modern waste management strategies worldwide. Governments across the globe actively encourage tire recycling projects because they address critical environmental, economic, and public health challenges. The ...
View More

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

batch pyrolysis reactor

Advanced Temperature Control and Precision Heating

Advanced Temperature Control and Precision Heating

A batch pyrolysis reactor incorporates sophisticated temperature regulation systems that maintain optimal pyrolysis conditions throughout the entire processing cycle. This batch pyrolysis reactor features real-time temperature monitoring with automated adjustment capabilities, ensuring consistent heating profiles that maximize product yields. The precise control mechanism within a batch pyrolysis reactor prevents temperature fluctuations that could compromise product quality or create safety hazards. Advanced insulation materials protect operators while optimizing thermal efficiency, reducing energy consumption and operational costs. The batch pyrolysis reactor's heating system can accommodate various material types and processing requirements, providing adaptability across multiple applications. Users appreciate how a batch pyrolysis reactor's temperature precision delivers reliable, repeatable results, minimizing production variability and supporting quality assurance objectives. This technological advantage transforms a batch pyrolysis reactor into an indispensable asset for operations demanding stringent product specifications.
Comprehensive Vapor Recovery and Condensation Systems

Comprehensive Vapor Recovery and Condensation Systems

Every batch pyrolysis reactor features integrated condensation technology that captures valuable vapors released during thermal decomposition. This batch pyrolysis reactor's vapor recovery system prevents environmental emissions while preserving product value that would otherwise dissipate into the atmosphere. The condensation unit within a batch pyrolysis reactor efficiently cools and collects pyrolysis vapors, converting them into liquid bio-oil suitable for fuel applications or chemical manufacturing. Advanced filtration components in a batch pyrolysis reactor remove particulates and contaminants, producing high-purity products that command premium market prices. The batch pyrolysis reactor's comprehensive recovery approach maximizes material utilization, converting up to ninety percent of feedstock into usable products. Operators benefit from a batch pyrolysis reactor's environmental performance, which significantly reduces atmospheric pollution and supports regulatory compliance. This recovery capability distinguishes a batch pyrolysis reactor as a complete waste-to-value solution rather than a simple thermal processor.
Flexible Feedstock Processing and Operational Adaptability

Flexible Feedstock Processing and Operational Adaptability

A batch pyrolysis reactor excels at processing diverse material streams without requiring extensive preprocessing or equipment modifications. This batch pyrolysis reactor accepts heterogeneous feedstock including mixed plastics, agricultural waste, rubber byproducts, and contaminated materials that traditional recycling methods cannot handle. The batch pyrolysis reactor's design accommodates varying material sizes and compositions through adjustable parameters and processing cycles. Operators can modify residence time, temperature profiles, and heating rates within a batch pyrolysis reactor to optimize results for specific applications. This adaptability ensures a batch pyrolysis reactor remains economically viable even when feedstock availability or composition changes seasonally or market-driven. The batch pyrolysis reactor's operational flexibility supports businesses managing unpredictable waste streams or pursuing multiple product outputs simultaneously. This advantage positions a batch pyrolysis reactor as a resilient investment that continues generating returns across varying business conditions and market circumstances.

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000
Newsletter
Please Leave A Message With Us