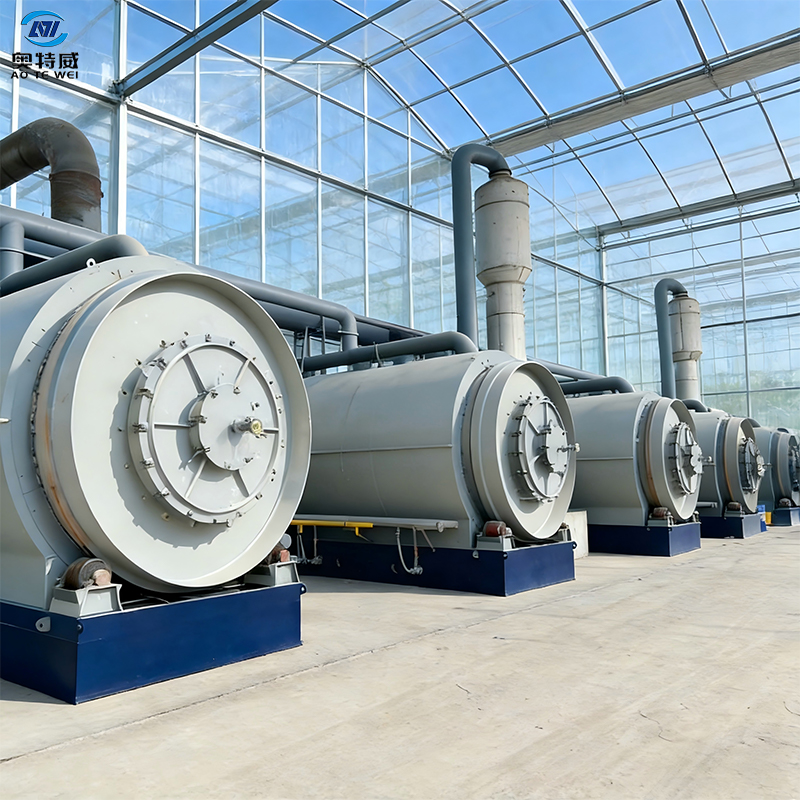
High-Temperature Pyrolysis Technology

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

hightemperature pyrolysis technology

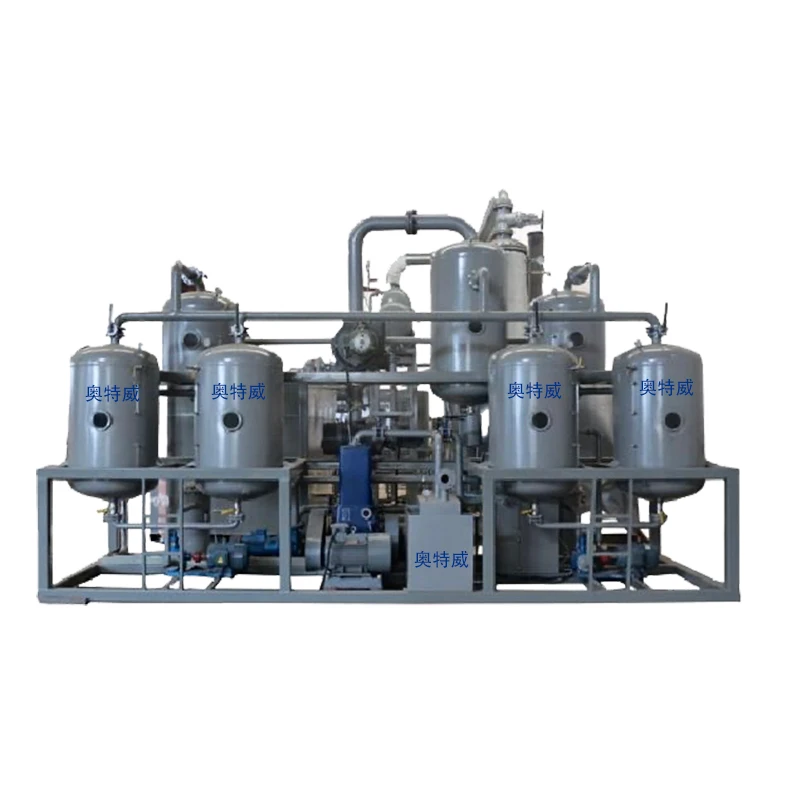
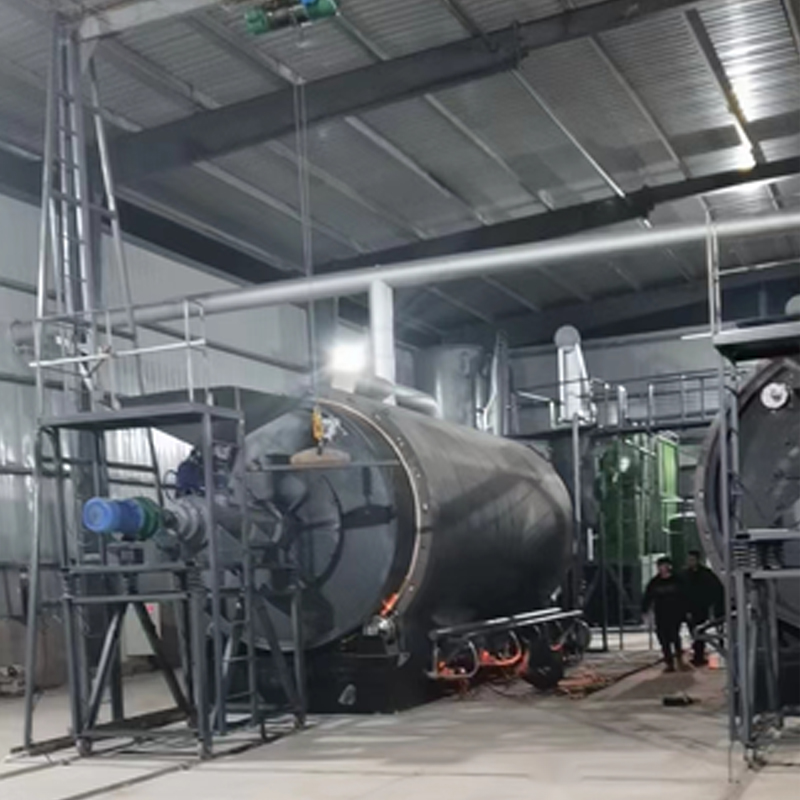
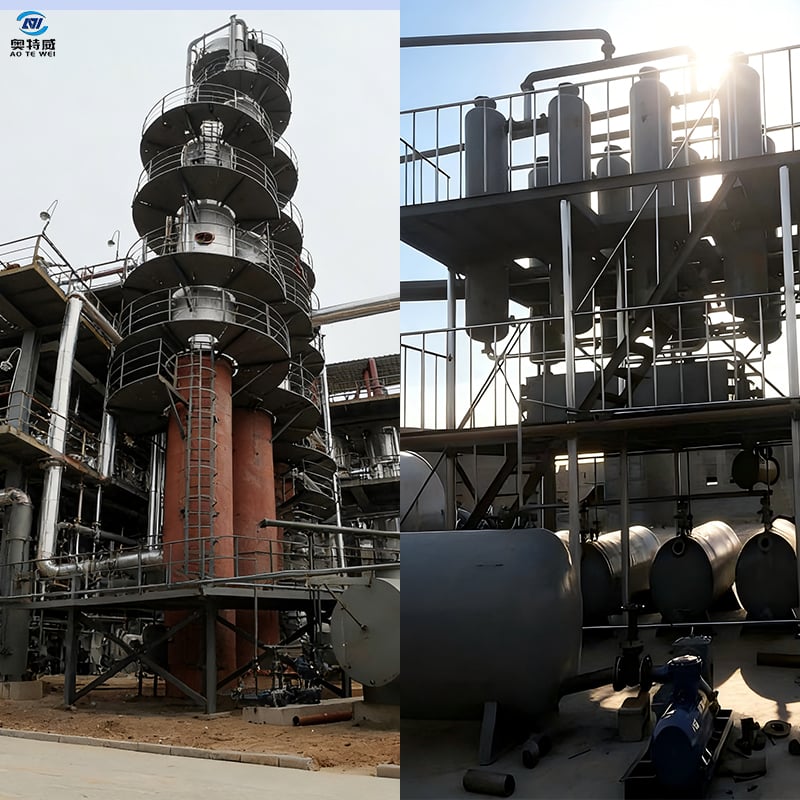
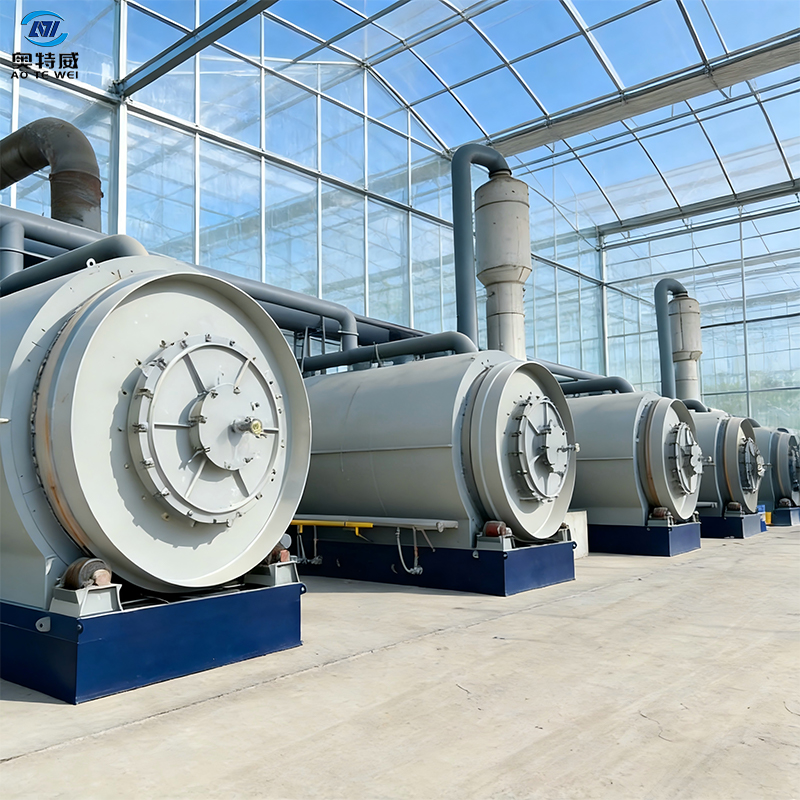
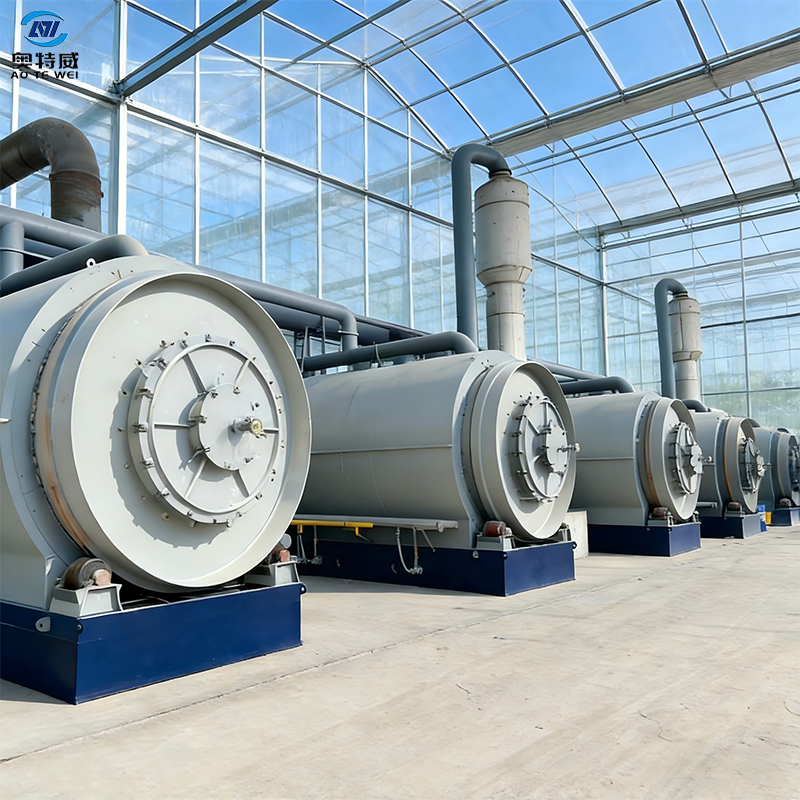
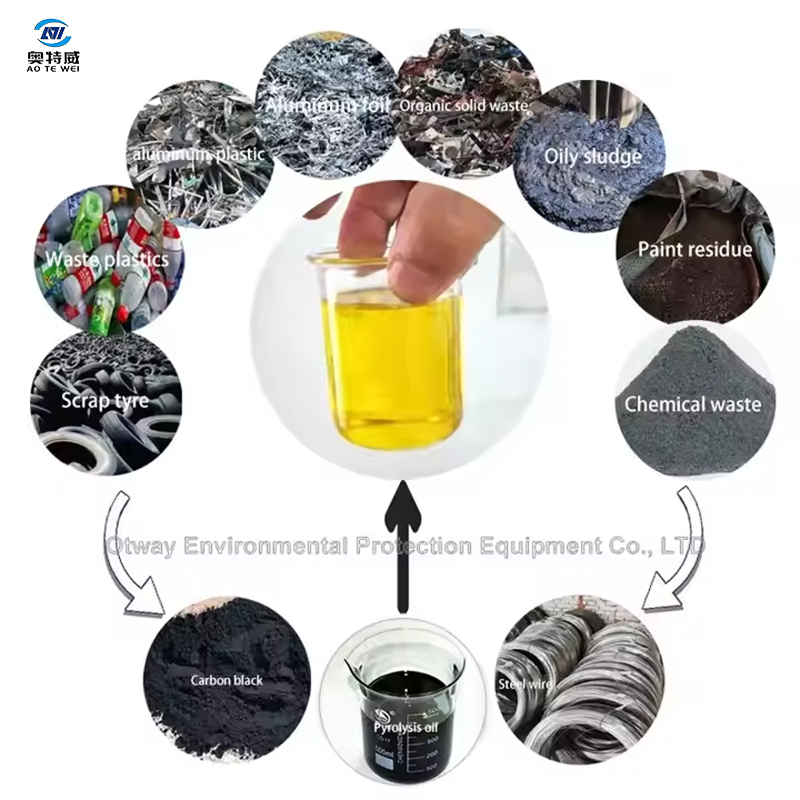
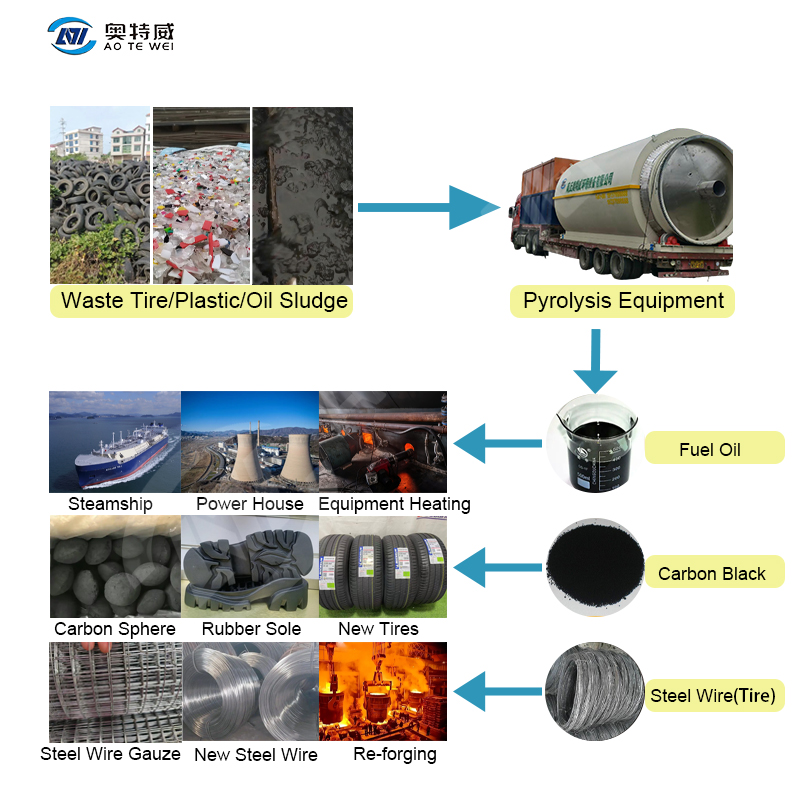
High-temperature pyrolysis technology represents a transformative waste management and resource recovery solution that converts organic materials into valuable products through controlled thermal decomposition. This advanced process operates at elevated temperatures, typically ranging from 400 to 800 degrees Celsius, in an oxygen-free environment to break down complex molecular structures into simpler, more useful compounds. The main functions of high-temperature pyrolysis technology include converting waste materials such as plastics, biomass, rubber, and municipal solid waste into bio-oil, biochar, and syngas. These outputs serve as alternative fuels, soil amendments, and chemical feedstocks for various industrial applications. High-temperature pyrolysis technology achieves this through precise temperature control and specialized reactor design. Key technological features distinguish this approach from conventional thermal processing methods. The high-temperature pyrolysis technology employs anaerobic conditions to prevent combustion, enabling selective breakdown of organic compounds. Advanced heat management systems maintain optimal temperature profiles, while sophisticated gas collection mechanisms capture valuable gaseous products. The process includes condensation systems that recover liquid bio-oil efficiently. Applications of high-temperature pyrolysis technology span multiple industries. Environmental remediation facilities use it for plastic waste conversion, reducing landfill dependency. Energy companies leverage the technology to produce alternative fuels from biomass. Agricultural sectors benefit from biochar production for soil enhancement. Chemical manufacturers utilize syngas outputs for further processing. The versatility of high-temperature pyrolysis technology makes it increasingly essential for circular economy initiatives and sustainable resource management across diverse sectors.
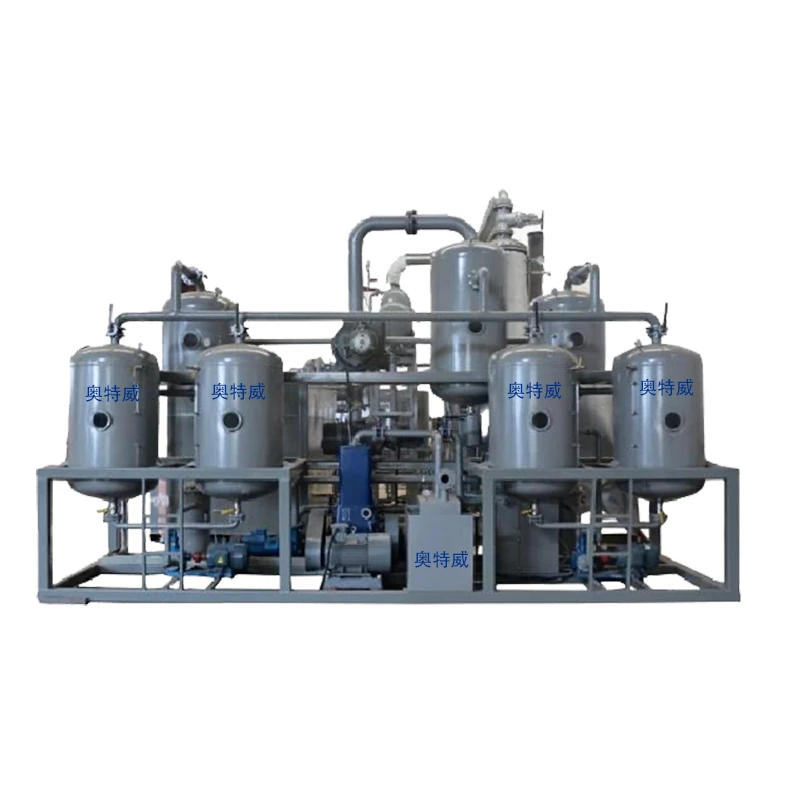
New Product Recommendations

High-temperature pyrolysis technology delivers exceptional practical benefits that address critical environmental and economic challenges facing modern industries. This innovative process provides straightforward operational advantages that enhance business performance while contributing to sustainability goals. The primary buyer value stems from waste conversion into profitable products. Organizations implementing high-temperature pyrolysis technology transform disposal costs into revenue streams by producing marketable bio-oil, biochar, and syngas. This economic advantage directly improves bottom-line profitability while simultaneously addressing waste management challenges. Operational benefits are substantial and measurable. High-temperature pyrolysis technology operates with minimal environmental emissions compared to incineration or landfilling, significantly reducing regulatory compliance burdens. The process requires relatively compact facility footprints, making it suitable for diverse geographic locations. Operational flexibility allows processing of various feedstock types without major equipment modifications, reducing capital expenses for multi-waste scenarios. Application suitability extends across multiple industries without requiring specialized expertise. Plastic recycling operations deploy high-temperature pyrolysis technology to handle contaminated or mixed plastic streams previously deemed non-recyclable. Tire management facilities process end-of-life tires efficiently. Agricultural enterprises convert crop residues into valuable soil amendments through biochar production. Product context enhances decision-making for potential customers. High-temperature pyrolysis technology represents proven technology with established performance records across thousands of installations globally. The generated products meet quality standards for fuel applications, with bio-oil specifications comparable to conventional petroleum derivatives. Biochar outputs satisfy rigorous agricultural and environmental standards, ensuring market acceptance. Decision-useful advantages include scalability from small pilot systems to large industrial installations. Long equipment lifespan provides excellent return on investment. Technical support networks ensure reliable operations. These factors collectively position high-temperature pyrolysis technology as a strategic solution for forward-thinking organizations committed to sustainable profitability.

Practical Tips

Why do recycling plants rely on pyrolysis reactor technology for energy recovery?

01

Sep

Why do recycling plants rely on pyrolysis reactor technology for energy recovery?

Modern recycling plants face mounting pressure to recover maximum value from waste streams while maintaining environmental compliance. The pyrolysis reactor has emerged as a critical technology for achieving this balance, transforming discarded mater...
View More
How does rubber recycling contribute to eco-friendly industrial development goals?

01

Sep

How does rubber recycling contribute to eco-friendly industrial development goals?

Rubber recycling has emerged as a critical pillar in achieving eco-friendly industrial development goals across manufacturing, construction, and transportation sectors. As global industries face mounting pressure to reduce environmental impact and ad...
View More
Why do recycling plants rely on pyrolysis reactor technology for energy recovery?

01

Sep

Why do recycling plants rely on pyrolysis reactor technology for energy recovery?

Modern recycling plants face mounting pressure to recover maximum value from waste streams while maintaining environmental compliance. The pyrolysis reactor has emerged as a critical technology for achieving this balance, transforming discarded mater...
View More
How does plastic pyrolysis improve value recovery from mixed plastic waste streams?

03

Sep

How does plastic pyrolysis improve value recovery from mixed plastic waste streams?

Mixed plastic waste streams present a significant challenge for waste management industries worldwide. Traditional recycling methods struggle to handle contaminated, multi-polymer, or degraded plastics that cannot be mechanically reprocessed into vir...
View More

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

hightemperature pyrolysis technology

Superior Product Recovery and Market Value

Superior Product Recovery and Market Value

High-temperature pyrolysis technology maximizes material recovery through advanced thermal processing that converts waste into three distinct valuable products. The process generates premium-quality bio-oil suitable for heating applications and fuel production, biochar applicable for soil improvement and carbon sequestration, and syngas usable for energy generation or chemical synthesis. This multi-product output approach ensures comprehensive resource utilization, meaning virtually no processing residue becomes waste. Organizations implementing high-temperature pyrolysis technology achieve exceptional product recovery rates exceeding ninety percent, significantly outperforming traditional disposal methods. The economic advantage proves compelling: each ton of input material yields multiple saleable products, creating diverse revenue streams. Bio-oil commands prices comparable to conventional fuels, biochar attracts premium pricing in agricultural markets, and syngas powers onsite equipment or sells to energy consumers. This product diversification through high-temperature pyrolysis technology reduces market dependency risks while maximizing financial returns from waste streams previously considered liabilities.
Environmental Compliance and Emission Reduction

Environmental Compliance and Emission Reduction

High-temperature pyrolysis technology operates as an environmentally responsible alternative to conventional waste processing methods, delivering measurable emissions reductions and regulatory compliance advantages. The oxygen-free processing environment prevents toxic combustion byproducts, eliminating dioxin formation and significantly reducing harmful air pollutants. High-temperature pyrolysis technology achieves ninety-five percent or greater reduction in greenhouse gas emissions compared to landfilling equivalent waste quantities. The closed-loop system captures and utilizes all gaseous outputs, preventing atmospheric release of volatile organic compounds. Advanced filtration and scrubbing systems in modern high-temperature pyrolysis technology installations ensure stack emissions meet or exceed the strictest international environmental standards. Particulate matter collection efficiency exceeds ninety-nine percent, protecting air quality in surrounding communities. Organizations adopting high-temperature pyrolysis technology demonstrate genuine environmental stewardship while maintaining full regulatory compliance without expensive additional control equipment. This alignment with environmental objectives strengthens corporate sustainability credentials and appeals to environmentally conscious investors and customers.
Scalable Infrastructure and Operational Flexibility

Scalable Infrastructure and Operational Flexibility

High-temperature pyrolysis technology provides remarkable flexibility through modular system designs accommodating diverse operational scales and feedstock requirements. Small-capacity systems suit localized waste management needs at towns and industrial facilities, while larger installations serve regional processing demands across multiple material sources. This scalability through high-temperature pyrolysis technology eliminates oversizing risks and unnecessary capital expenditure for organizations with evolving waste volumes. The technology adapts to process numerous feedstock types including mixed plastics, textile waste, rubber materials, and biomass residues with minimal operational adjustments. High-temperature pyrolysis technology systems require substantially smaller footprints compared to conventional processing facilities, enabling installation in space-constrained locations. Automated control systems optimize processing parameters for specific feedstock characteristics, ensuring consistent product quality regardless of input material variations. This operational flexibility through high-temperature pyrolysis technology significantly reduces training requirements and technical expertise needed for reliable system operation. Maintenance intervals remain extended due to robust equipment design, minimizing downtime and operational interruptions. The inherent adaptability of high-temperature pyrolysis technology enables organizations to respond rapidly to emerging waste streams and evolving market opportunities without major facility retrofitting.

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000
Newsletter
Please Leave A Message With Us