Rubber Recycling Equipment | Advanced Processing

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

rubber recycling equipment

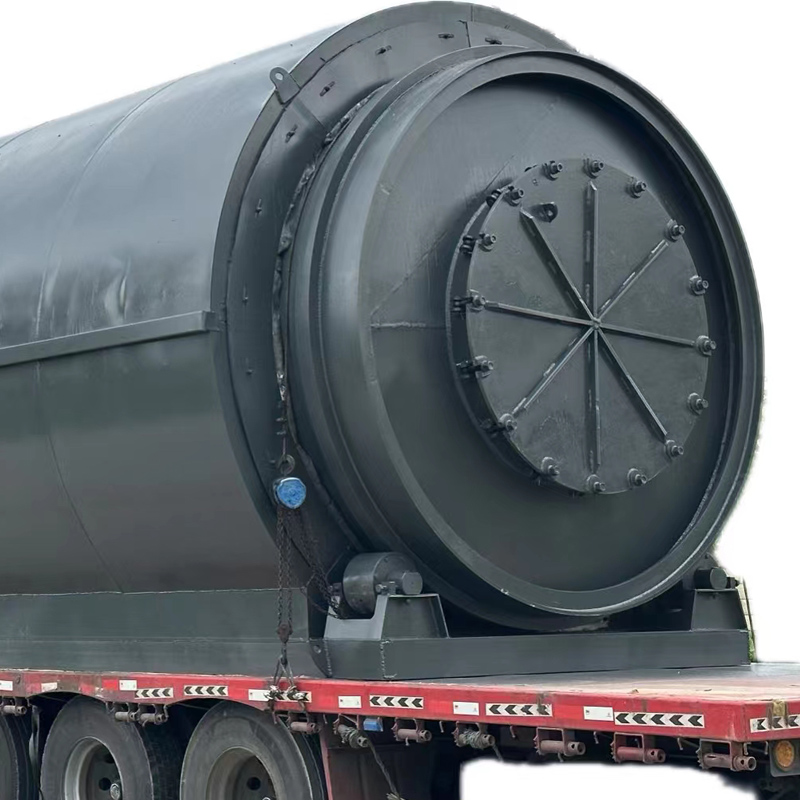
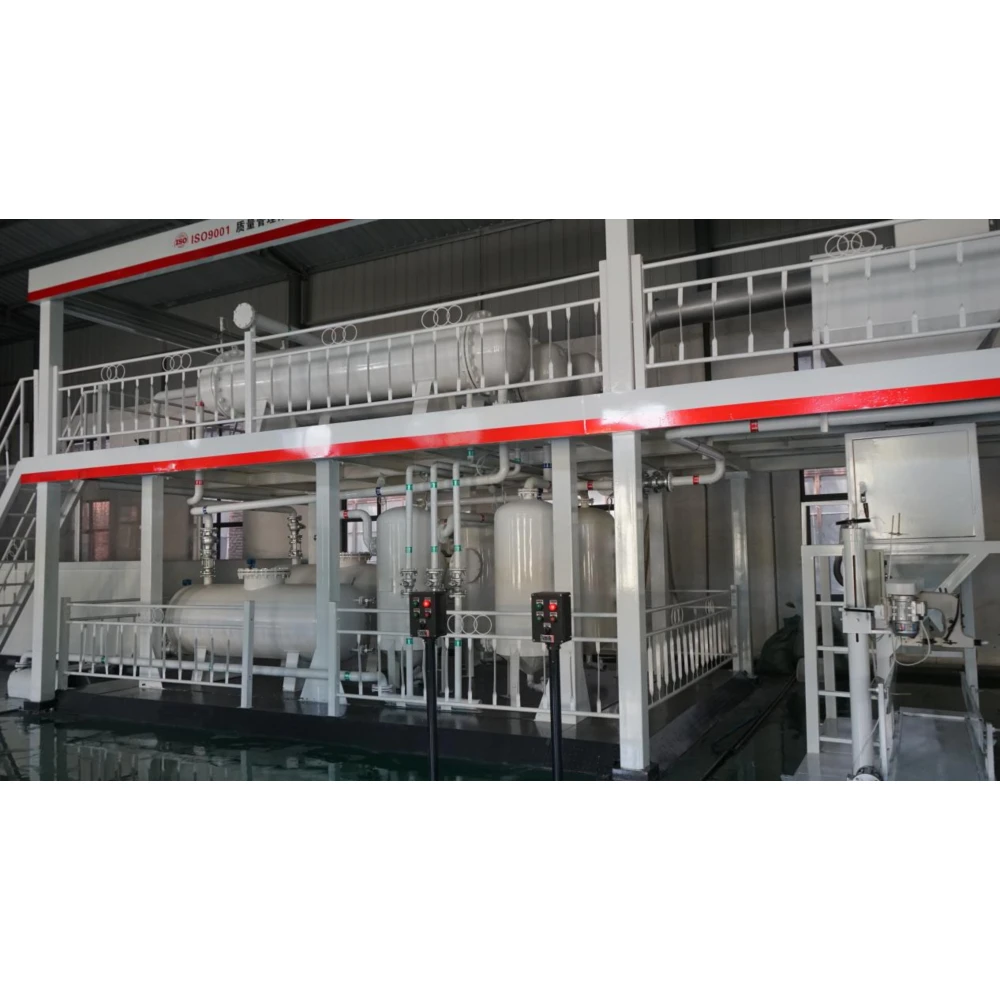
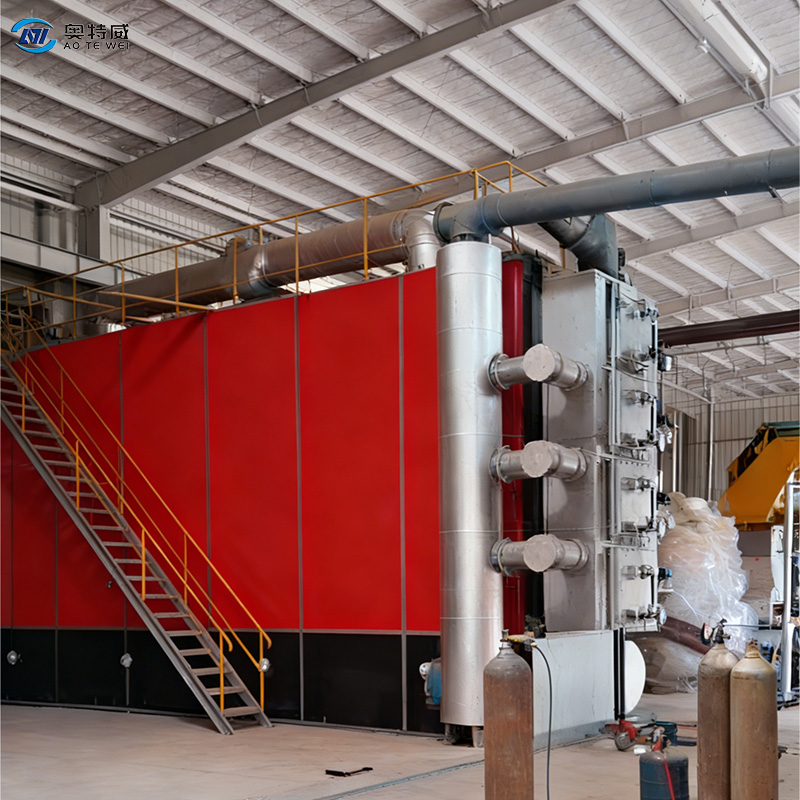
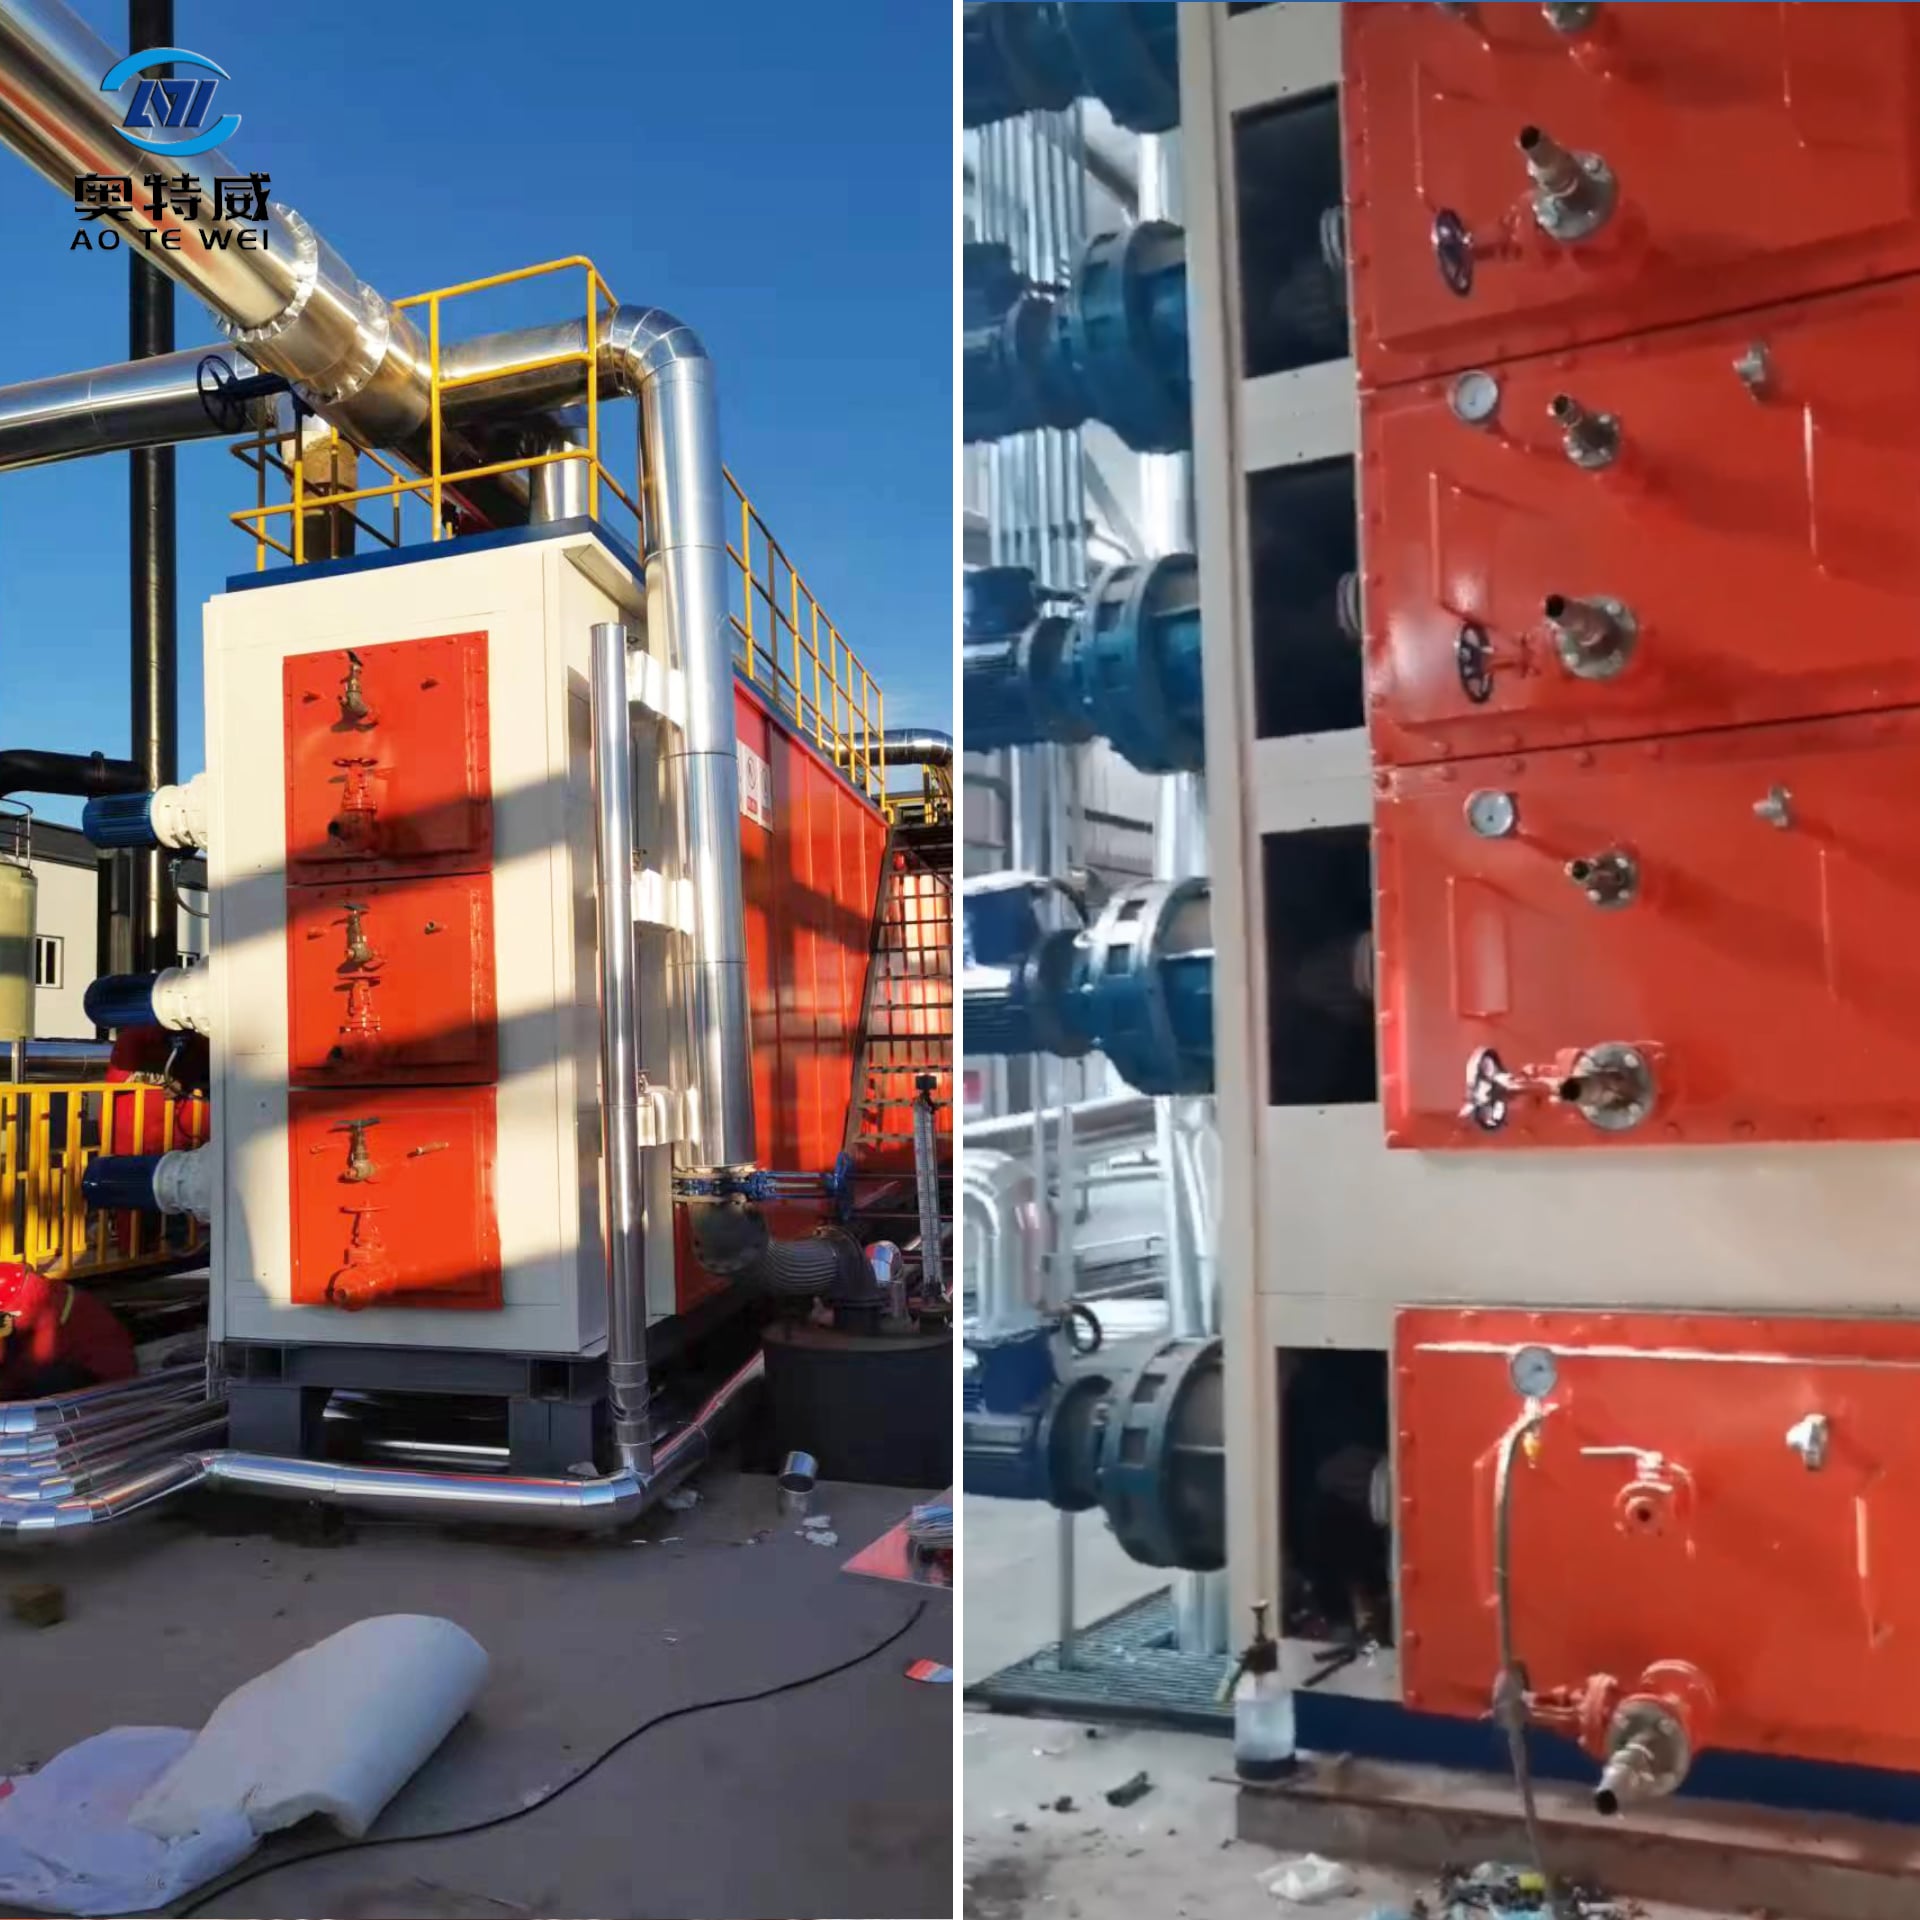
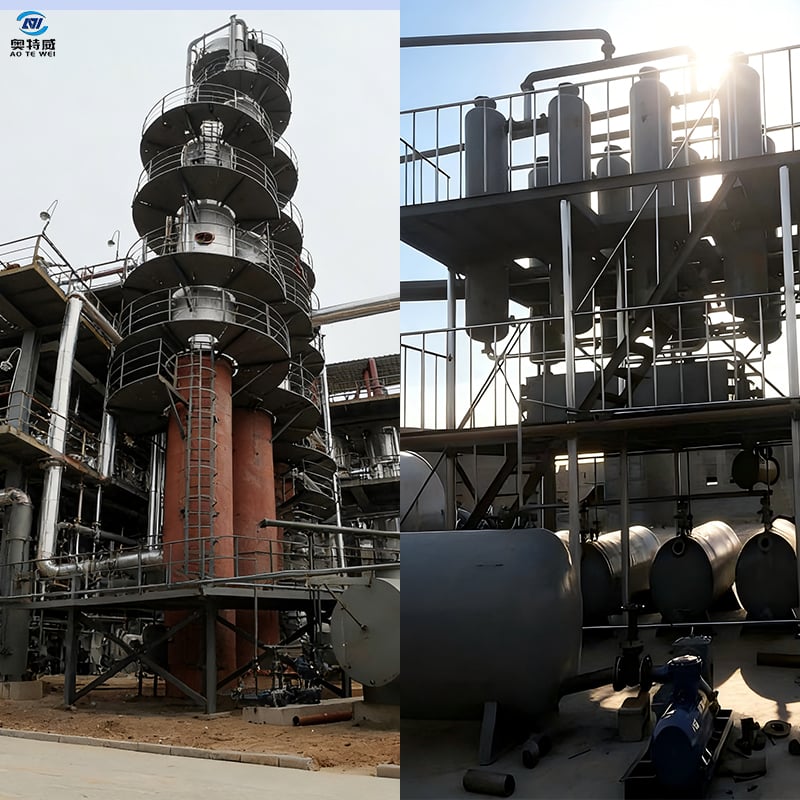
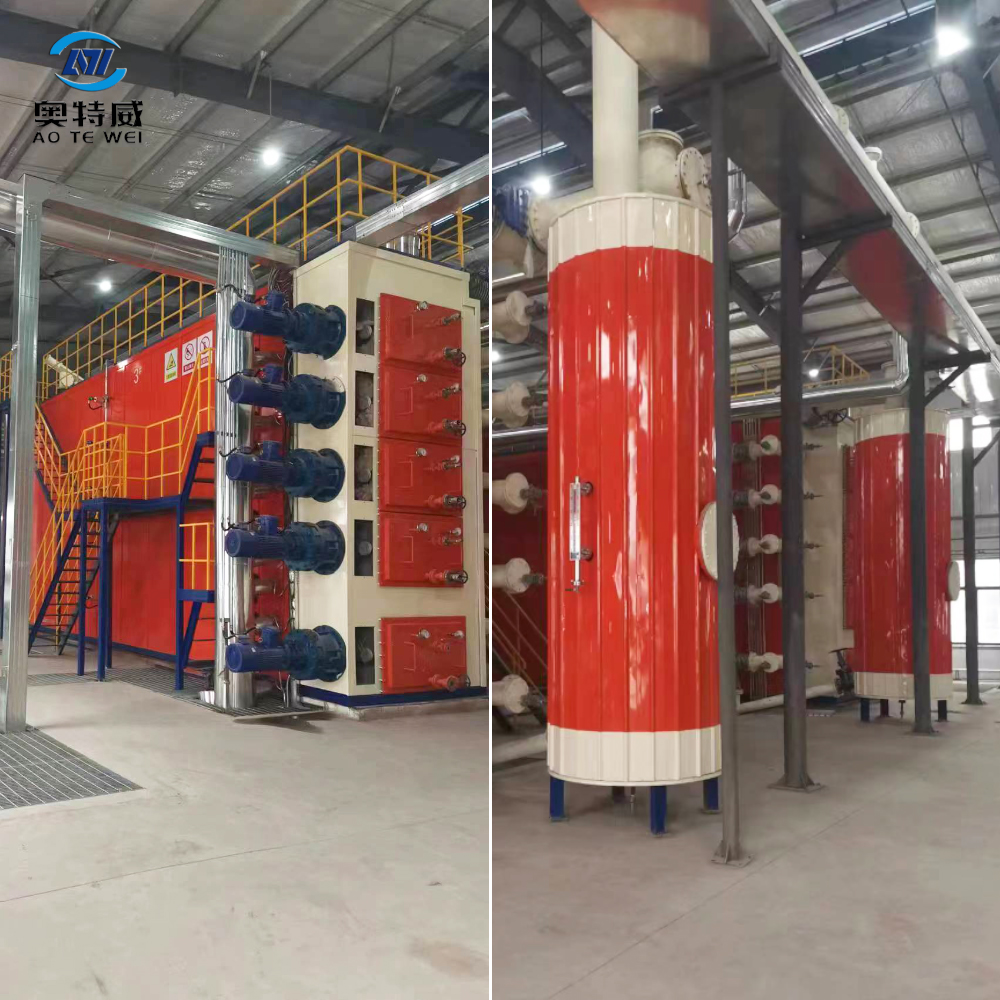
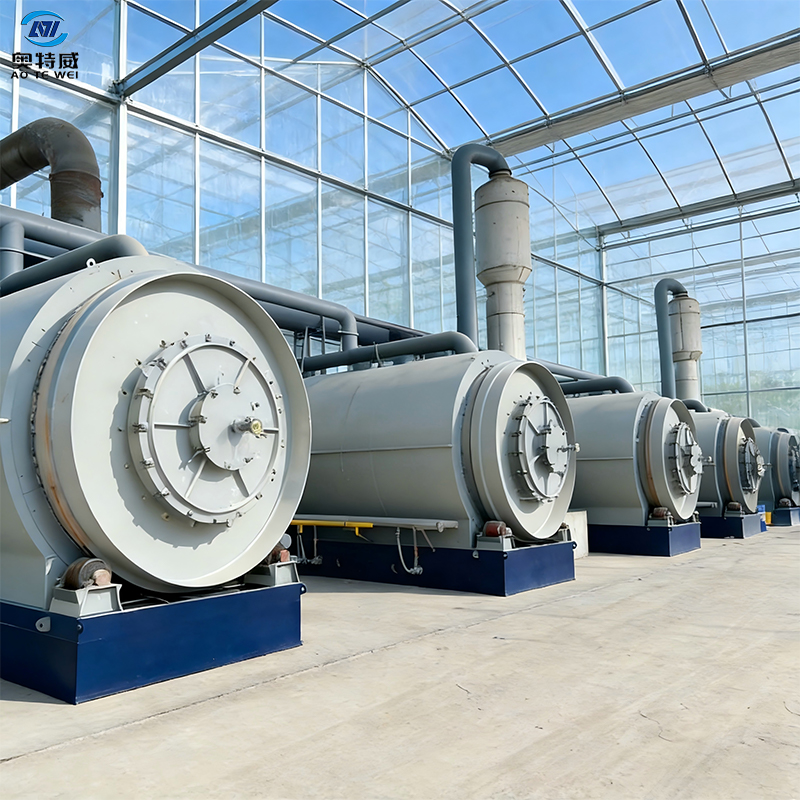
Rubber recycling equipment represents a sophisticated solution for transforming discarded rubber materials into reusable resources. This specialized machinery processes waste rubber from tires, industrial products, and consumer goods through advanced technological systems. Rubber recycling equipment operates by shredding, grinding, and separating rubber components into granules and powder suitable for various applications. The primary functions of rubber recycling equipment include size reduction, material separation, and quality enhancement. Modern rubber recycling equipment incorporates cutting-edge technology such as automated sorting systems, precision grinding mechanisms, and dust collection features. These technological advancements ensure efficient processing while maintaining environmental safety standards. Applications for rubber recycling equipment span multiple industries including construction, automotive, playground surfacing, and sports facilities. Manufacturers utilize processed rubber from this equipment to create rubber mats, athletic tracks, road surfaces, and protective barriers. The versatility of rubber recycling equipment makes it an essential investment for waste management facilities and material recovery operations. The environmental impact of rubber recycling equipment cannot be overstated. By processing waste rubber materials, this equipment diverts substantial waste from landfills while creating valuable secondary materials. Rubber recycling equipment enables businesses to meet sustainability goals while generating revenue from recovered materials, making it an economically viable and environmentally responsible choice for modern recycling operations.
New Product Releases

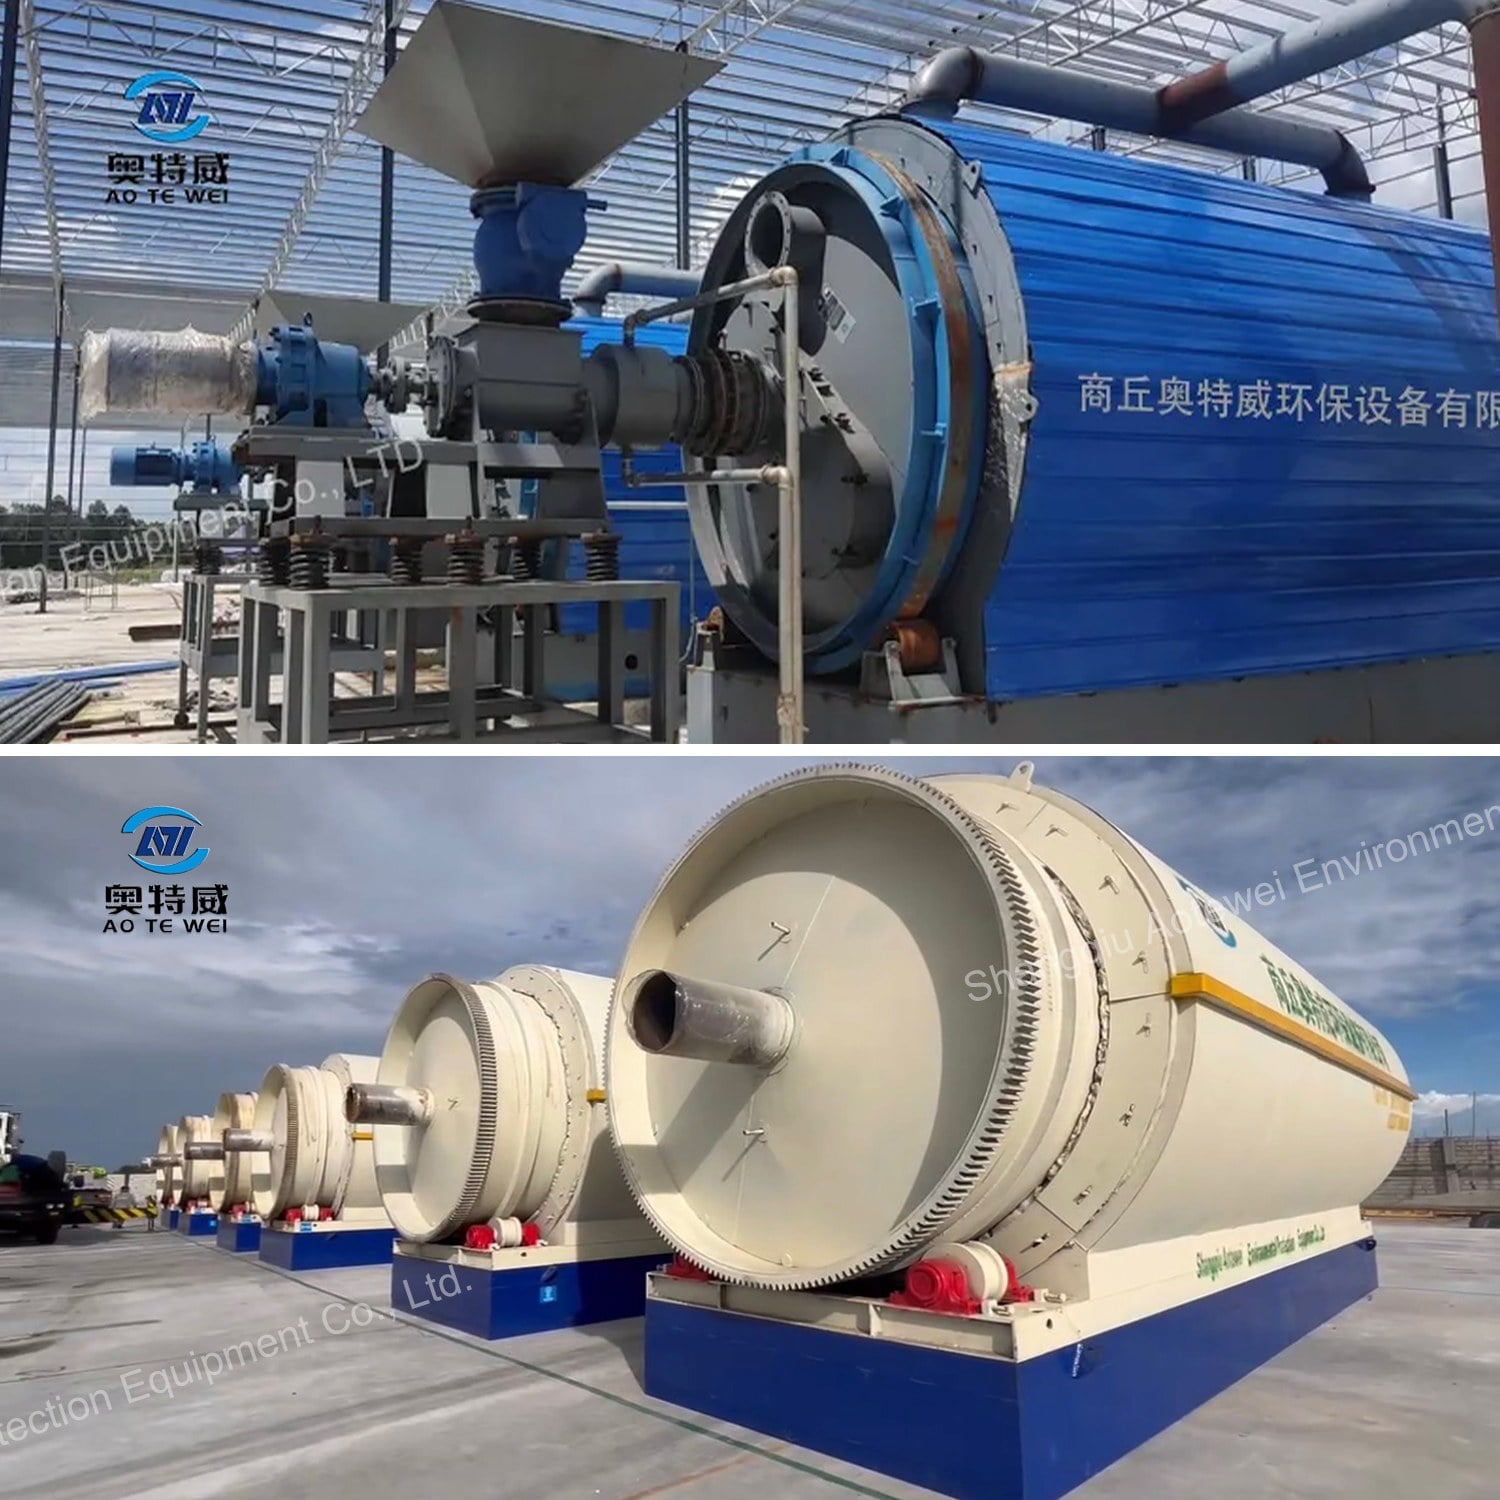
Rubber recycling equipment delivers substantial economic and operational benefits to businesses seeking sustainable waste management solutions. First, this equipment significantly reduces disposal costs by transforming waste rubber into marketable products, directly improving your bottom line. Rubber recycling equipment generates revenue streams through the production of valuable recycled materials, offsetting operational expenses while creating profitable business opportunities. Operational efficiency represents another major advantage of rubber recycling equipment. The automated systems integrated into modern rubber recycling equipment minimize labor requirements and maximize processing capacity. Your facility can process larger volumes of waste rubber with fewer personnel, reducing overhead costs while increasing productivity and throughput. Environmental compliance becomes effortless with rubber recycling equipment, as these systems help businesses meet strict waste management regulations and sustainability requirements. Investing in rubber recycling equipment demonstrates corporate environmental responsibility, enhancing brand reputation and appealing to environmentally conscious customers and stakeholders. The versatility of rubber recycling equipment makes it suitable for diverse industrial applications and market segments. Whether you operate a tire recycling facility, waste management center, or manufacturing plant, rubber recycling equipment adapts to your specific processing needs and material requirements. This adaptability ensures long-term value and relevance as your business evolves and market demands change. Finally, rubber recycling equipment requires minimal maintenance compared to traditional waste processing systems. The durable construction and advanced engineering of quality rubber recycling equipment ensure consistent performance and extended equipment lifespan. Lower maintenance demands translate directly to reduced downtime, lower repair costs, and improved overall return on investment for your recycling operation.

Latest News

How does oil distillation improve purity and usability of recycled oil products?

01

Sep

How does oil distillation improve purity and usability of recycled oil products?

Oil distillation represents one of the most effective methods for restoring the quality and usability of recycled oil products in modern industrial operations. As environmental regulations tighten and resource costs rise, the ability to recycle used ...
View More
Why do recycling plants rely on pyrolysis reactor technology for energy recovery?

01

Sep

Why do recycling plants rely on pyrolysis reactor technology for energy recovery?

Modern recycling plants face mounting pressure to recover maximum value from waste streams while maintaining environmental compliance. The pyrolysis reactor has emerged as a critical technology for achieving this balance, transforming discarded mater...
View More
How does rubber recycling contribute to eco-friendly industrial development goals?

01

Sep

How does rubber recycling contribute to eco-friendly industrial development goals?

Rubber recycling has emerged as a critical pillar in achieving eco-friendly industrial development goals across manufacturing, construction, and transportation sectors. As global industries face mounting pressure to reduce environmental impact and ad...
View More
How does rubber recycling improve material reuse in manufacturing industries?

01

Sep

How does rubber recycling improve material reuse in manufacturing industries?

Rubber recycling represents one of the most effective strategies for transforming industrial waste into valuable manufacturing resources. As manufacturing industries face increasing pressure to reduce environmental footprints and optimize material co...
View More

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

rubber recycling equipment

Advanced Processing Technology

Advanced Processing Technology

Modern rubber recycling equipment incorporates state-of-the-art technology that maximizes material recovery and processing efficiency. The grinding and shredding mechanisms within rubber recycling equipment utilize precision engineering to achieve consistent particle sizes and optimal material specifications. Advanced sensors and automated controls ensure that your rubber recycling equipment operates at peak performance throughout the processing cycle. The technological sophistication of rubber recycling equipment enables operators to customize output specifications according to specific market demands and application requirements. Whether producing fine powder, granules, or crumb rubber, this equipment delivers superior quality products that command premium market prices. The integration of dust collection systems within rubber recycling equipment maintains clean operating environments while capturing valuable fine materials that would otherwise be wasted, maximizing your material recovery rates and profitability.
Cost-Effective Operations

Cost-Effective Operations

Investing in rubber recycling equipment represents a strategic financial decision that delivers impressive return on investment within reasonable timeframes. The operational cost savings generated by rubber recycling equipment through reduced labor requirements and lower disposal fees accumulate quickly, making this equipment financially attractive for businesses of all sizes. Rubber recycling equipment enables facilities to convert waste materials into revenue-generating products, transforming what was once an expense into a profit center. The scalability of rubber recycling equipment allows businesses to start with basic systems and expand capacity as demand grows and revenues increase. This flexible approach to investment means you can implement rubber recycling equipment without overwhelming financial burden. Lower maintenance requirements further enhance the cost-effectiveness of rubber recycling equipment, as these systems are engineered for durability and reliability, minimizing unexpected expenses and downtime that could disrupt your operations.
Environmental and Regulatory Benefits

Environmental and Regulatory Benefits

Rubber recycling equipment provides comprehensive environmental benefits by diverting substantial quantities of waste rubber from landfills into productive reuse cycles. Implementing rubber recycling equipment demonstrates your commitment to sustainability and environmental stewardship, positioning your business as a responsible corporate citizen. This equipment helps your facility exceed environmental compliance requirements while reducing your carbon footprint through waste reduction and material recovery. Regulatory agencies increasingly favor businesses that invest in rubber recycling equipment, often providing incentives, grants, or preferred licensing status. By implementing rubber recycling equipment, your business aligns with global sustainability initiatives and meets consumer expectations for environmentally responsible practices. The documentation and tracking capabilities of rubber recycling equipment help you demonstrate compliance with environmental regulations, protecting your business from potential penalties and regulatory issues while building customer trust and loyalty.

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000
Newsletter
Please Leave A Message With Us