Advanced Tire Recycling Solutions

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

advanced tire recycling

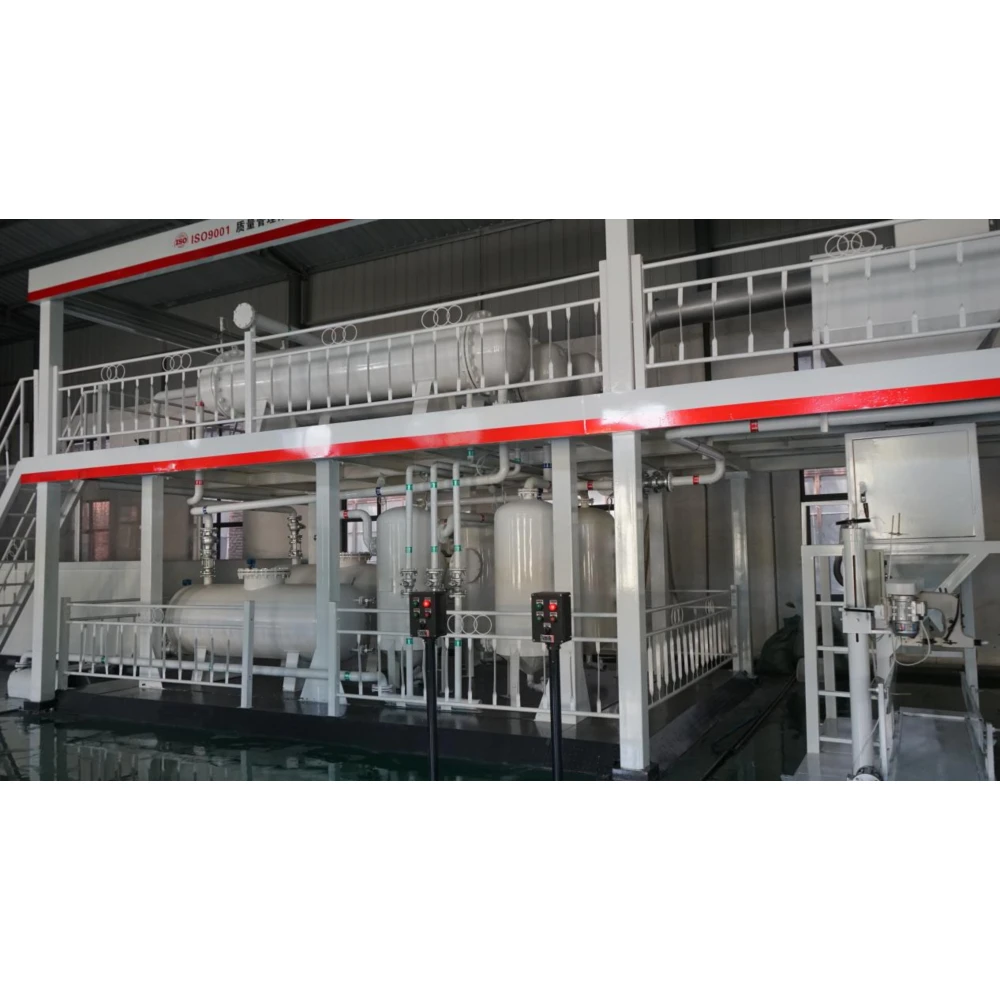
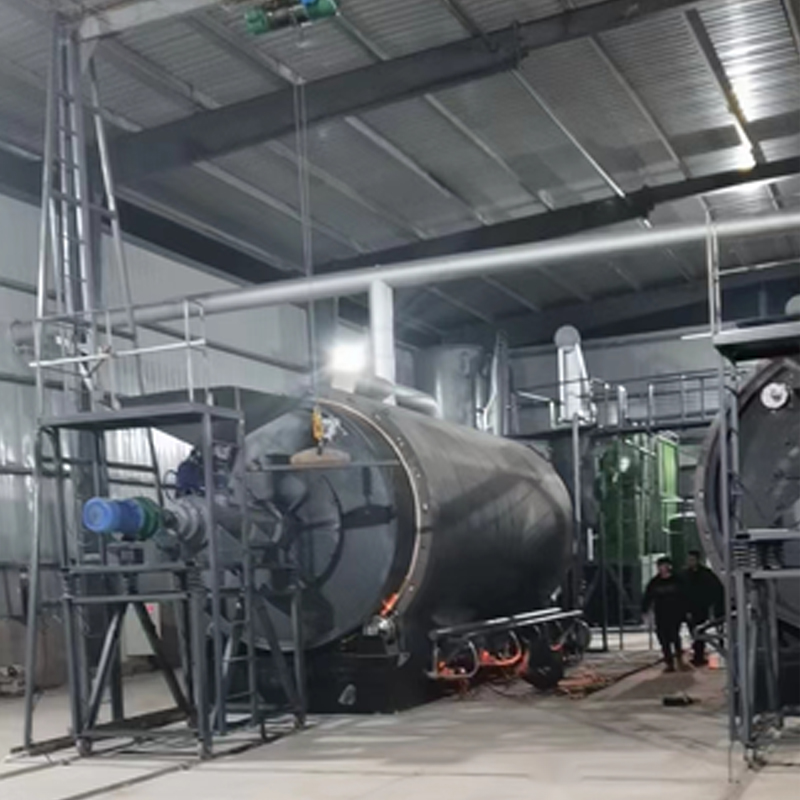
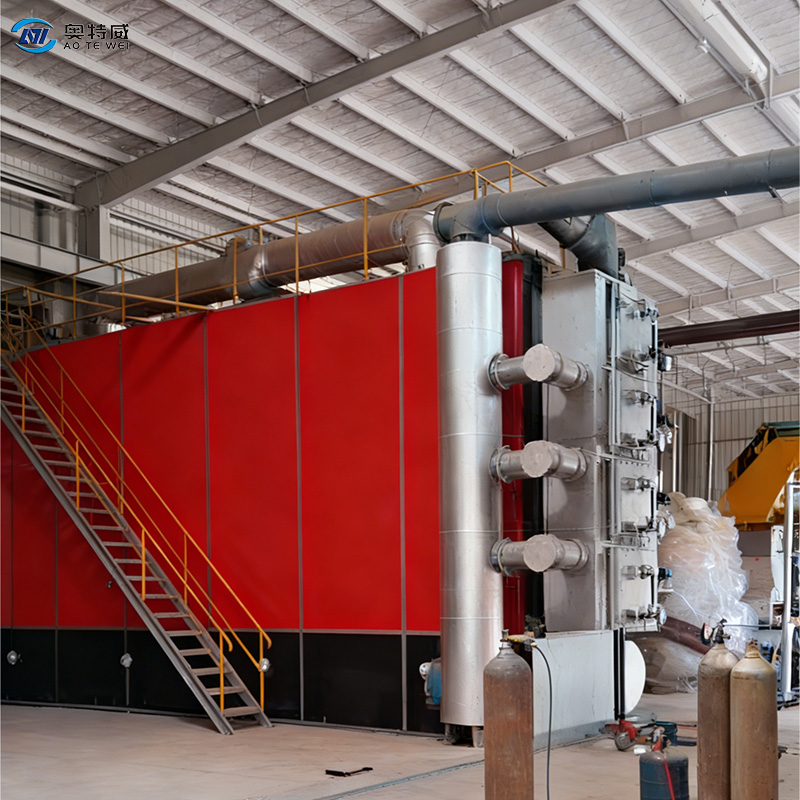
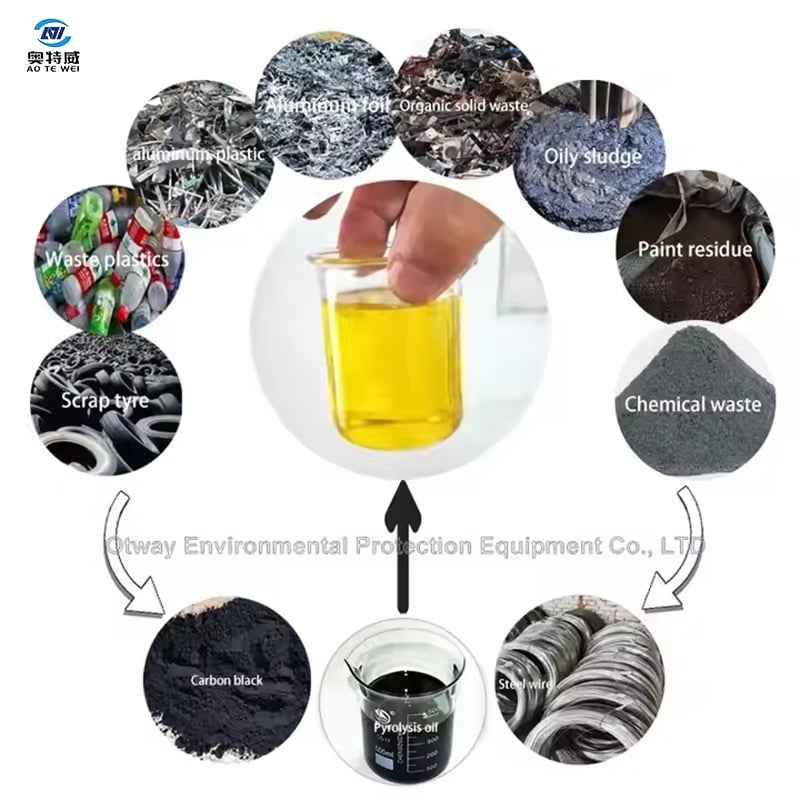
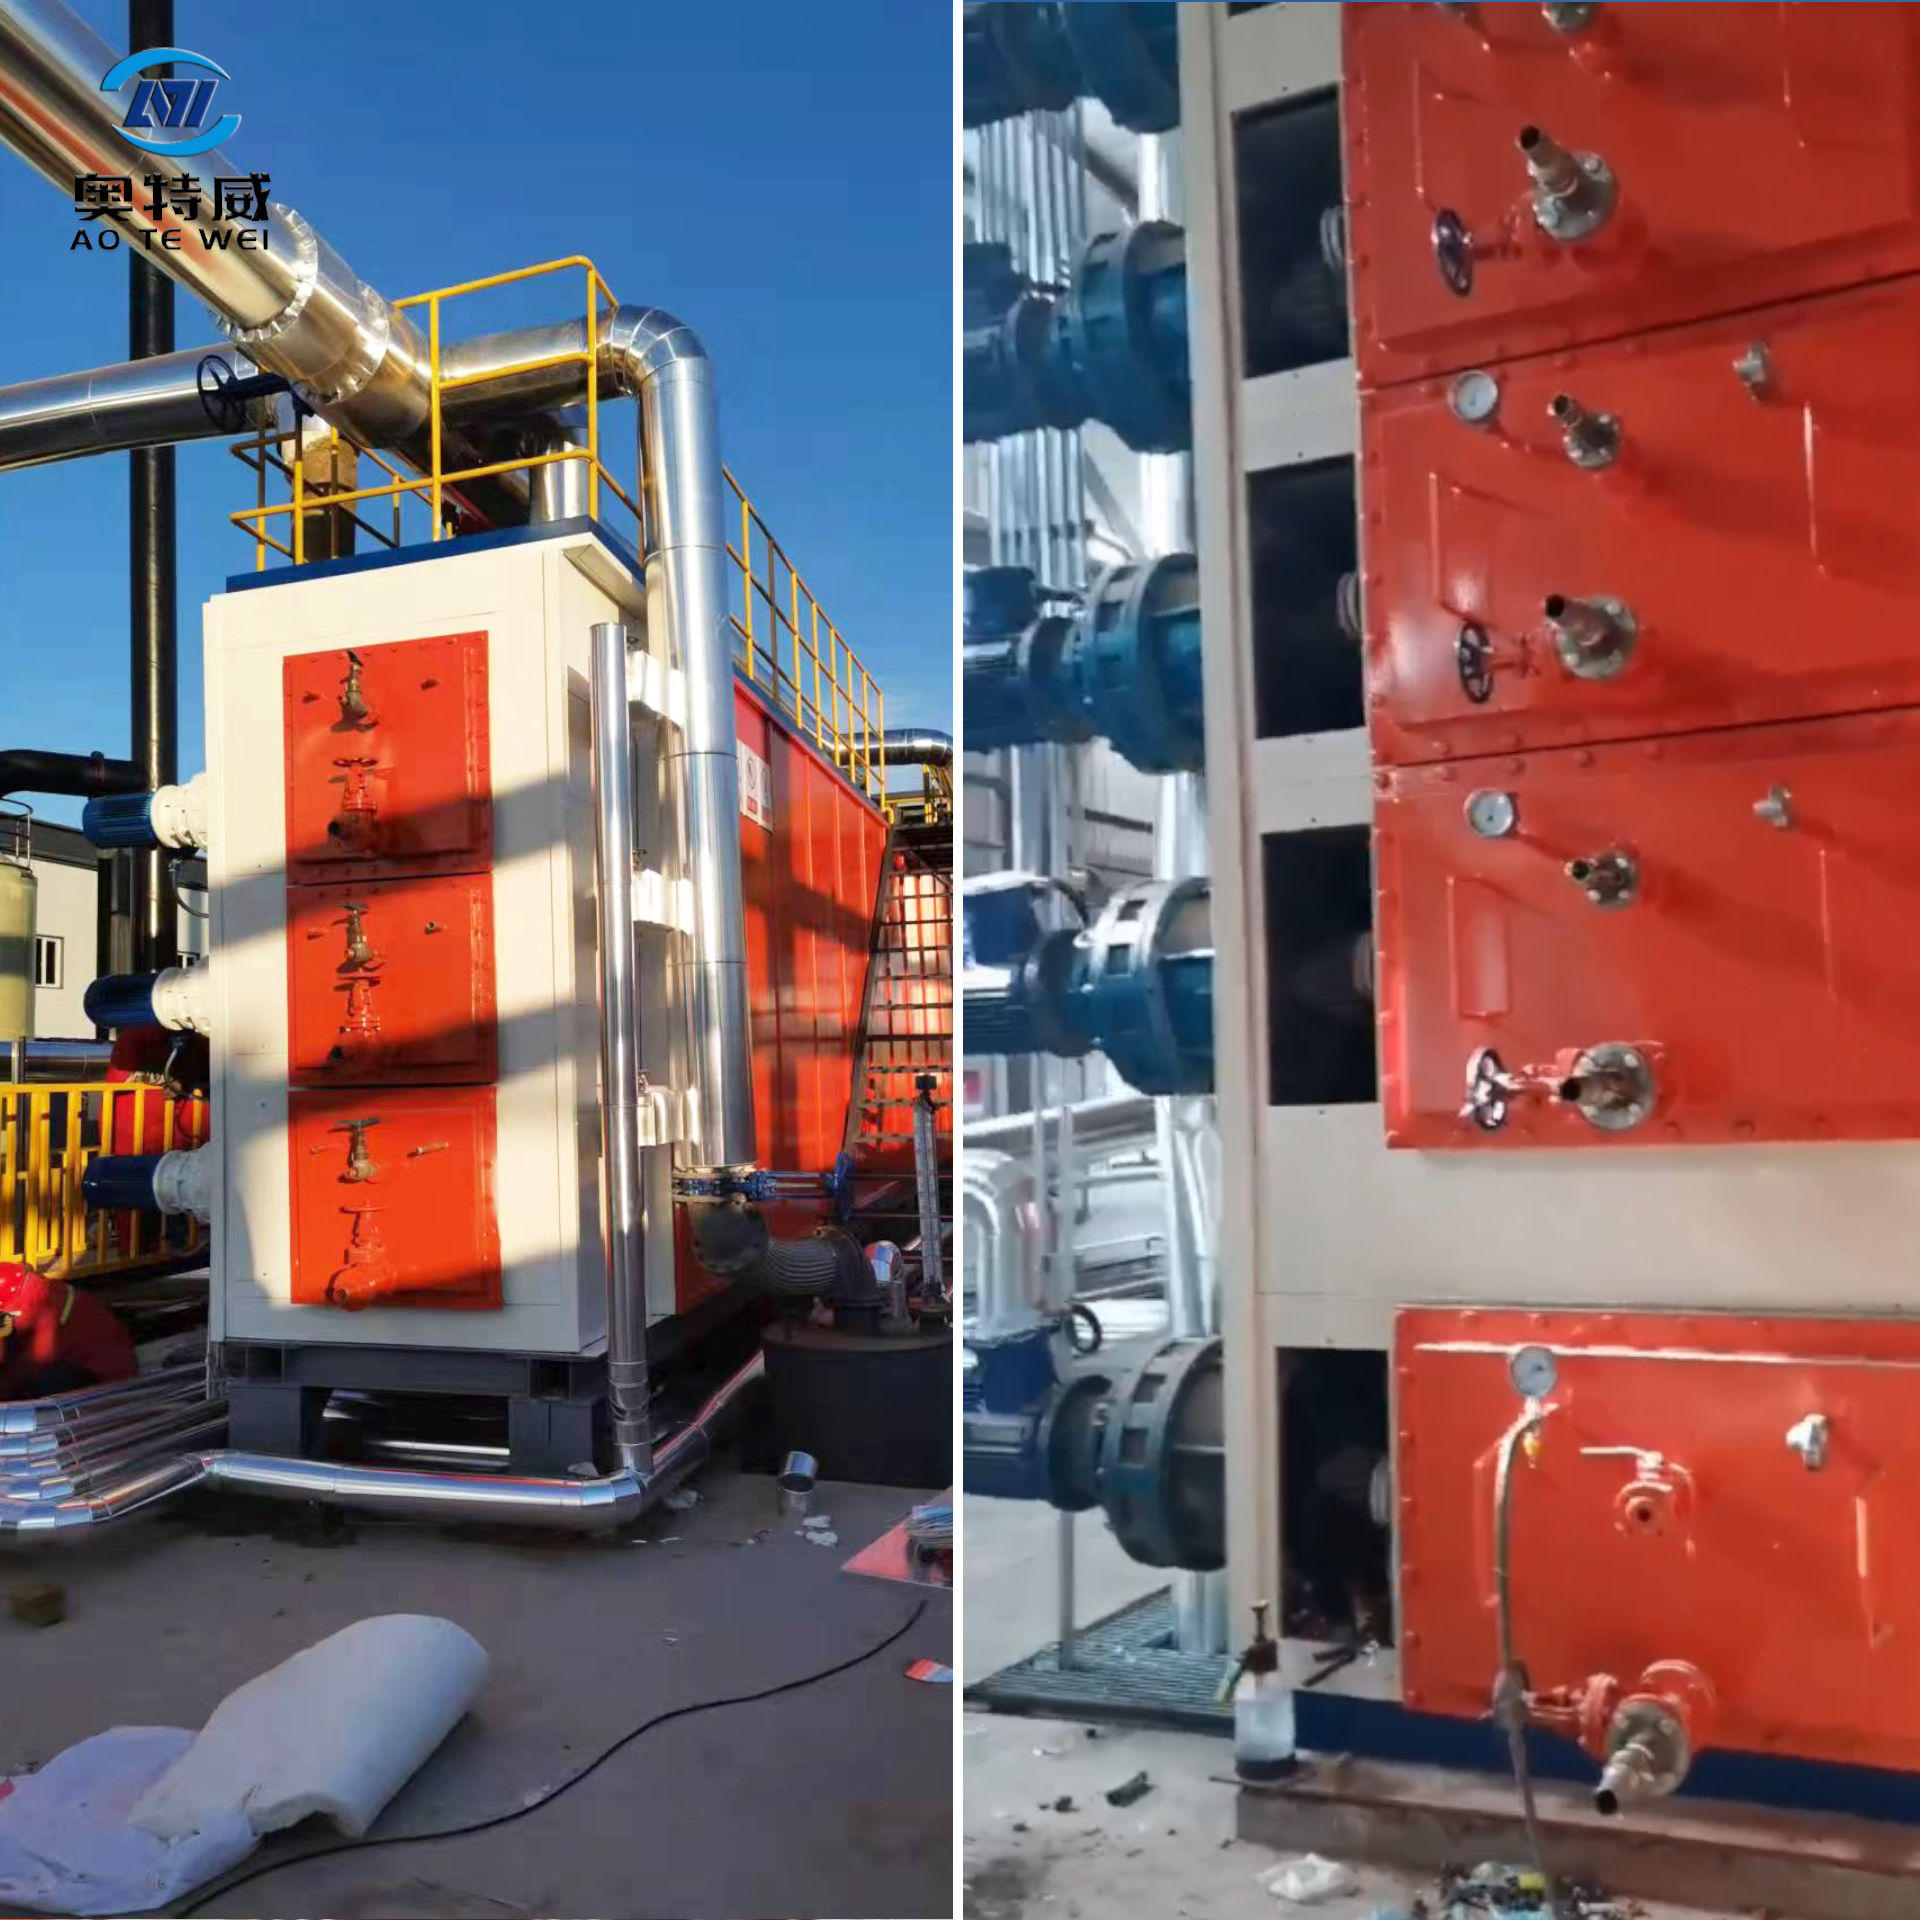
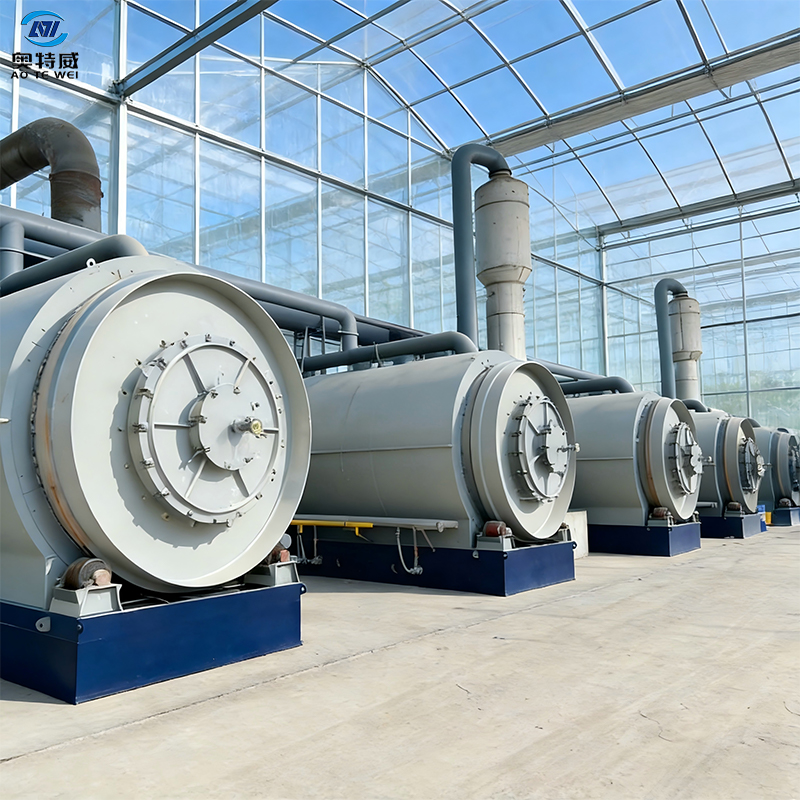
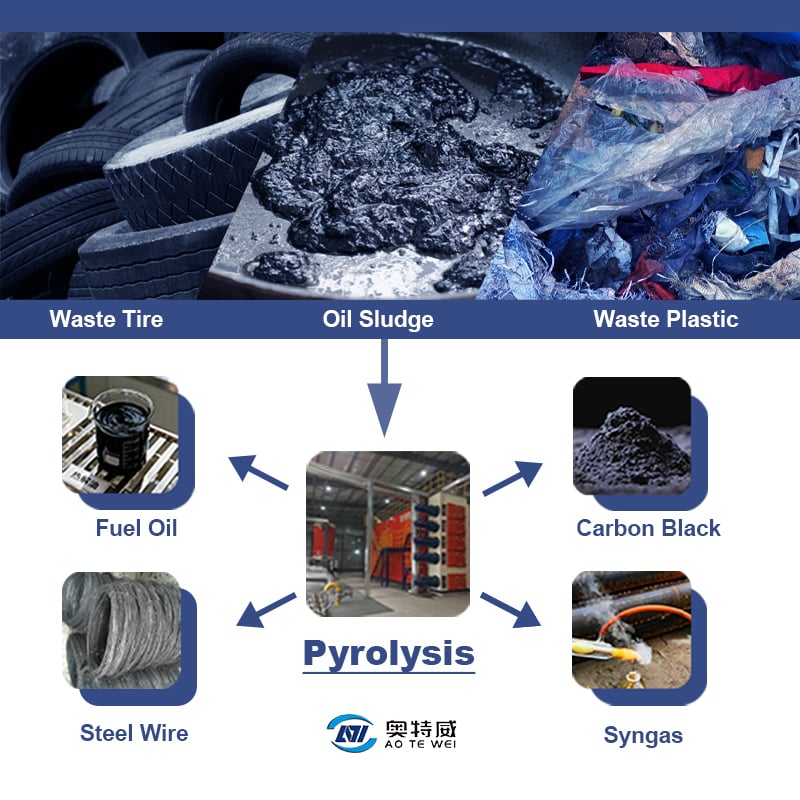
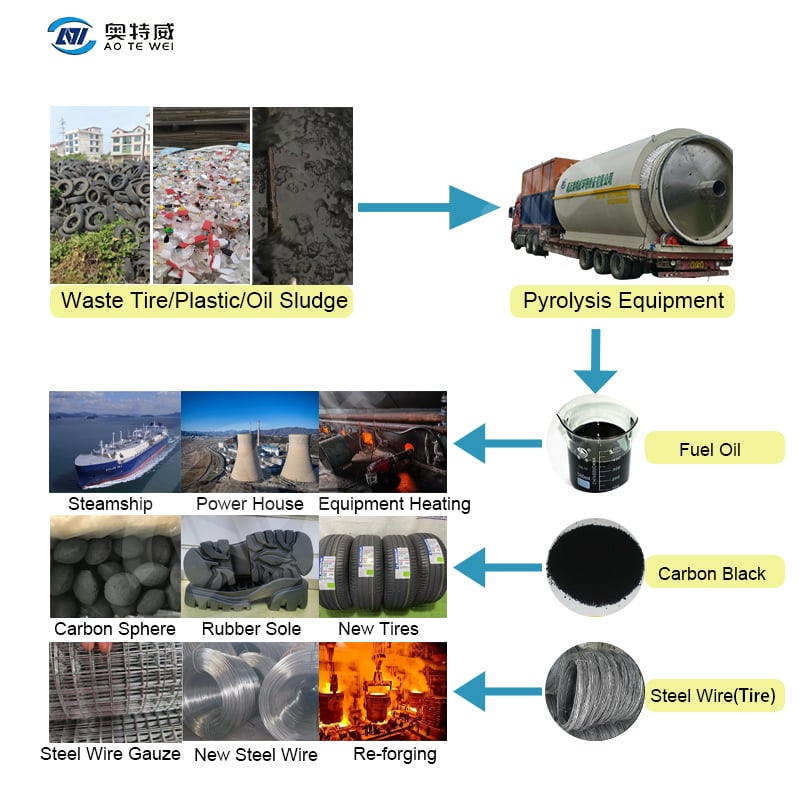
Advanced tire recycling represents a sophisticated environmental solution that transforms end-of-life tires into valuable resources through cutting-edge processing technology. Advanced tire recycling systems utilize mechanical shredding, pyrolysis, and devulcanization techniques to break down worn tires into reusable components including rubber granules, steel wire, and textile fibers. These recycled materials serve multiple industries, from playground surfaces and athletic tracks to asphalt additives and automotive components. The main functions of advanced tire recycling include tire collection and sorting, size reduction through industrial shredders, separation of rubber from steel and fabric, and quality grading of final products. Technological features encompass automated sorting systems, cryogenic freezing processes that improve rubber brittleness for easier processing, and advanced separation equipment that maximizes material recovery rates. Environmental benefits are substantial, as advanced tire recycling diverts millions of tons from landfills annually while reducing carbon emissions compared to raw material extraction. Applications span construction, playground safety surfacing, civil engineering projects, and manufacturing. The technology supports the circular economy by creating secondary raw materials that reduce production costs and environmental impact. Modern advanced tire recycling facilities operate continuously, processing diverse tire types while maintaining rigorous quality standards for output materials. This comprehensive approach addresses both waste management challenges and resource scarcity issues facing global industries today.
Popular Products

Advanced tire recycling delivers transformative benefits that make it an essential choice for environmentally conscious businesses and communities seeking sustainable waste solutions. The primary advantage is environmental responsibility—advanced tire recycling prevents millions of tons of tires from accumulating in landfills, reducing hazardous waste and associated environmental contamination risks. Cost efficiency represents another significant benefit, as recycled rubber and steel materials cost substantially less than virgin materials, allowing manufacturers to reduce production expenses while maintaining quality standards. Operational benefits include consistent supply chain advantages, as advanced tire recycling creates a reliable local source of raw materials that reduces transportation costs and supply chain vulnerabilities associated with imported virgin resources. Regulatory compliance becomes simpler when utilizing advanced tire recycling products, as many jurisdictions now mandate recycled content in specific applications, making compliant materials readily available. Market reputation improves dramatically when companies demonstrate commitment to circular economy principles through advanced tire recycling adoption. The process creates employment opportunities throughout collection, processing, and distribution networks, supporting local economic development. Practical applications expand significantly—recycled materials from advanced tire recycling work excellently in playground installations, road construction, athletic facilities, and industrial manufacturing. Decision-useful context shows that advanced tire recycling technology continuously improves, offering better material quality and processing efficiency than traditional methods. Customers benefit from reliable product consistency, environmental certifications, and partnership with facilities maintaining highest safety standards. Investment in advanced tire recycling demonstrates corporate social responsibility while generating tangible financial returns through material cost reductions and operational efficiency gains across multiple business sectors.

Latest News

How does oil distillation improve purity and usability of recycled oil products?

01

Sep

How does oil distillation improve purity and usability of recycled oil products?

Oil distillation represents one of the most effective methods for restoring the quality and usability of recycled oil products in modern industrial operations. As environmental regulations tighten and resource costs rise, the ability to recycle used ...
View More
What factors affect profitability in plastic recycling industry operations?

30

Jul

What factors affect profitability in plastic recycling industry operations?

The plastic recycling industry has grown into a significant economic sector, yet many operators struggle to achieve consistent profit margins. Understanding what drives profitability in plastic recycling is essential for anyone planning to enter or e...
View More
What factors influence performance of a pyrolysis reactor in industrial applications?

01

Sep

What factors influence performance of a pyrolysis reactor in industrial applications?

The performance of a pyrolysis reactor directly determines the efficiency, profitability, and sustainability of waste processing and renewable energy operations. Understanding the critical factors that influence pyrolysis reactor output is essential ...
View More
How does a continuous pyrolysis plant support uninterrupted industrial production?

03

Sep

How does a continuous pyrolysis plant support uninterrupted industrial production?

Industrial manufacturers face significant operational challenges when production must halt for maintenance or equipment downtime. A continuous pyrolysis plant eliminates these disruptions by maintaining consistent, uninterrupted output throughout the...
View More

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

advanced tire recycling

Environmental Impact and Sustainability

Environmental Impact and Sustainability

Advanced tire recycling transforms environmental responsibility into measurable action by preventing tire accumulation in landfills and reducing overall waste streams significantly. Each tire processed through advanced tire recycling systems represents avoided environmental contamination, as improperly disposed tires create breeding grounds for disease vectors and contribute to soil degradation over decades. The sustainability aspect of advanced tire recycling extends beyond waste prevention—it actively reduces carbon emissions by eliminating the need for virgin rubber production and petroleum-intensive manufacturing processes. By implementing advanced tire recycling, facilities divert approximately 1.5 tons of rubber annually per processing unit, creating positive environmental impact at scale. The technology supports climate goals through material reuse, reducing greenhouse gas emissions by up to 40 percent compared to virgin material production. Communities adopting advanced tire recycling contribute meaningfully to global circular economy initiatives while protecting local ecosystems from tire-related pollution.
Cost Efficiency and Economic Benefits

Cost Efficiency and Economic Benefits

Advanced tire recycling delivers substantial financial advantages through material cost reductions and operational efficiency improvements that directly impact bottom-line profitability. Recycled materials produced by advanced tire recycling systems cost 30-50 percent less than equivalent virgin materials, allowing manufacturers to significantly reduce raw material expenses. The economic model supporting advanced tire recycling creates multiple revenue streams through material sales, tipping fees for tire collection, and government incentives promoting sustainable practices. Businesses implementing advanced tire recycling reduce procurement costs while maintaining strict quality control over material specifications and performance standards. Investment in advanced tire recycling facilities generates long-term returns through consistent material supply, eliminating price volatility associated with crude oil and virgin rubber markets. Employment creation represents another economic benefit, as advanced tire recycling operations employ skilled technicians, equipment operators, and logistics professionals throughout facility operations and distribution networks.
Versatile Applications and Material Quality

Versatile Applications and Material Quality

Advanced tire recycling produces premium-grade materials suitable for diverse industrial applications, from infrastructure projects to consumer products requiring high-performance characteristics. Rubber granules from advanced tire recycling serve playground safety surfacing, athletic track construction, and industrial vibration dampening applications with exceptional durability and safety credentials. Steel reinforcement extracted through advanced tire recycling technology provides construction-grade material for concrete reinforcement and industrial manufacturing applications. Advanced tire recycling output meets rigorous quality standards, ensuring material consistency that manufacturers require for reliable production processes and final product performance. Textile fibers recovered from advanced tire recycling support innovative applications in composite materials and geotextile manufacturing. The versatility of advanced tire recycling materials expands market opportunities across construction, manufacturing, sports, and civil engineering sectors. Quality assurance protocols embedded in advanced tire recycling processes guarantee material specifications, enabling customers to confidently specify recycled content in product specifications and regulatory compliance documentation.

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000
Newsletter
Please Leave A Message With Us