advanced tire recycling
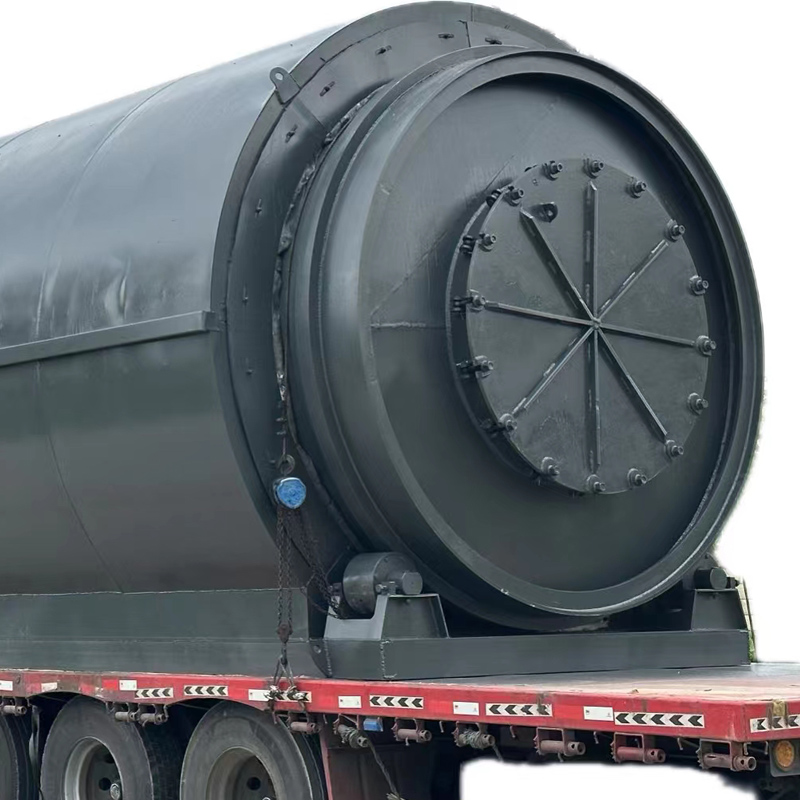
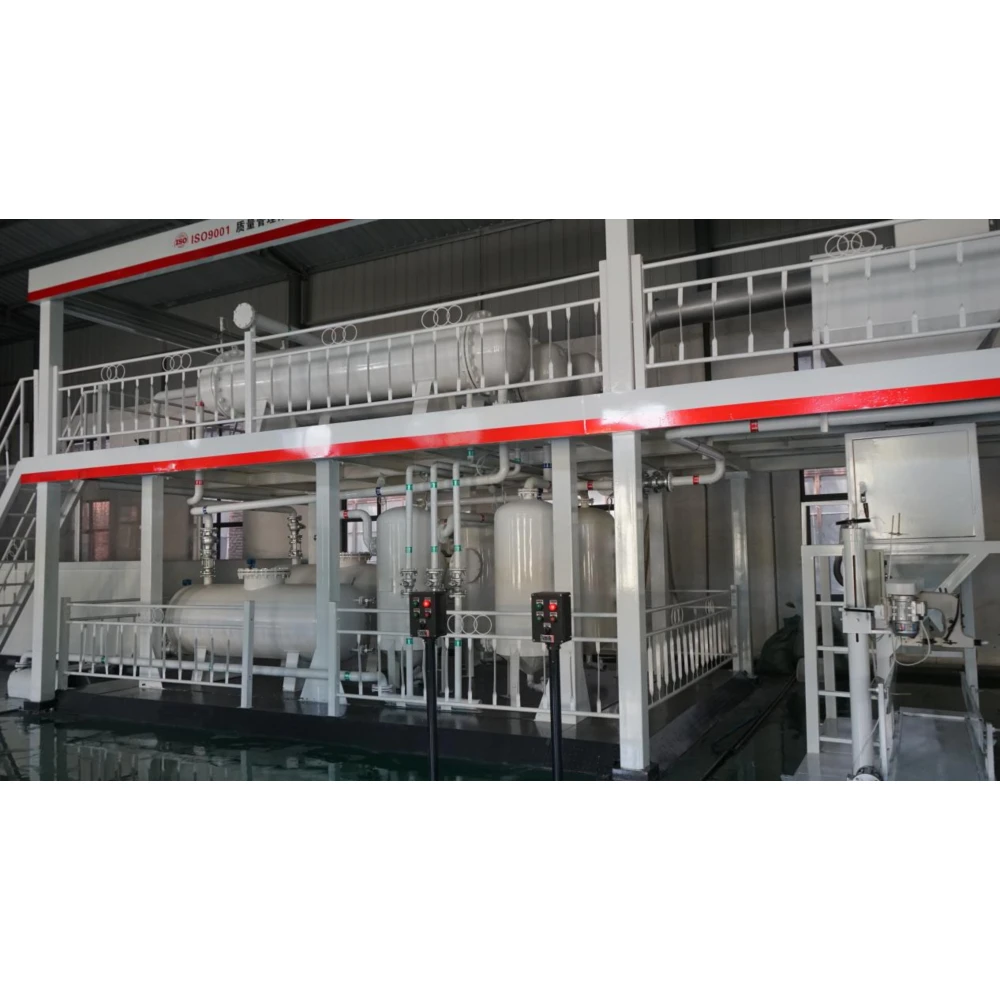
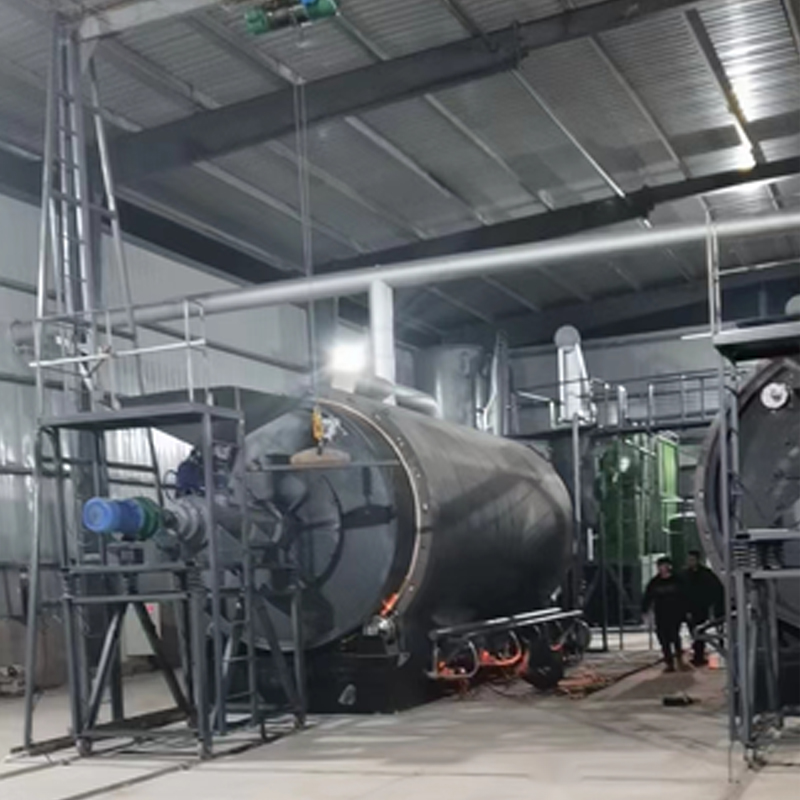
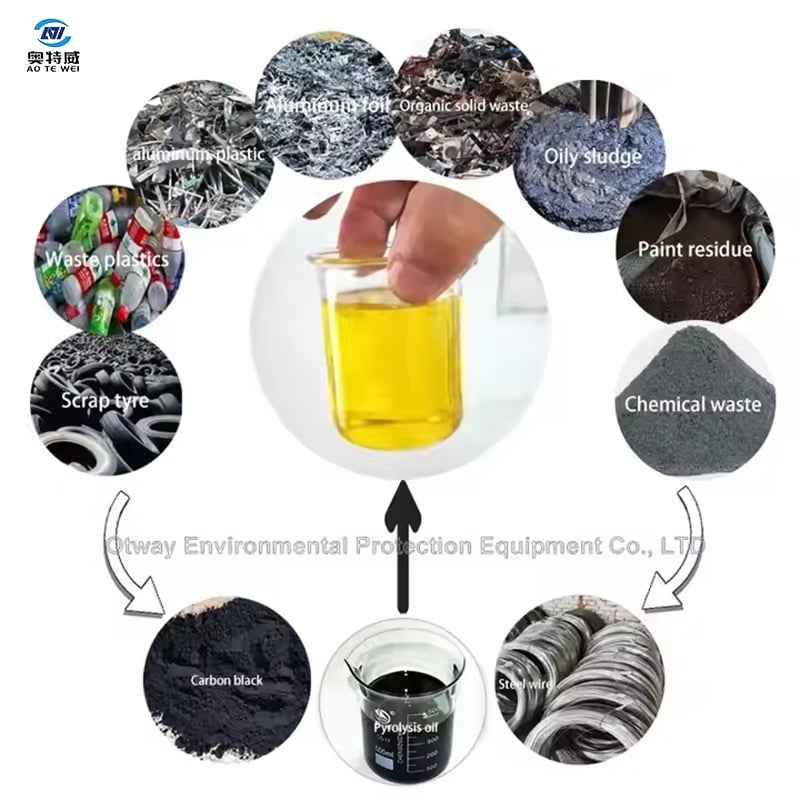
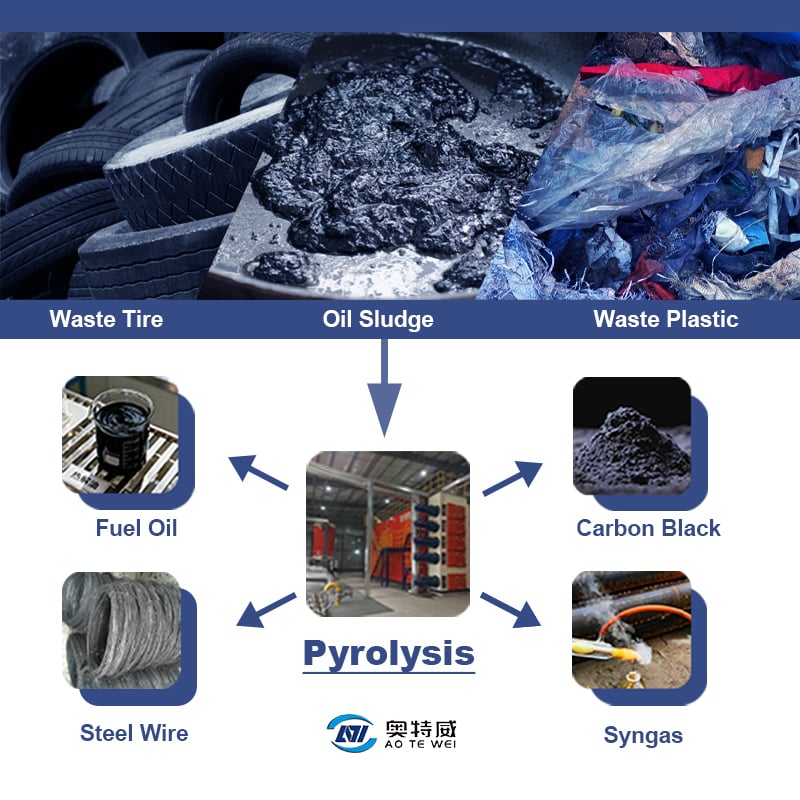
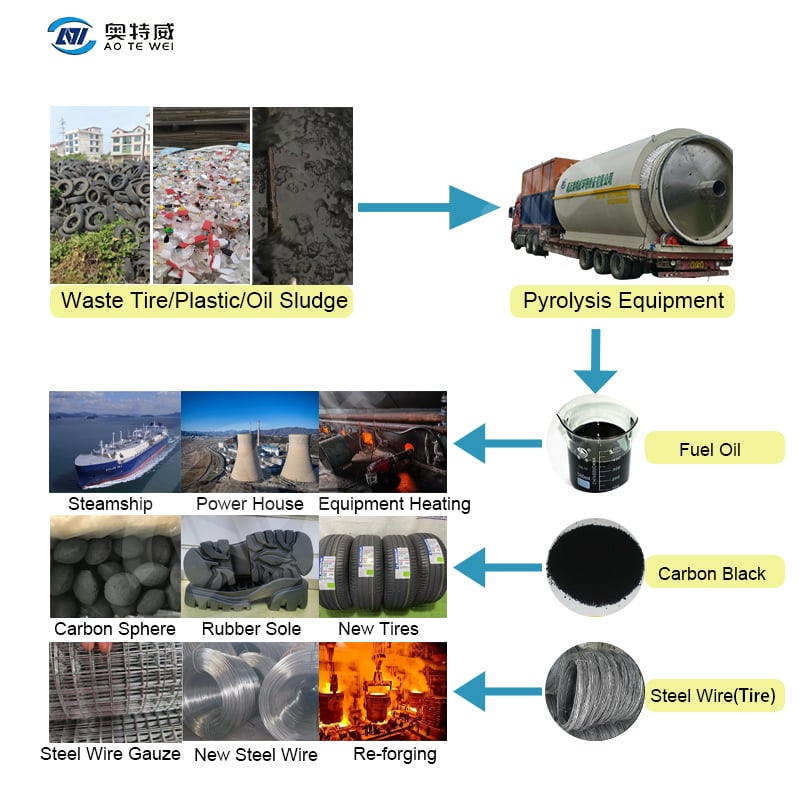
Advanced tire recycling represents a sophisticated environmental solution that transforms end-of-life tires into valuable resources through cutting-edge processing technology. Advanced tire recycling systems utilize mechanical shredding, pyrolysis, and devulcanization techniques to break down worn tires into reusable components including rubber granules, steel wire, and textile fibers. These recycled materials serve multiple industries, from playground surfaces and athletic tracks to asphalt additives and automotive components. The main functions of advanced tire recycling include tire collection and sorting, size reduction through industrial shredders, separation of rubber from steel and fabric, and quality grading of final products. Technological features encompass automated sorting systems, cryogenic freezing processes that improve rubber brittleness for easier processing, and advanced separation equipment that maximizes material recovery rates. Environmental benefits are substantial, as advanced tire recycling diverts millions of tons from landfills annually while reducing carbon emissions compared to raw material extraction. Applications span construction, playground safety surfacing, civil engineering projects, and manufacturing. The technology supports the circular economy by creating secondary raw materials that reduce production costs and environmental impact. Modern advanced tire recycling facilities operate continuously, processing diverse tire types while maintaining rigorous quality standards for output materials. This comprehensive approach addresses both waste management challenges and resource scarcity issues facing global industries today.