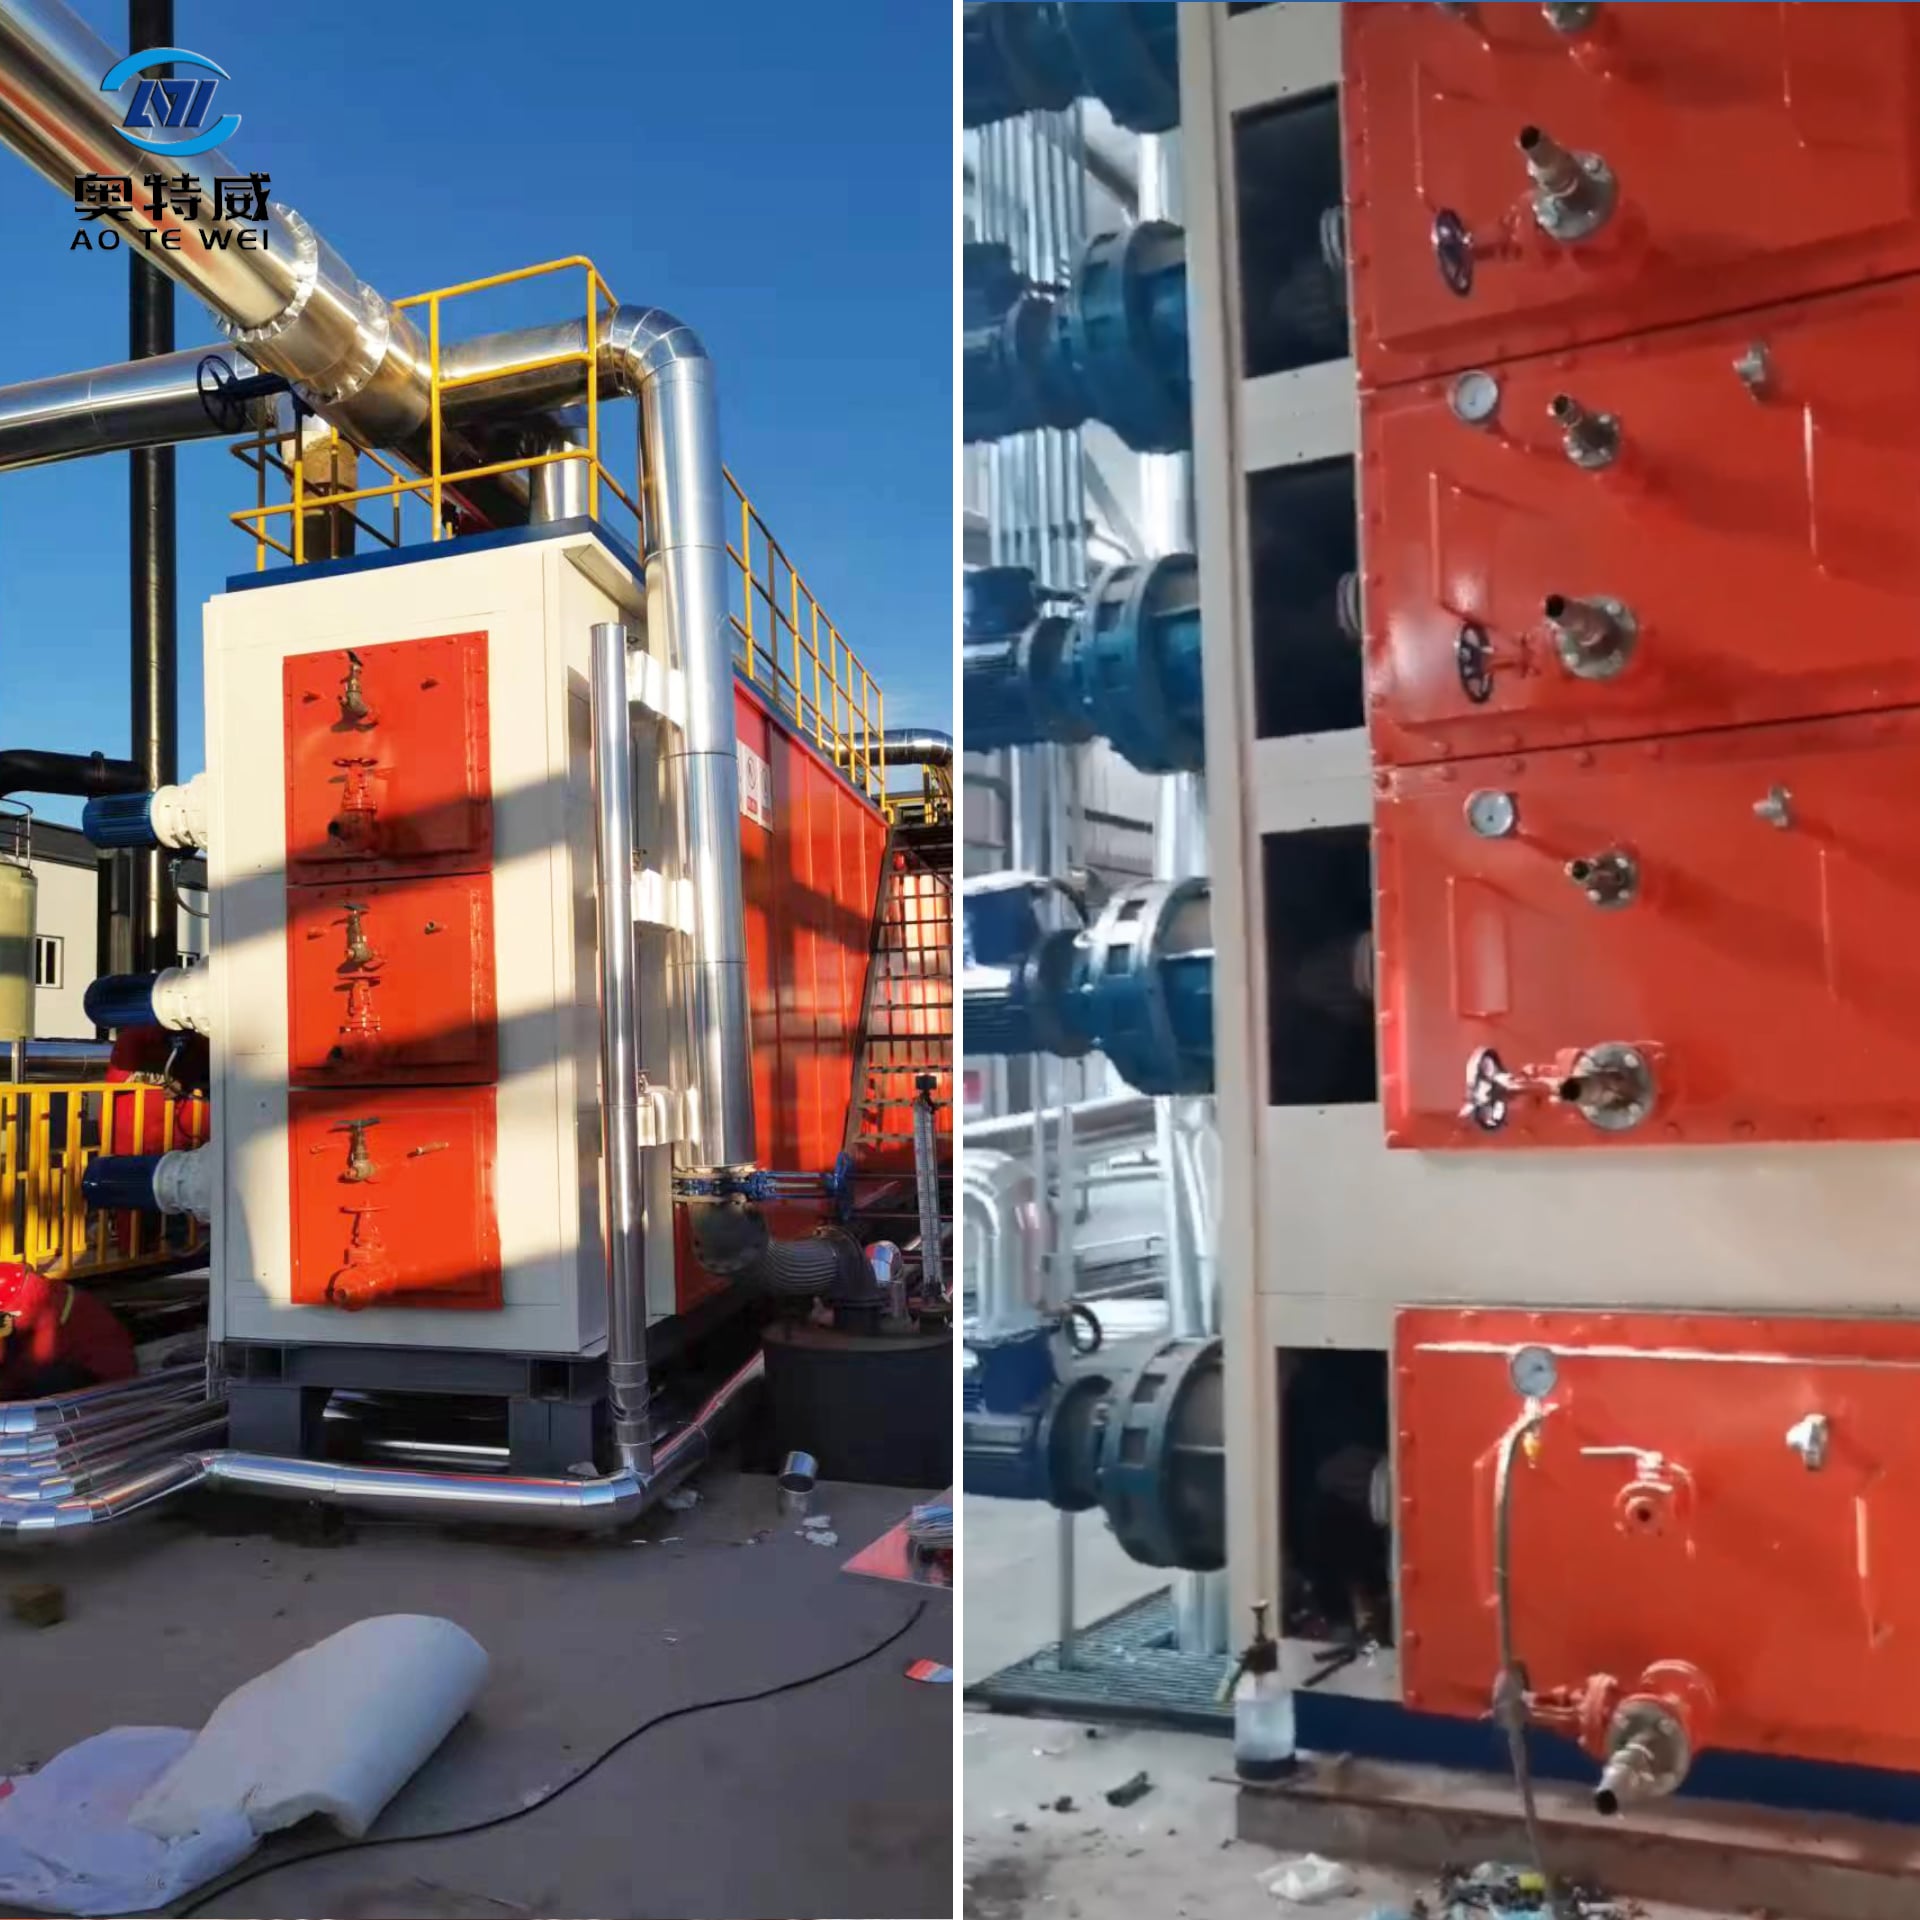
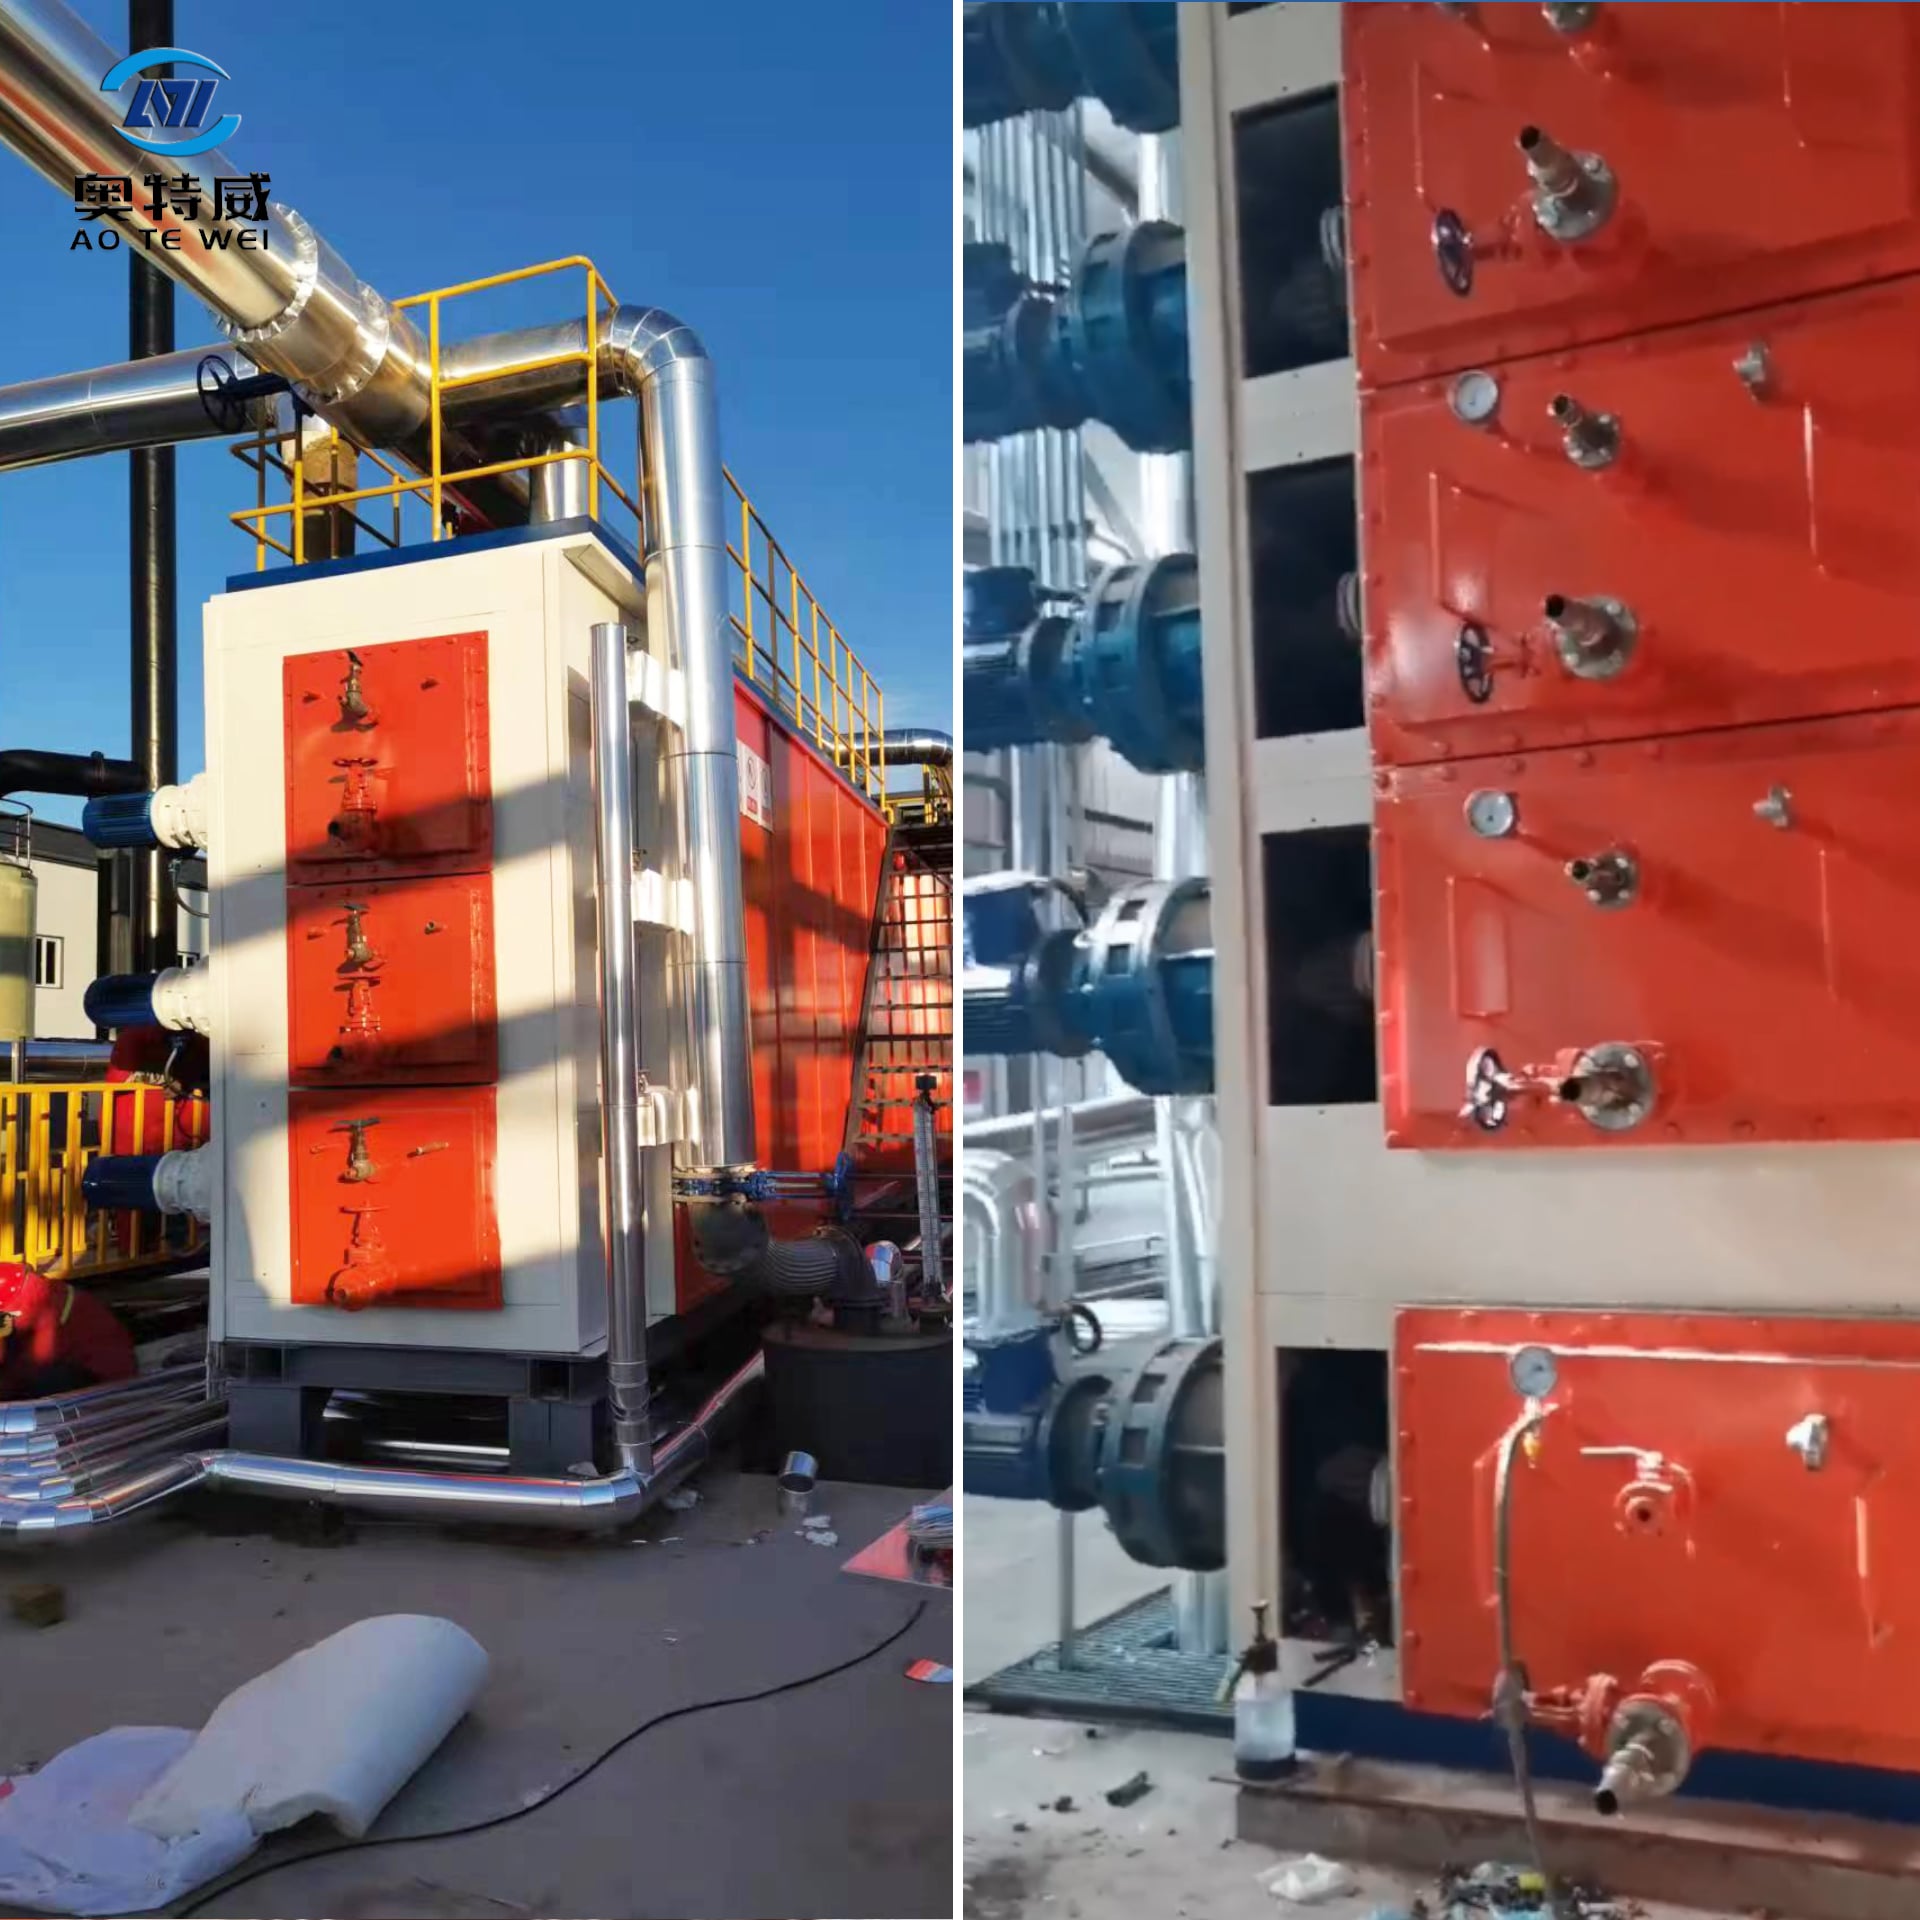
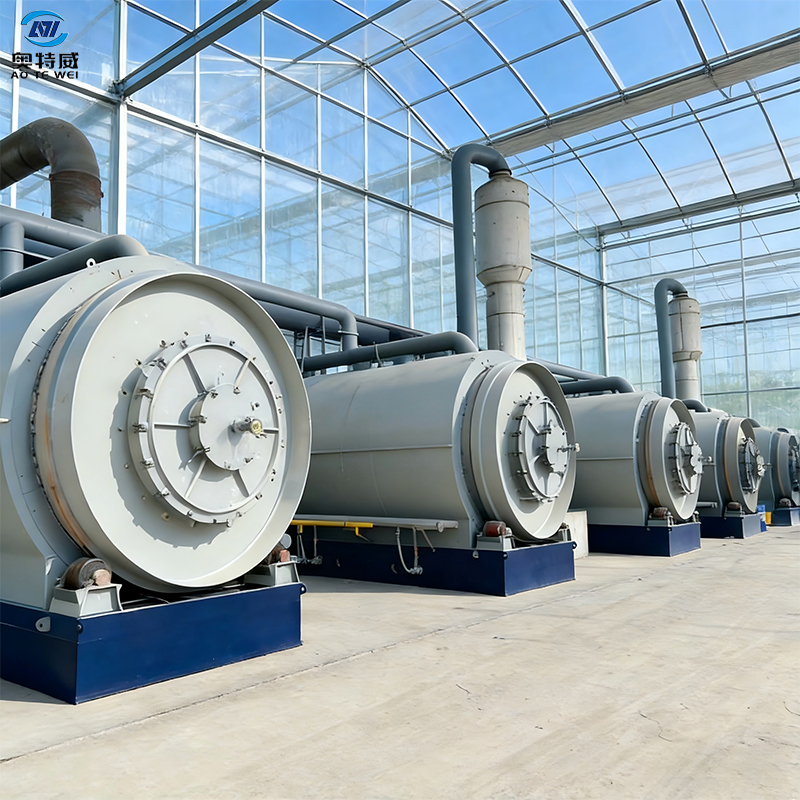
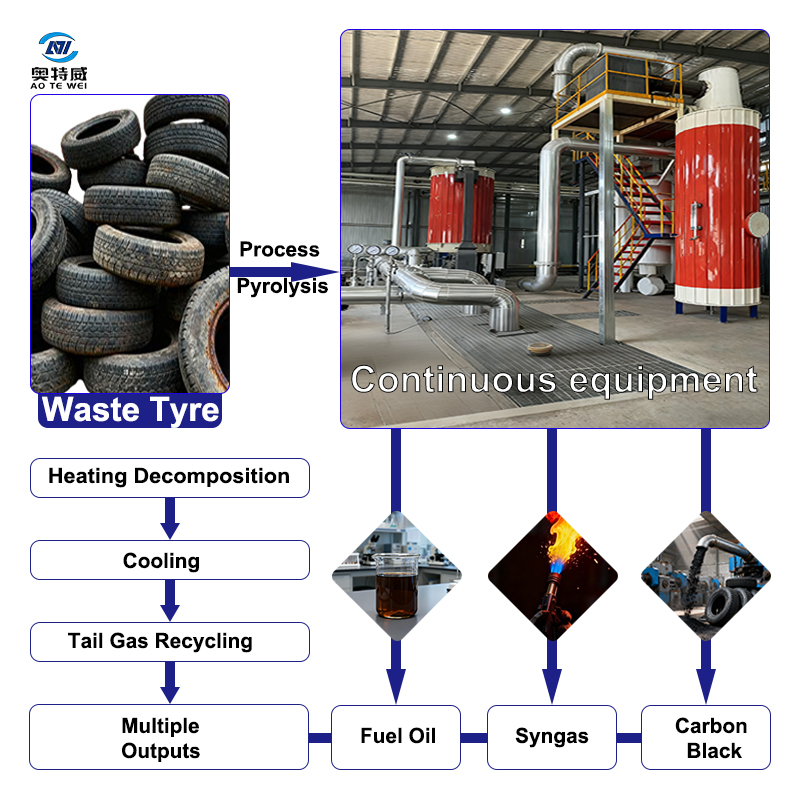
Indirect Heating Pyrolysis Reactor

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

indirect heating pyrolysis reactor

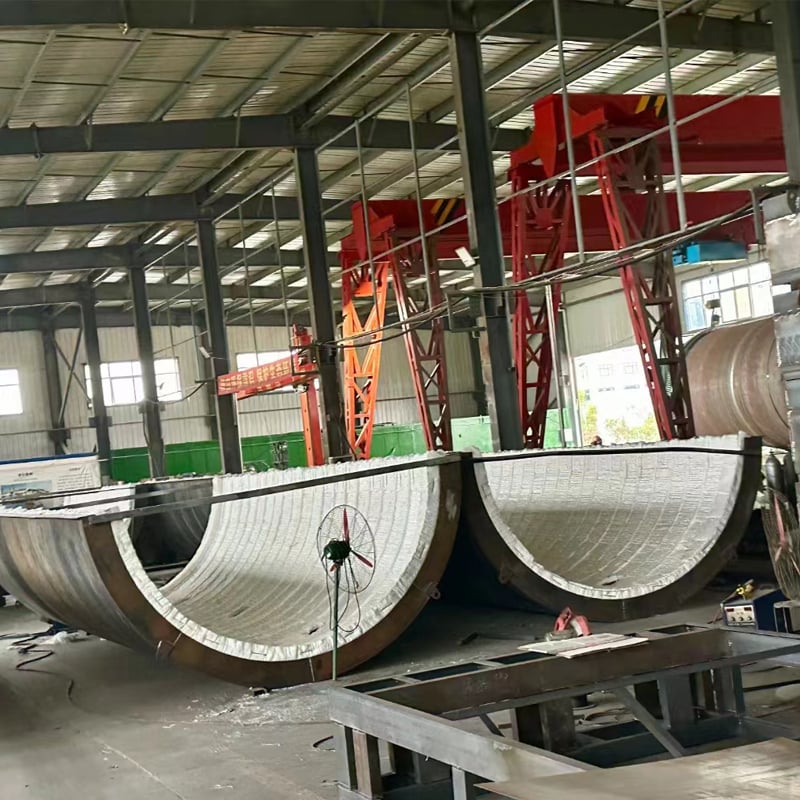
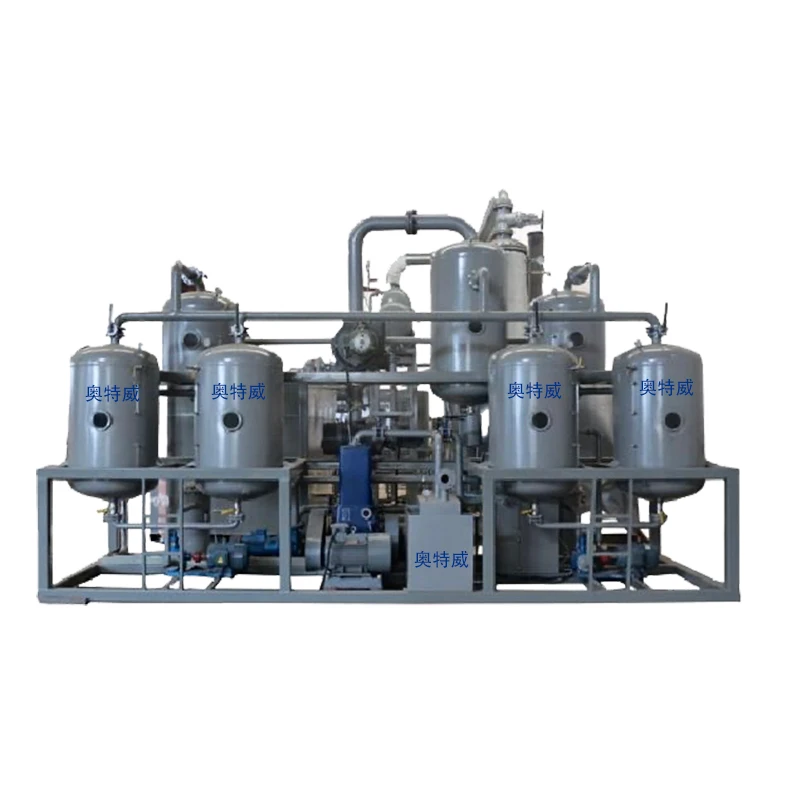
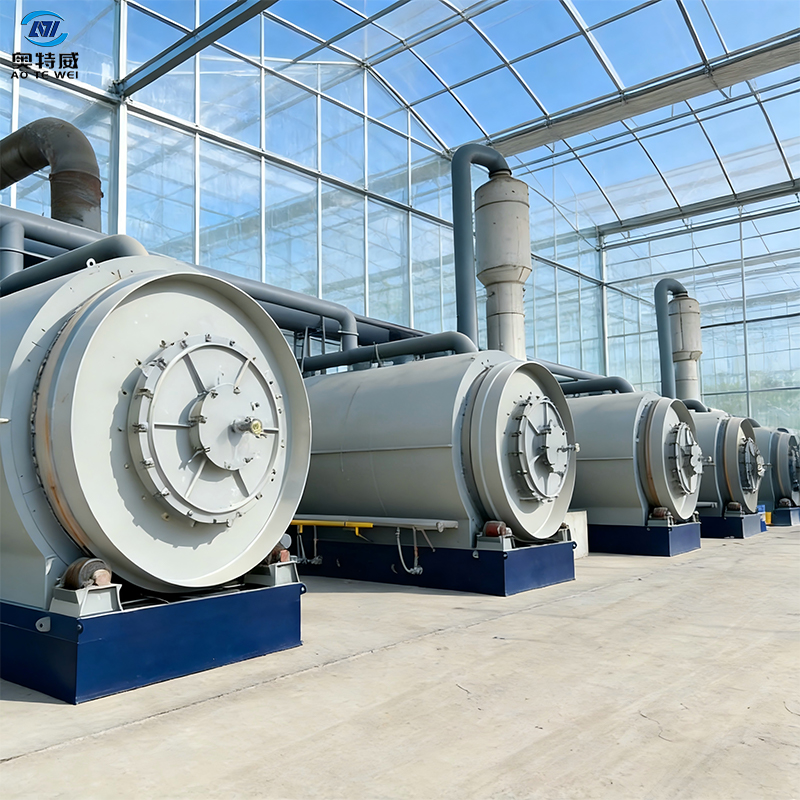
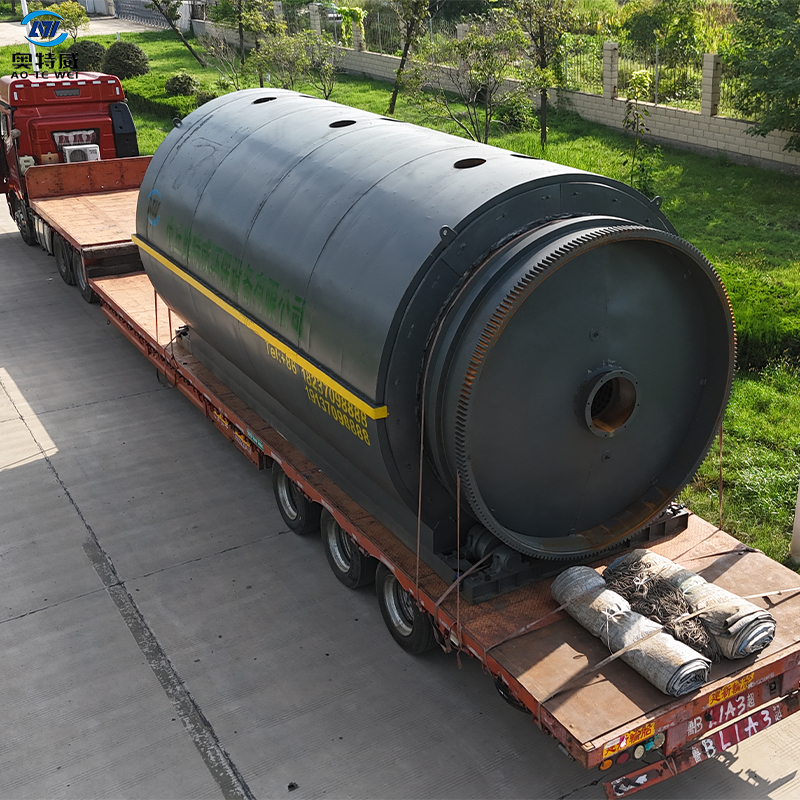
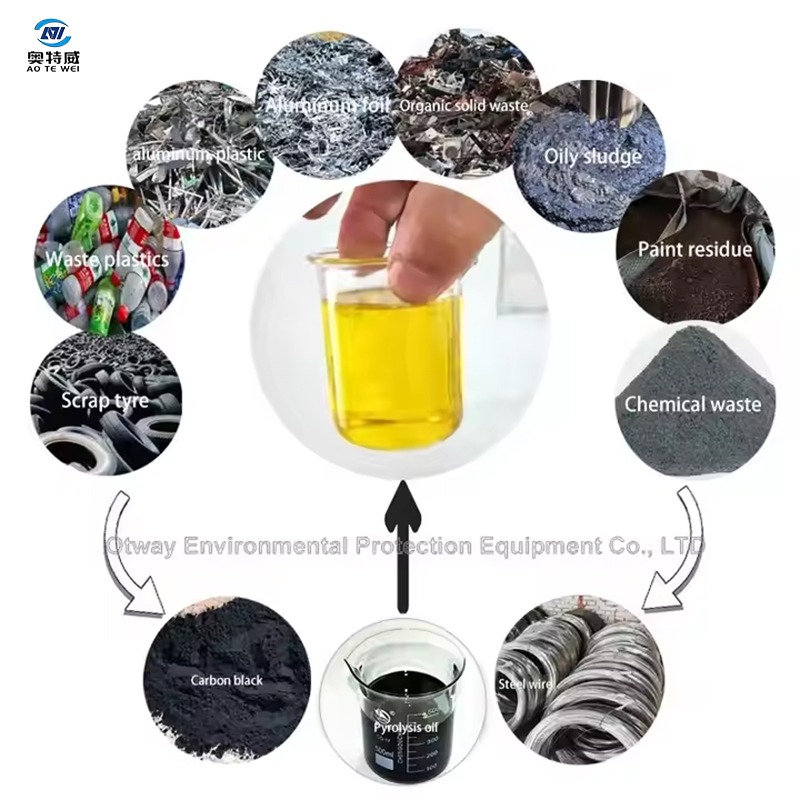
An indirect heating pyrolysis reactor represents an advanced thermal processing system designed to decompose organic materials at high temperatures without direct flame contact. This specialized equipment utilizes indirect heating mechanisms to ensure uniform temperature distribution and precise control throughout the pyrolysis process. The indirect heating pyrolysis reactor operates by transferring heat through chamber walls rather than exposing materials directly to heat sources, creating a safer and more controlled environment for material transformation. The indirect heating pyrolysis reactor serves multiple critical functions across various industries. It thermally breaks down feedstock materials into valuable products including biochar, oils, and gases through a process called pyrolysis. The technology features sophisticated temperature regulation systems, insulated vessels, and automated monitoring capabilities that ensure consistent output quality. The indirect heating pyrolysis reactor employs sealed combustion chambers that prevent oxidation while maintaining optimal thermal conditions. Key technological features include advanced heat exchangers, temperature sensors, and exhaust gas management systems. These components work together to maximize energy efficiency while minimizing environmental impact. The indirect heating pyrolysis reactor applications span waste management, biomass conversion, plastic recycling, and chemical production. Industrial facilities utilize this equipment to convert waste materials into commercially valuable products. The indirect heating pyrolysis reactor technology enables sustainable resource recovery and reduces landfill dependency across multiple sectors.
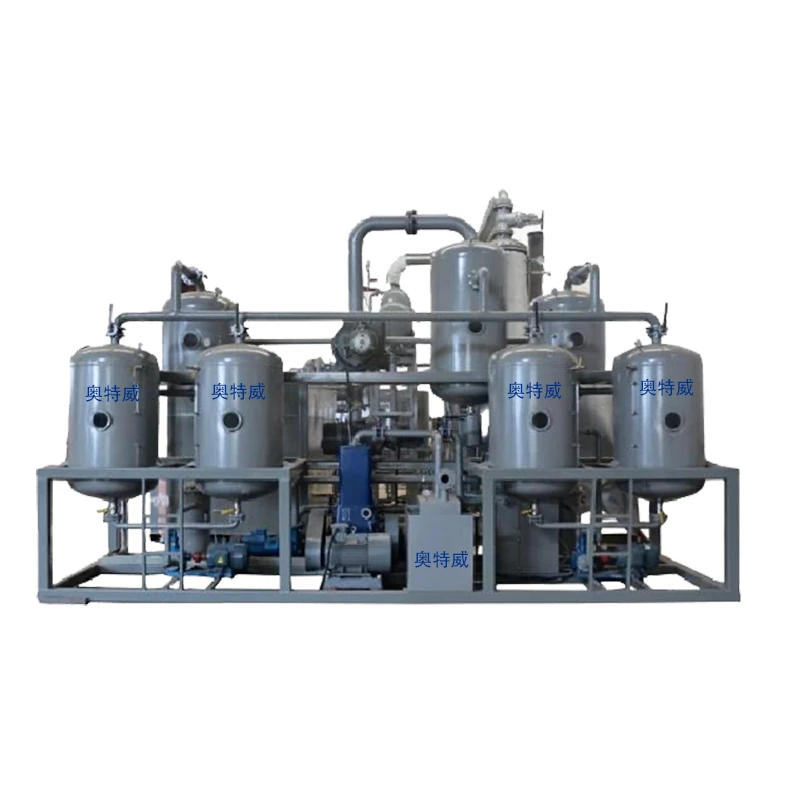
New Product Recommendations

The indirect heating pyrolysis reactor delivers substantial operational and economic advantages that make it an excellent choice for material processing businesses. This equipment eliminates direct flame exposure, creating a significantly safer working environment for operators and reducing fire-related risks considerably. The indirect heating pyrolysis reactor protects your investment by maintaining consistent operational conditions that extend equipment lifespan and reduce maintenance requirements. Operational benefits include precise temperature control that ensures uniform material processing and superior product quality throughout production cycles. The indirect heating pyrolysis reactor enables efficient feedstock conversion with minimal heat loss, reducing energy consumption and lowering operational costs substantially. Automated monitoring systems provide real-time performance data, allowing operators to optimize processes and identify potential issues before they become expensive problems. The indirect heating pyrolysis reactor excels in handling diverse material types, from biomass waste to plastic refuse, making it incredibly versatile for different industrial applications. This flexibility allows businesses to process multiple feedstock sources without equipment modifications. The sealed system design prevents air infiltration, enabling anaerobic conditions that improve product yields and quality outcomes. Environmental advantages include reduced air pollution, minimal emissions, and compliance with stringent regulatory standards. Potential customers benefit from significantly higher profitability through efficient waste-to-resource conversion. The indirect heating pyrolysis reactor generates valuable end products that offset operational expenses and create revenue streams. Businesses achieve faster payback periods on capital investments while contributing to circular economy initiatives. Advanced safety features reduce insurance costs and worker compensation claims, further improving your bottom line and operational sustainability for long-term business success.

Tips And Tricks

How does rubber recycling contribute to eco-friendly industrial development goals?

01

Sep

How does rubber recycling contribute to eco-friendly industrial development goals?

Rubber recycling has emerged as a critical pillar in achieving eco-friendly industrial development goals across manufacturing, construction, and transportation sectors. As global industries face mounting pressure to reduce environmental impact and ad...
View More
How does rubber recycling improve material reuse in manufacturing industries?

01

Sep

How does rubber recycling improve material reuse in manufacturing industries?

Rubber recycling represents one of the most effective strategies for transforming industrial waste into valuable manufacturing resources. As manufacturing industries face increasing pressure to reduce environmental footprints and optimize material co...
View More
Why do recycling plants rely on pyrolysis reactor technology for energy recovery?

01

Sep

Why do recycling plants rely on pyrolysis reactor technology for energy recovery?

Modern recycling plants face mounting pressure to recover maximum value from waste streams while maintaining environmental compliance. The pyrolysis reactor has emerged as a critical technology for achieving this balance, transforming discarded mater...
View More
How does oil distillation improve purity and usability of recycled oil products?

01

Sep

How does oil distillation improve purity and usability of recycled oil products?

Oil distillation represents one of the most effective methods for restoring the quality and usability of recycled oil products in modern industrial operations. As environmental regulations tighten and resource costs rise, the ability to recycle used ...
View More

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

indirect heating pyrolysis reactor

Precise Temperature Management and Uniform Heating Distribution

Precise Temperature Management and Uniform Heating Distribution

The indirect heating pyrolysis reactor incorporates sophisticated temperature control mechanisms that maintain exact thermal conditions throughout the pyrolysis process. Advanced heating systems distribute heat evenly across the reaction chamber, ensuring consistent material processing regardless of feedstock composition or particle size variations. This precision eliminates hot spots and temperature gradients that typically cause uneven decomposition and product quality inconsistencies. The indirect heating pyrolysis reactor's thermal management capabilities allow operators to optimize processing parameters for specific material types and desired end products. Automated sensors continuously monitor internal temperatures and automatically adjust heating intensity to maintain predetermined conditions. This level of control significantly improves product homogeneity, increases yield rates, and reduces waste generation during processing cycles. Businesses achieve superior product quality that commands premium market prices.
Enhanced Safety Features and Environmental Compliance

Enhanced Safety Features and Environmental Compliance

The indirect heating pyrolysis reactor prioritizes operator safety through sealed combustion chamber design that eliminates direct flame contact and fire hazards. The equipment operates in controlled, anaerobic conditions that prevent unexpected reactions and dangerous gas accumulation. Advanced ventilation systems capture and treat exhaust gases before atmospheric release, ensuring compliance with environmental regulations and air quality standards. The indirect heating pyrolysis reactor minimizes harmful emissions including particulates, volatile organic compounds, and greenhouse gases that regulatory agencies strictly monitor. Companies utilizing this technology demonstrate environmental responsibility while avoiding costly penalties and operational shutdowns. The sealed system design prevents fugitive emissions that damage air quality in surrounding communities. Workers operate in safer environments with reduced exposure to toxic substances and thermal hazards.
Versatile Feedstock Processing and Exceptional Product Recovery

Versatile Feedstock Processing and Exceptional Product Recovery

The indirect heating pyrolysis reactor handles an impressive range of material inputs including agricultural waste, plastic refuse, tire chips, wood residue, and mixed organic matter. This versatility allows businesses to process diverse waste streams without equipment modifications or complex operational adjustments. The indirect heating pyrolysis reactor converts waste materials into valuable products including biochar, pyrolysis oils, and syngas that generate substantial revenue. Different feedstock types produce marketable end products suitable for energy generation, soil amendments, or chemical manufacturing applications. The sealed anaerobic environment maximizes conversion efficiency and improves product yields compared to conventional thermal processing methods. Businesses unlock additional income streams by processing multiple material sources simultaneously or sequentially throughout operational periods.

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000
Newsletter
Please Leave A Message With Us