Distillation of Kerosene: Quality Fuel Production

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

distillation of kerosene

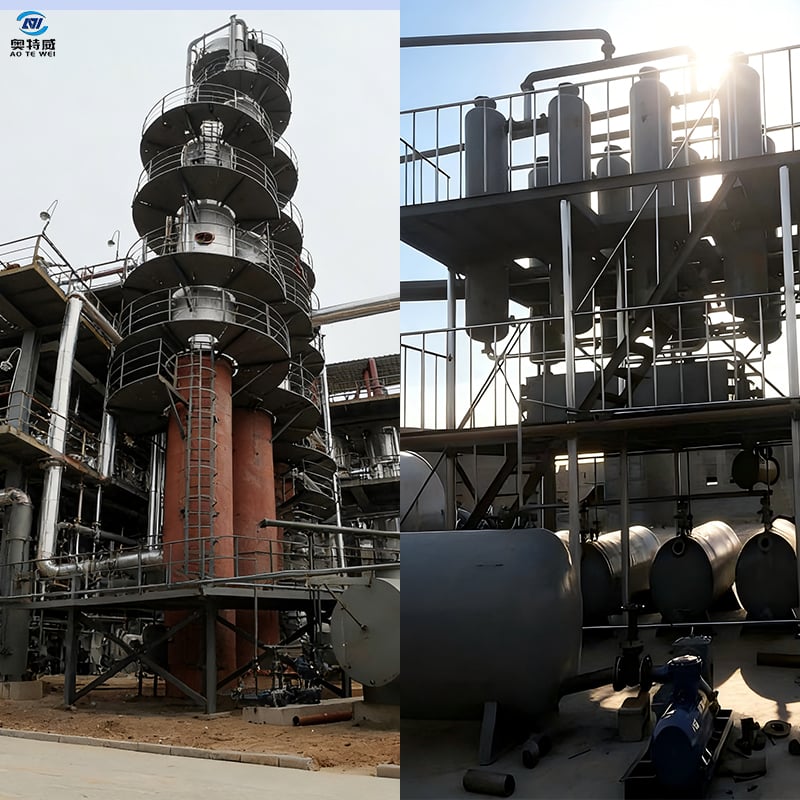
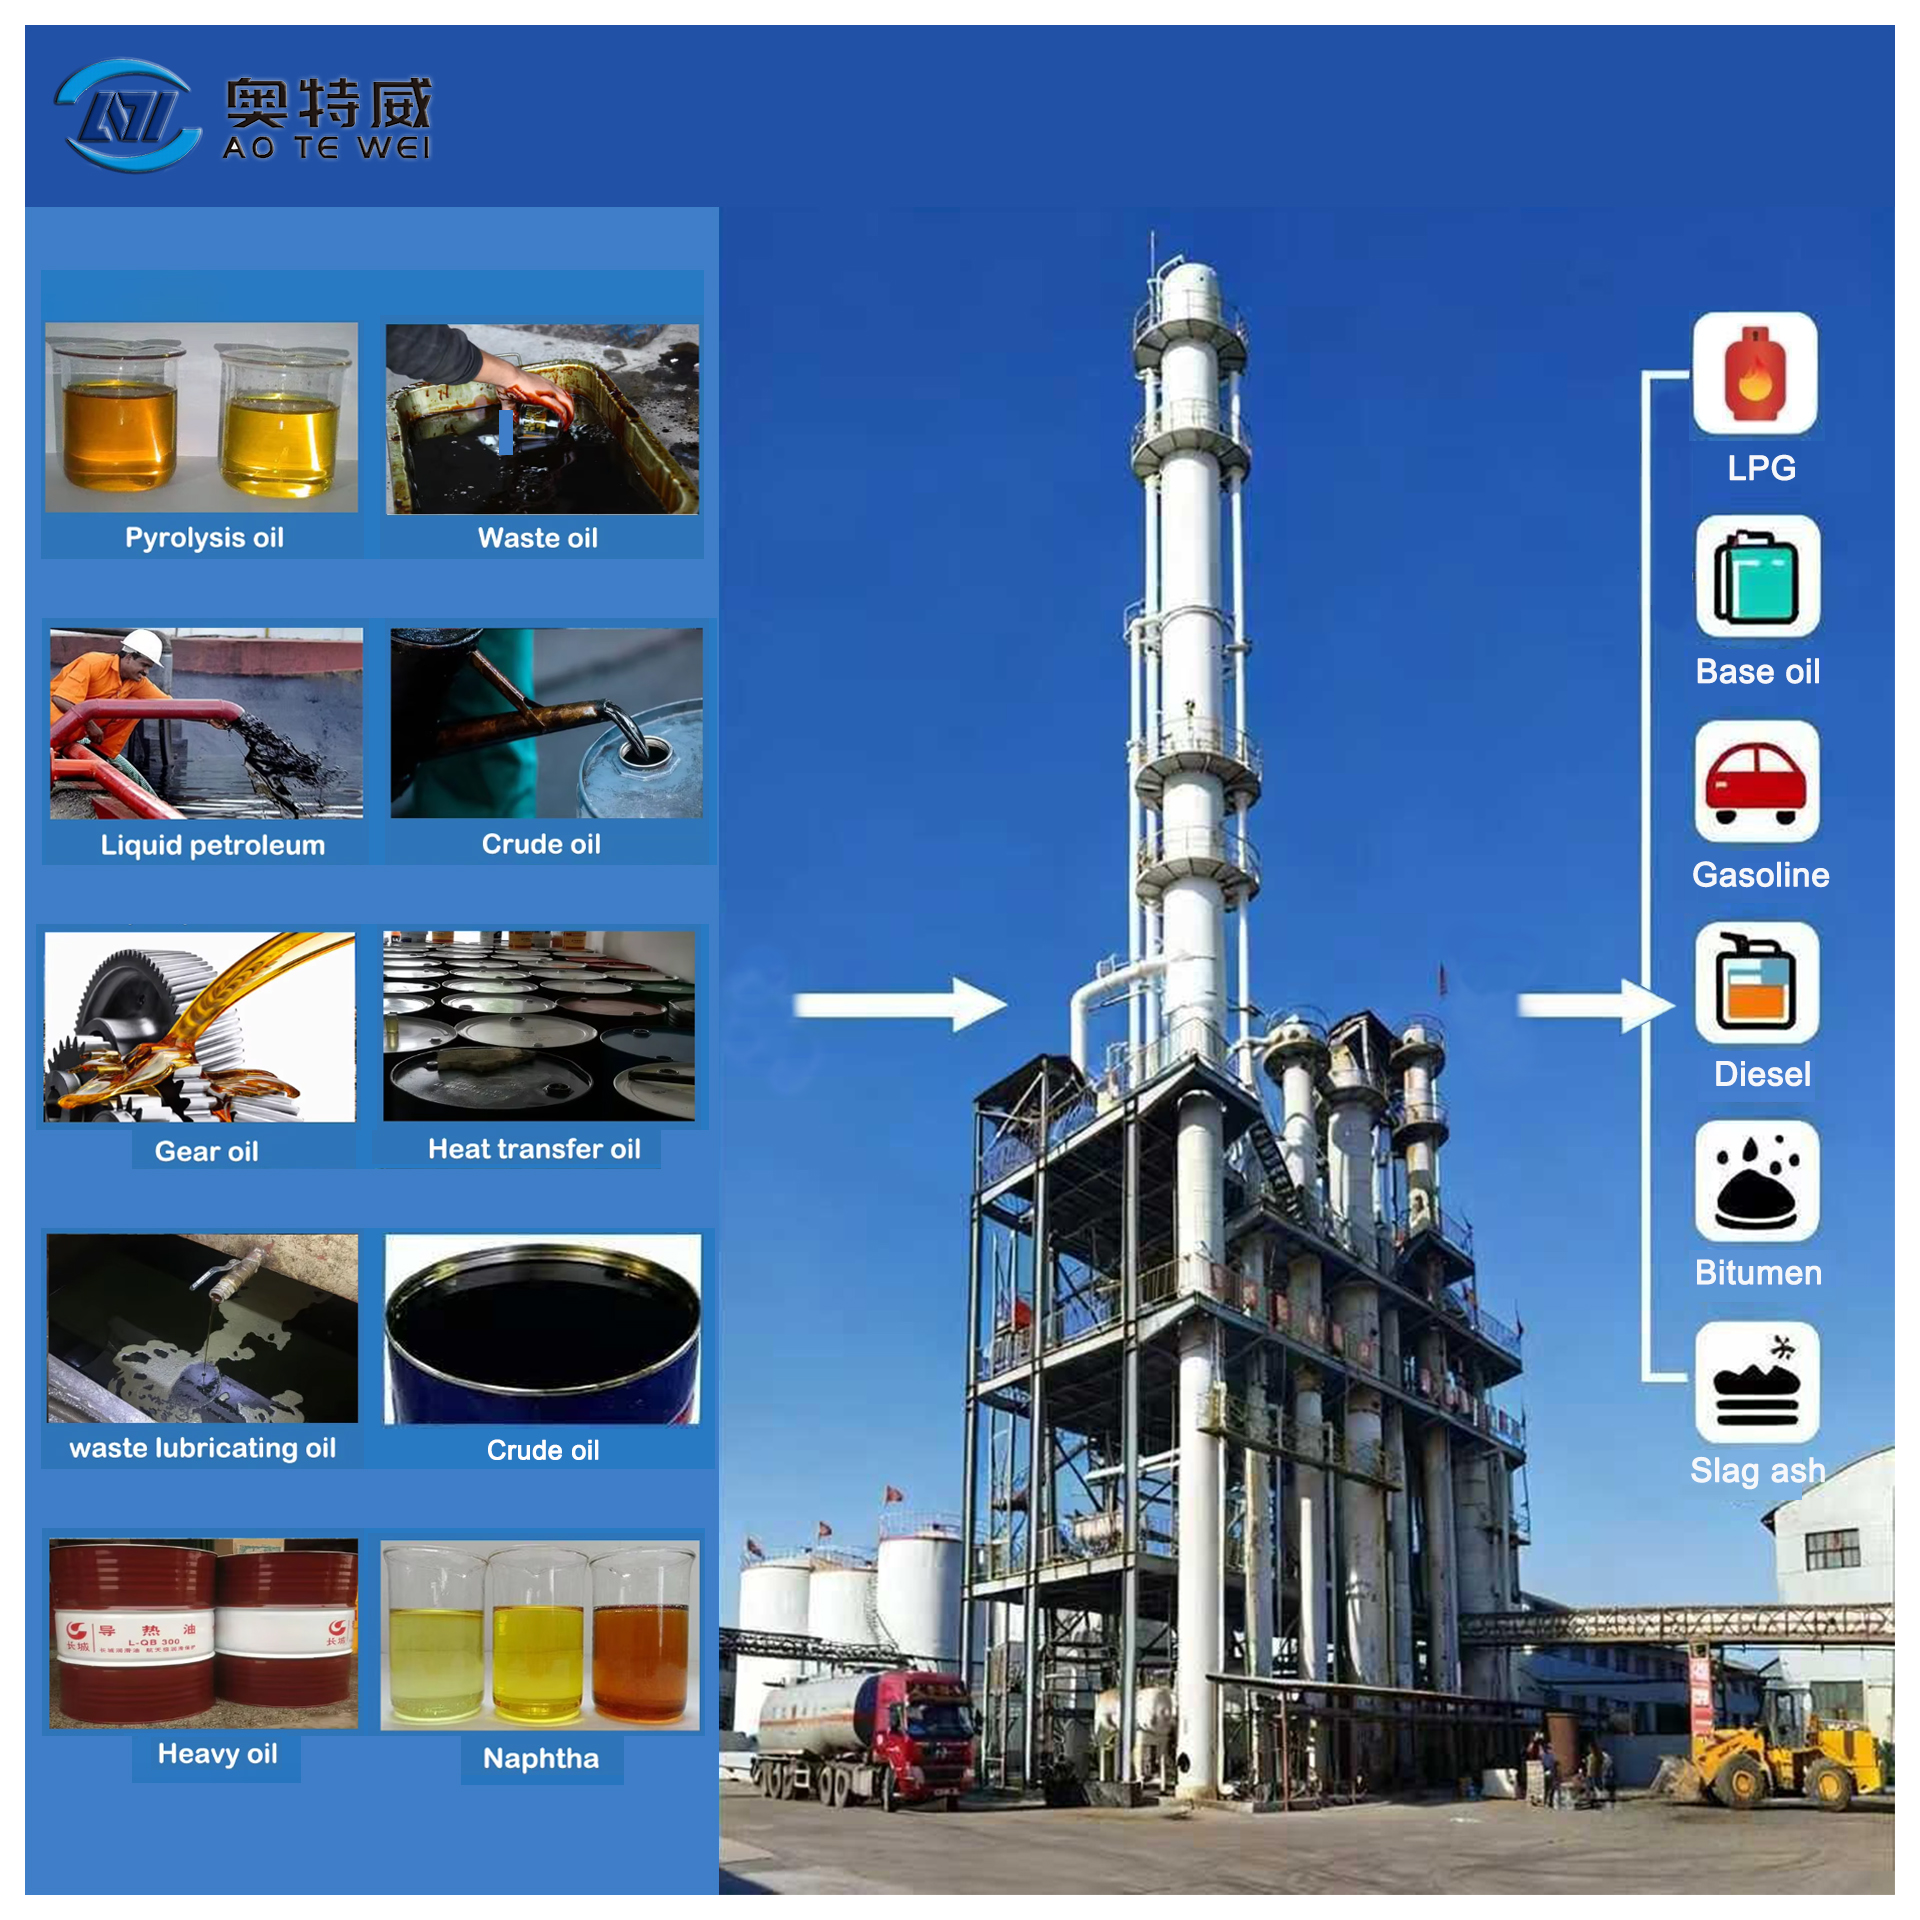
The distillation of kerosene represents a critical refining process that separates kerosene from crude oil through heat and fractional distillation techniques. This petroleum refining method utilizes the boiling point differences between various hydrocarbons to extract kerosene, a versatile fuel product with numerous applications across industries. The distillation of kerosene involves heating crude oil to approximately 350-400 degrees Celsius, forcing heavier and lighter components to vaporize selectively. These vapors then enter a fractionating column where temperature gradients guide molecules to their appropriate collection levels based on molecular weight and boiling points. The distillation of kerosene produces a refined product with consistent quality, optimal viscosity, and reliable performance characteristics. Modern distillation facilities employ advanced monitoring systems and automated controls to maintain precise temperature and pressure conditions throughout the process. The extracted kerosene typically contains hydrocarbons ranging from C10 to C14, making it ideal for specific industrial and consumer applications. The distillation of kerosene remains economically efficient, allowing refineries to maximize yield while minimizing waste. This sophisticated separation process ensures that the final product meets stringent international quality standards and regulatory requirements. Understanding the distillation of kerosene helps customers appreciate the engineering excellence behind fuel production.

New Product Recommendations

The distillation of kerosene offers substantial operational advantages that directly benefit end-users and industrial applications. First, this refining process produces kerosene with exceptional purity and consistency, ensuring reliable performance across heating systems, aviation engines, and lighting applications. The distillation of kerosene maintains precise quality control through continuous monitoring, eliminating batch variations that compromise equipment efficiency. Users experience superior combustion characteristics, reduced maintenance costs, and extended equipment lifespan when utilizing kerosene produced through proper distillation methods. The distillation of kerosene also delivers cost-effective fuel production by optimizing crude oil utilization and minimizing processing waste. This efficiency translates to more competitive market pricing while maintaining premium product quality. Environmental benefits emerge prominently, as the distillation of kerosene incorporates modern emission controls and waste management systems. The refined product burns cleaner, producing fewer pollutants than alternative fuels. Industrial customers gain significant advantages through reliable supply chains and standardized product specifications. The distillation of kerosene ensures compatibility with existing infrastructure, requiring no equipment modifications for most applications. Additionally, the process supports energy independence by maximizing domestic crude oil processing capabilities. Businesses and households benefit from stable pricing structures when refineries operate efficient distillation facilities. The distillation of kerosene represents a proven technology offering measurable operational improvements, environmental responsibility, and economic advantages that justify continued investment in this essential refining process.

Practical Tips

How does oil distillation improve purity and usability of recycled oil products?

01

Sep

How does oil distillation improve purity and usability of recycled oil products?

Oil distillation represents one of the most effective methods for restoring the quality and usability of recycled oil products in modern industrial operations. As environmental regulations tighten and resource costs rise, the ability to recycle used ...
View More
What factors affect productivity in a distillation plant processing system?

30

Jul

What factors affect productivity in a distillation plant processing system?

A distillation plant is at the heart of many industrial refining operations, converting used engine oil, pyrolysis oil, and other feedstocks into valuable diesel fuel. Understanding what drives productivity in a distillation plant is essential for op...
View More
How does rubber recycling contribute to eco-friendly industrial development goals?

01

Sep

How does rubber recycling contribute to eco-friendly industrial development goals?

Rubber recycling has emerged as a critical pillar in achieving eco-friendly industrial development goals across manufacturing, construction, and transportation sectors. As global industries face mounting pressure to reduce environmental impact and ad...
View More
How does a continuous pyrolysis plant support uninterrupted industrial production?

03

Sep

How does a continuous pyrolysis plant support uninterrupted industrial production?

Industrial manufacturers face significant operational challenges when production must halt for maintenance or equipment downtime. A continuous pyrolysis plant eliminates these disruptions by maintaining consistent, uninterrupted output throughout the...
View More

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000

distillation of kerosene

Superior Fuel Quality and Consistency

Superior Fuel Quality and Consistency

The distillation of kerosene produces exceptionally pure fuel with outstanding consistency that exceeds industry standards. Modern distillation equipment separates hydrocarbons with remarkable precision, ensuring that every batch of kerosene maintains identical chemical composition and performance characteristics. This consistency eliminates the variability problems associated with lower-grade fuels, guaranteeing reliable combustion properties regardless of seasonal temperature changes or storage duration. Users experience predictable energy output, improved flame quality, and reduced equipment wear when relying on kerosene produced through advanced distillation processes. The distillation of kerosene incorporates real-time quality monitoring systems that test viscosity, sulfur content, and thermal stability throughout production cycles. These rigorous quality assurance protocols ensure that finished kerosene consistently meets stringent specifications set by international petroleum organizations. Customers purchasing distillation of kerosene benefit from reduced operational downtime, fewer maintenance issues, and extended equipment longevity. This superior quality translates directly into cost savings over time, making premium-quality kerosene a financially prudent choice for heating systems, generators, and industrial applications.
Enhanced Environmental Performance and Emissions Reduction

Enhanced Environmental Performance and Emissions Reduction

The distillation of kerosene incorporating modern environmental technologies delivers cleaner fuel with significantly lower emission profiles. Advanced refining processes remove harmful sulfur compounds, aromatic hydrocarbons, and other pollutants that contribute to air quality degradation. When the distillation of kerosene emphasizes environmental standards, the resulting product burns more completely, generating fewer particulate emissions and reduced carbon footprints. This environmental advantage proves particularly important for industrial facilities operating under strict emission regulations and sustainability mandates. The distillation of kerosene through state-of-the-art methods supports corporate environmental initiatives and helps organizations meet their carbon reduction targets. Users switching to environmentally optimized kerosene contribute positively to community air quality while demonstrating corporate environmental responsibility. Modern distillation facilities employ waste minimization strategies, closed-loop water systems, and advanced emission controls. These comprehensive environmental measures ensure that kerosene production aligns with global sustainability objectives. The distillation of kerosene represents a commitment to protecting planetary health while delivering reliable fuel performance, satisfying both operational requirements and environmental consciousness.
Reliable Performance Across Diverse Industrial Applications

Reliable Performance Across Diverse Industrial Applications

The distillation of kerosene produces versatile fuel suitable for aviation, heating, industrial processing, and emergency backup power applications. Each industry vertical benefits from kerosene's stable combustion characteristics, predictable energy content, and compatibility with existing equipment infrastructure. The distillation of kerosene maintains flame brightness and heat output consistency, making it ideal for precision heating applications and specialized industrial processes requiring stable thermal conditions. Aviation industries depend critically on kerosene distillation quality, as jet fuel specifications demand extraordinary purity and performance reliability. The distillation of kerosene for aviation purposes incorporates additional purification stages and rigorous testing protocols ensuring flight safety and engine reliability. Commercial facilities utilize distillation of kerosene for emergency generators, backup heating systems, and specialized manufacturing processes requiring controlled heat application. This broad application suitability demonstrates kerosene's versatility and the essential role distillation plays in fuel preparation. Organizations across diverse sectors gain competitive advantages through access to reliable, high-performance kerosene fuel. The distillation of kerosene ensures that every application receives optimal fuel specifications, maximizing operational efficiency and equipment lifespan across industrial landscapes.

Get a Free Quote

Our representative will contact you soon.
Email
WhatsApp / Mobile
Name
Company Name
Message
0/1000
Newsletter
Please Leave A Message With Us